I Counted a Dozen Sensors on a Single Machine at the Laundry Exhibition
The Shanghai Laundry Expo in China Kicks Off in Grand Style, Unlocking a New Ecosystem for Industrial Laundry 01
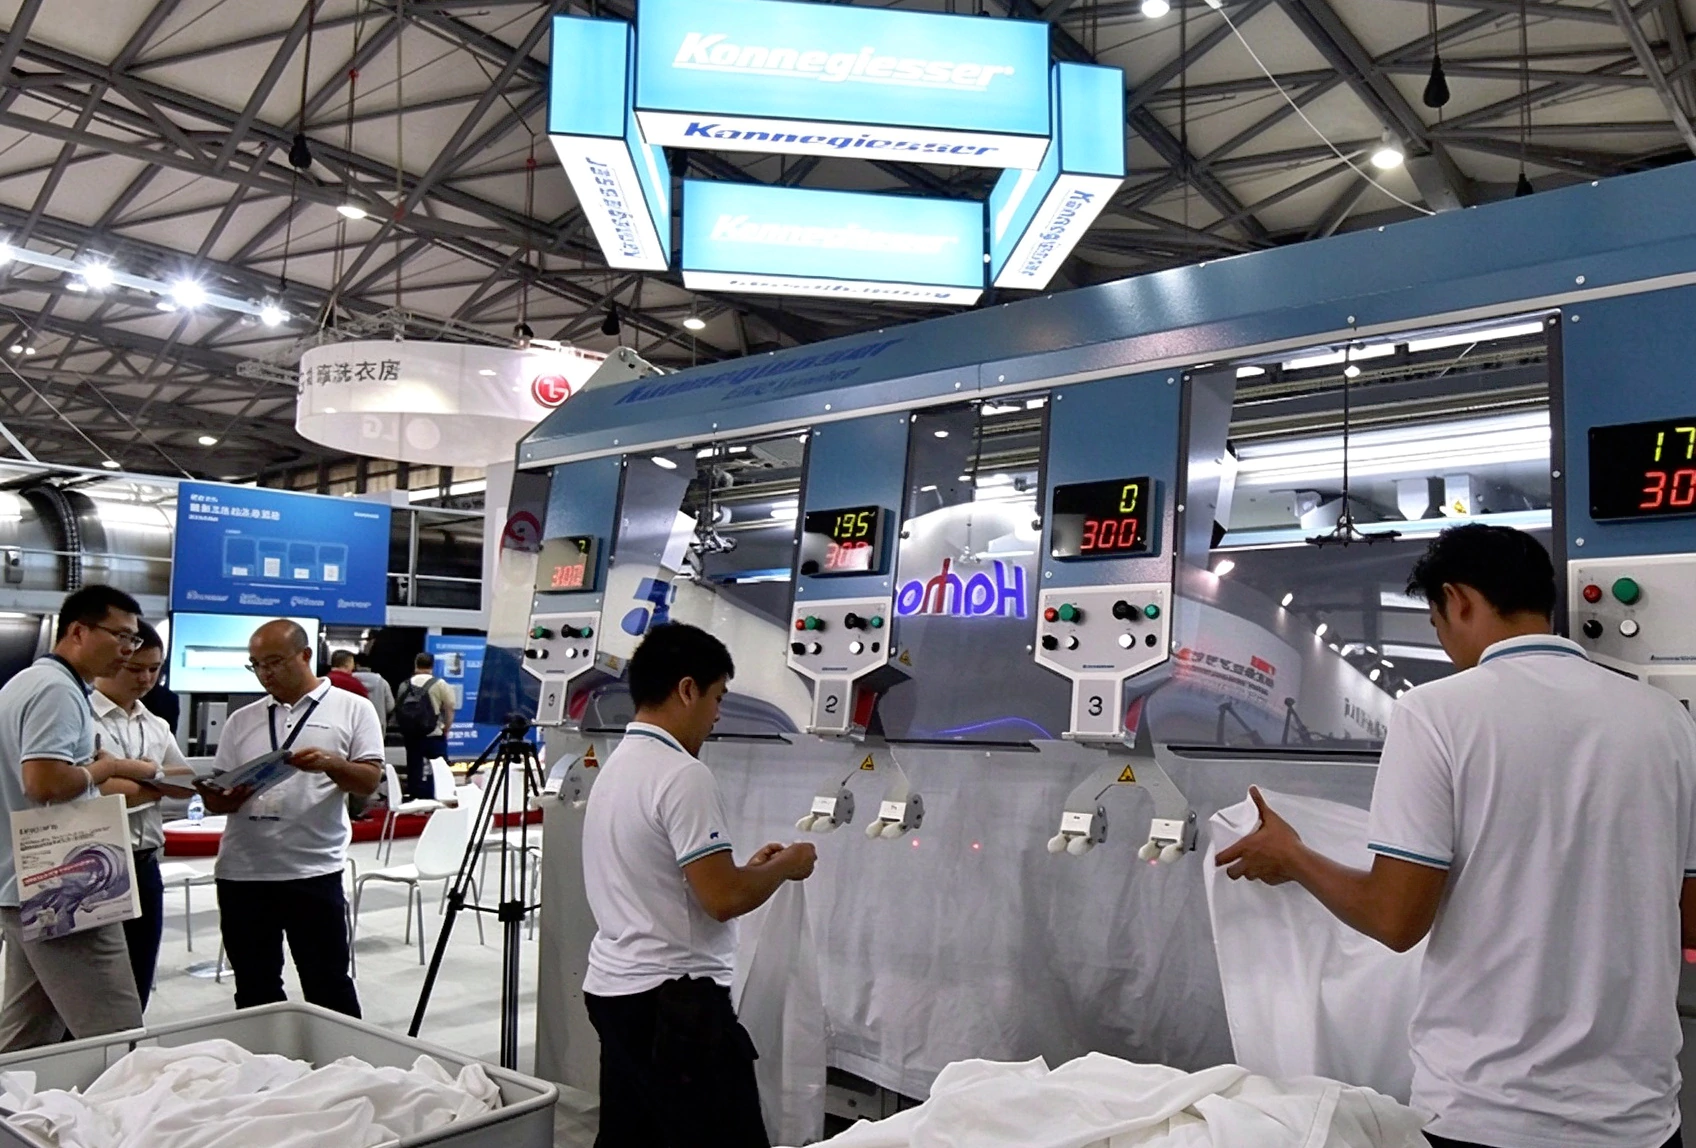
To be honest, before visiting, my understanding of a commercial laundry plant stopped at “big washing machines plus dryers.”
It wasn’t until we walked into the industrial washing exhibition in China and stood in front of ironers, folders, and feeders that it hit me.
this isn’t “washing clothes.” This is an entire, highly automated industrial production line.
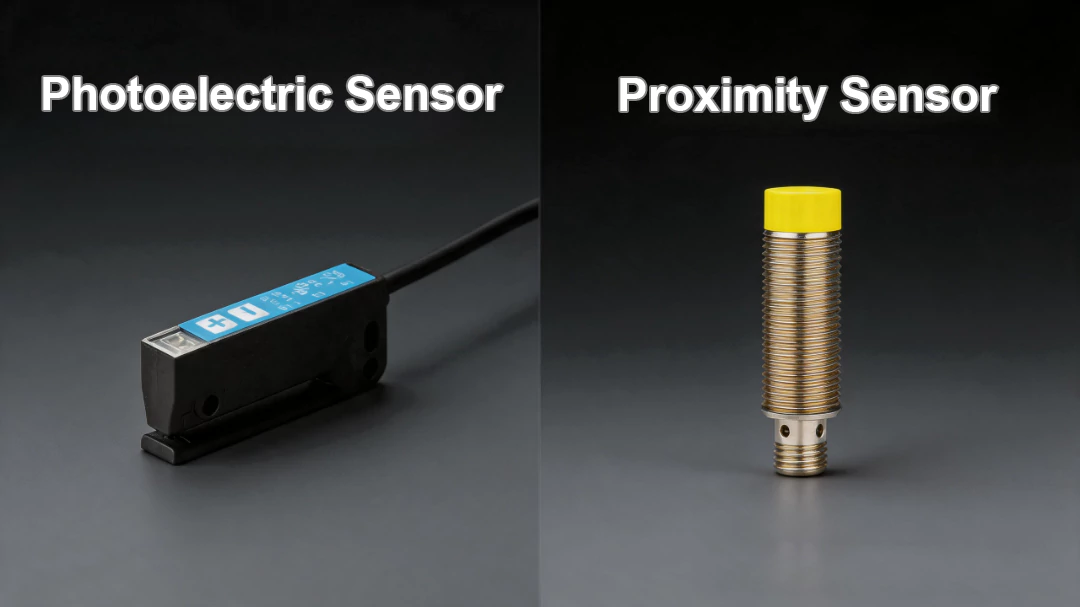
Photoelectric switches: the “eyes” on the conveyor that set the pace of the whole line 02
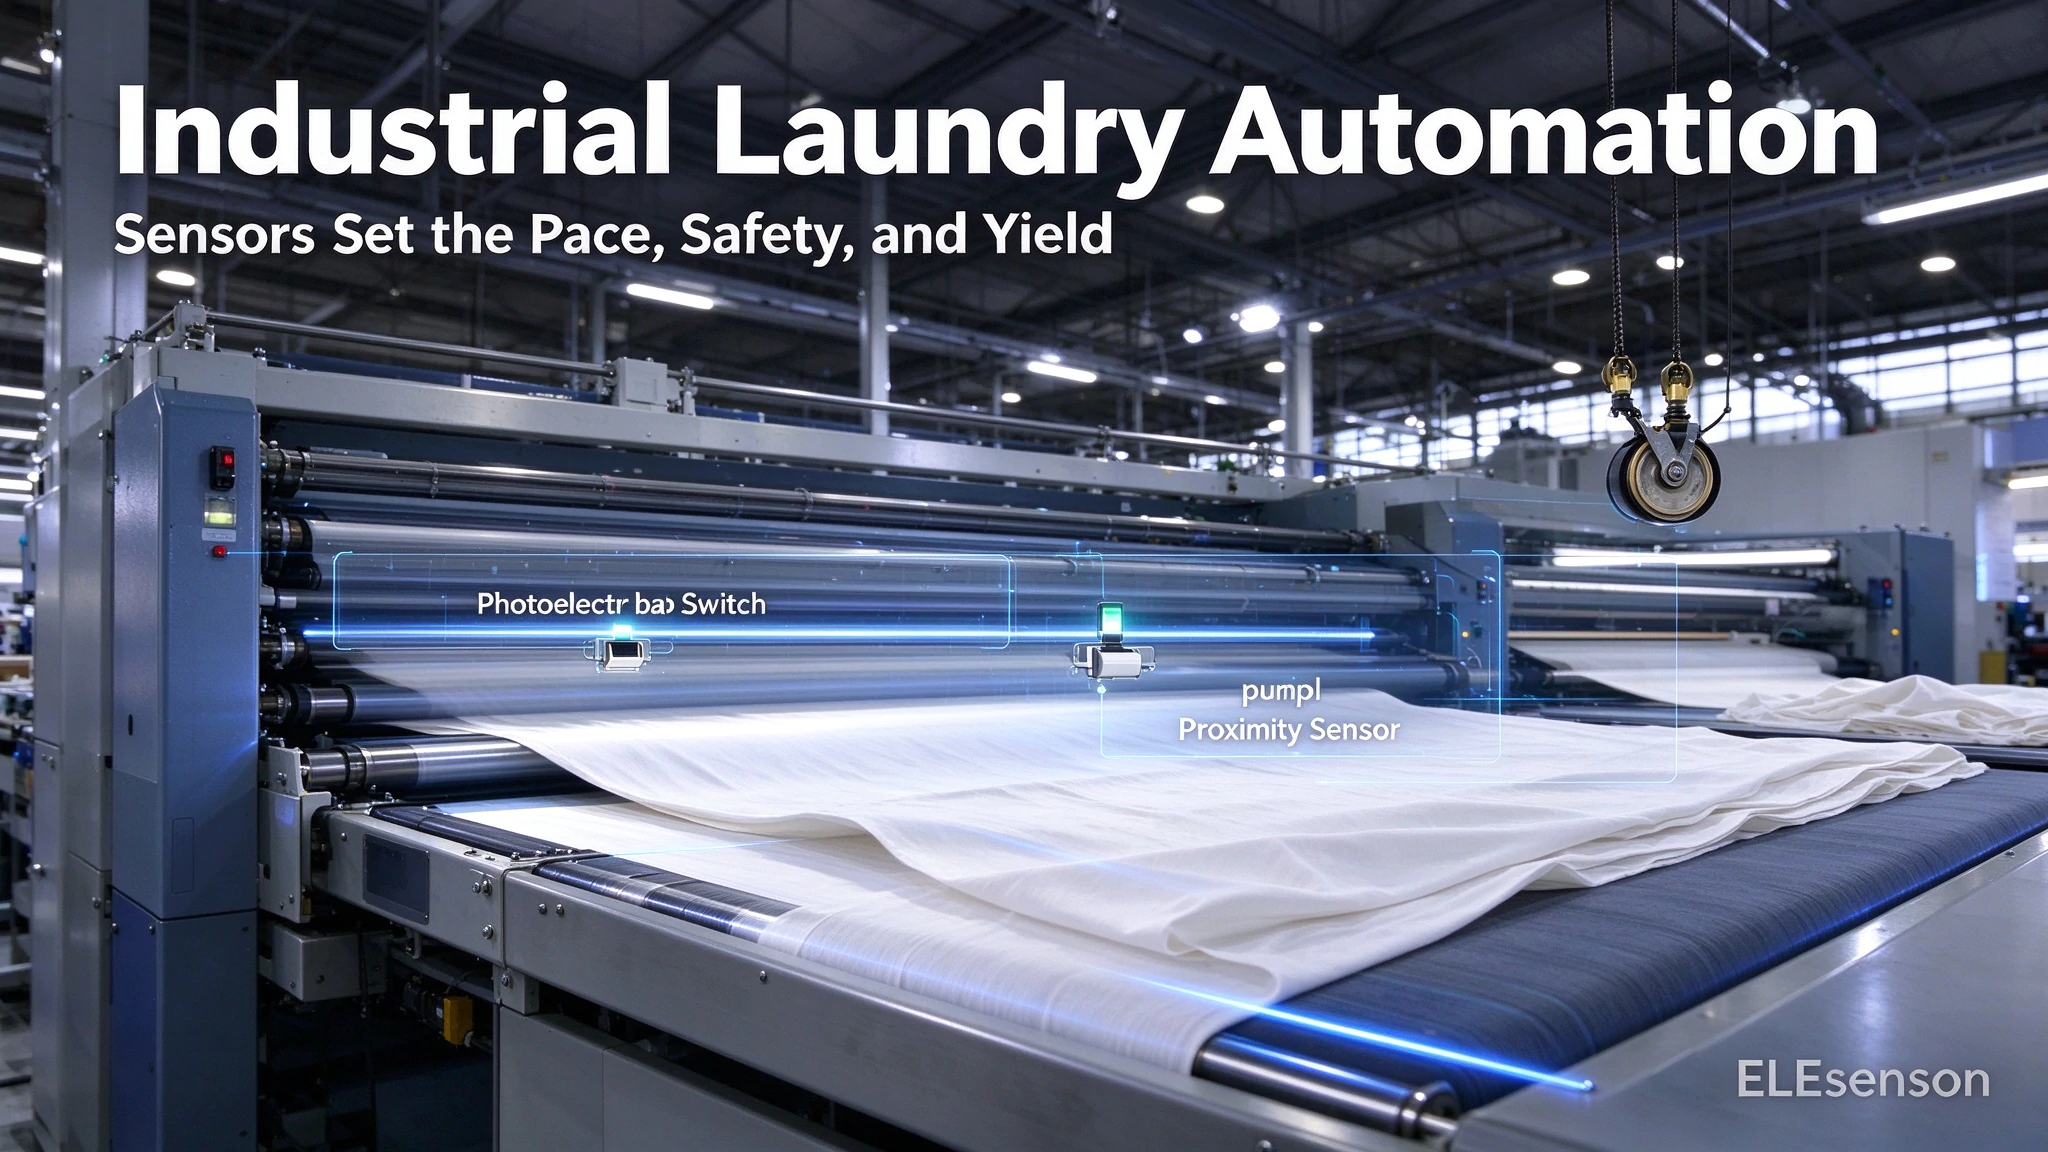
At the first machine, my eyes went straight to the conveyor. A stack of towels went in at the feed, the belt ran smoothly, and at a certain point the machine automatically started ironing and folding — with nobody pressing a button.
“Who tells the machine the linen is here?” I asked my colleague. He pointed at a fingernail-sized part on the side of the belt ——
photoelectric switch.
When the fabric arrives, the light is blocked, a signal fires, and the machine starts. When it passes, the light path recovers and the machine stands by.
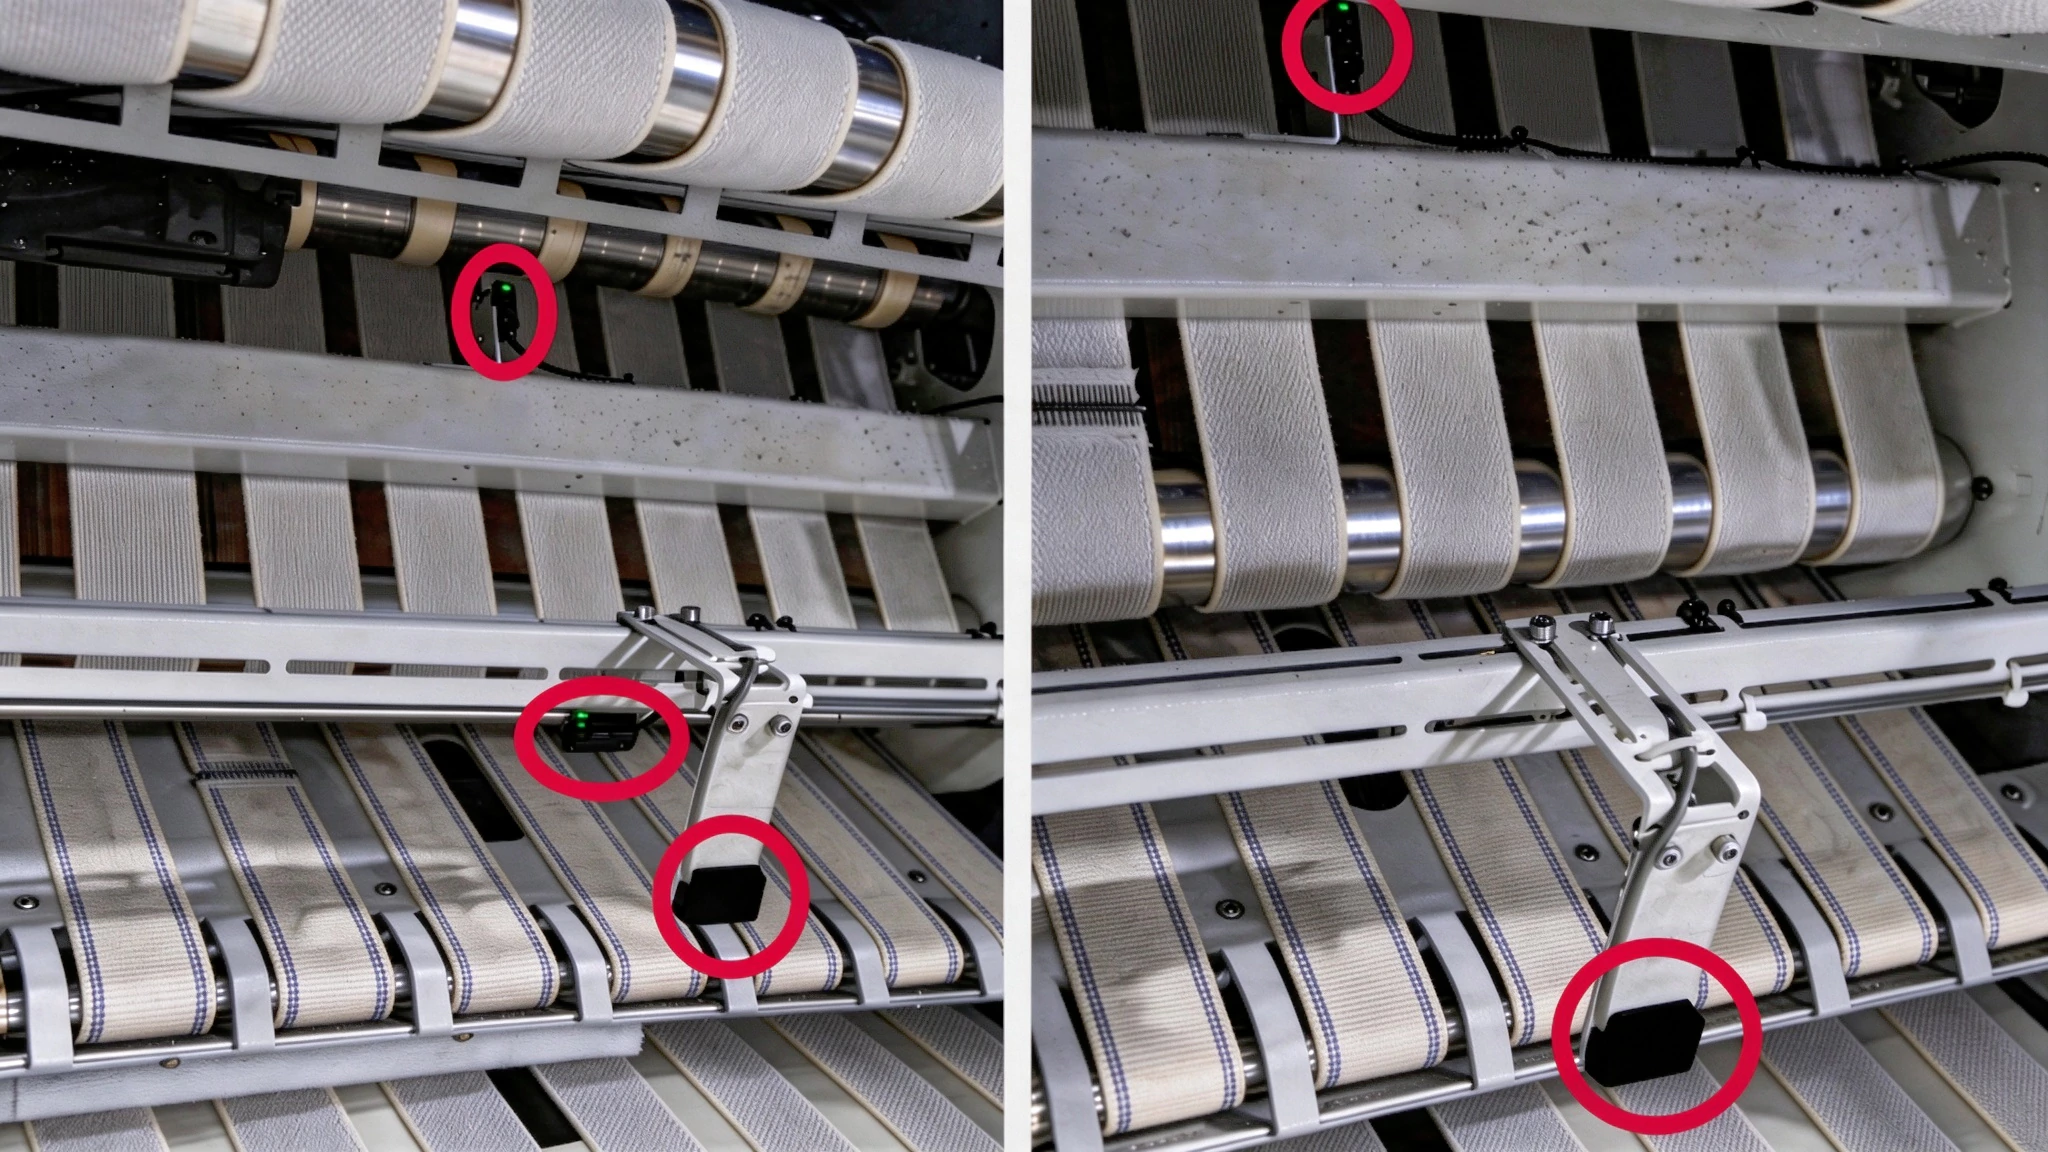
That tiny component sets the pace of the entire line. Without it, the machine either idles and wastes power, or fabric piles up and jams. A laundry plant processes thousands of pieces of linen every day, and every “yes/no” judgment has to be right — one miss, and the whole line stops.
Proximity sensors: the “gatekeepers” up top that catch a fault in the first second 03
Look up and you see a different story. The top of the machine is full of pulley banks — linen is pulled from one roller to the next, driven by these wheels. Get close and you’ll find a small device near almost every pulley: a proximity sensor.
It doesn’t touch the wheel, yet it can sense whether it is turning and turning correctly. The moment a pulley stops — a torn cloth, a jam, or a worn bearing — the proximity sensor fires a signal and the whole line emergency-stops.
Don’t underestimate that stop. A 10-second delay can mean hundreds of meters of fabric scrapped.
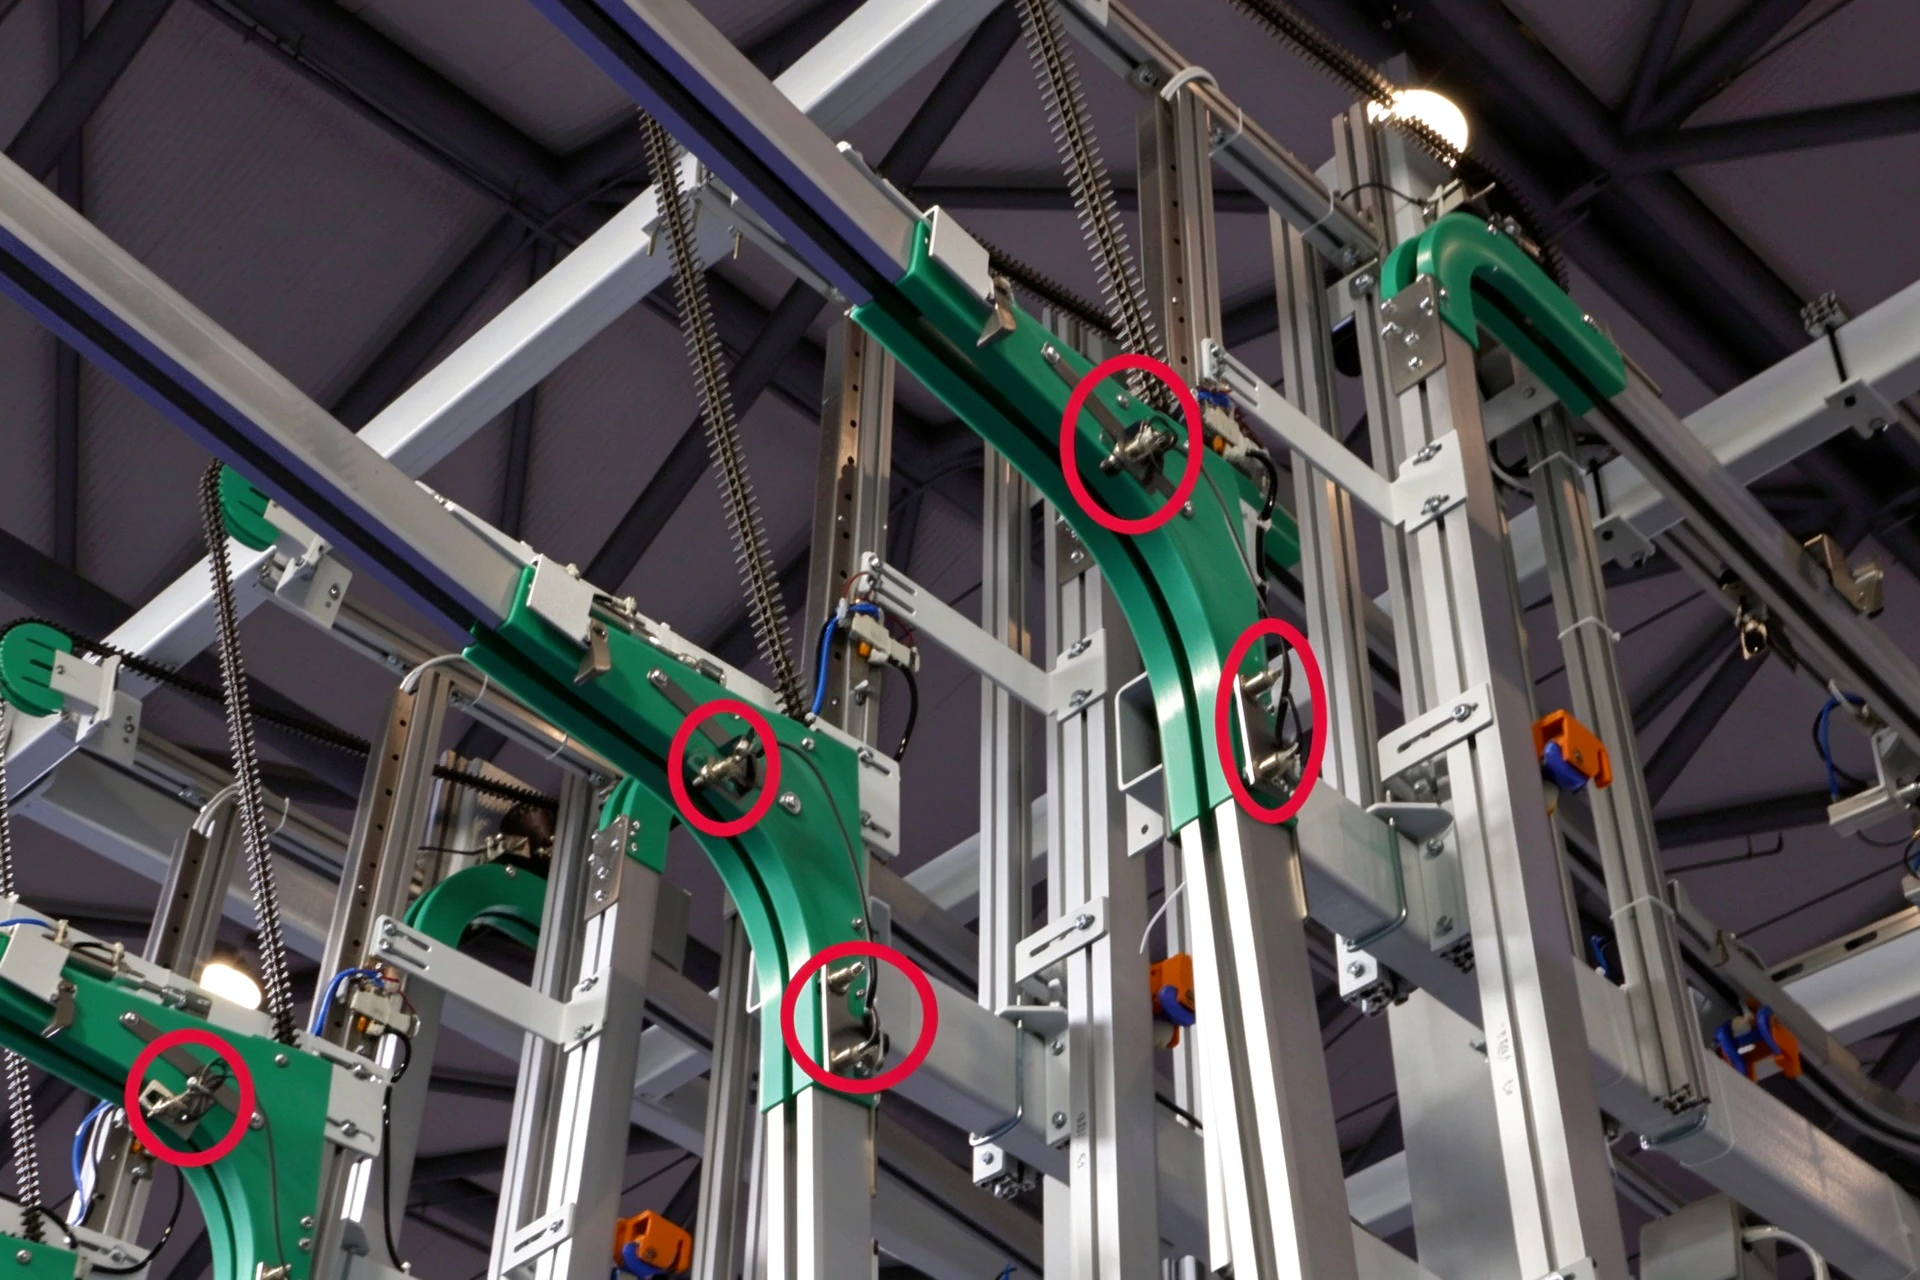 In a laundry plant, time is money: a high-speed ironing line handles dozens of meters per minute, and an undetected fault can eat a whole day’s profit in half an hour. The proximity sensor’s job is to catch the fault in the first second.
How many sensors does an industrial washing machine really carry? 04
My colleague and I started counting. On a standard tunnel ironer, besides the photoelectric switches and proximity sensors we’d already covered ——
sensors are hidden in every roller, belt, and pulley bank
▎Level sensors
in water and detergent tanks, detecting water/level to refill and dose automatically.
▎Temperature sensors
controlling heat in dryers and ironers, protecting fabric from scorching while keeping drying efficiency high.
▎Pressure sensors
monitoring steam lines and pneumatic systems — safety protection and efficiency control in one.
▎Speed sensors / encoders
checking belt and roller speed to keep every stage in sync — no stretching, no bunching.
▎Color sensors / photoelectric identification
in the sorting stage, identifying linen type and color to route baskets automatically.
In the end, even we were surprised ——
a single washing machine hides a dozen or even dozens of sensors.
They don’t speak and they’re easy to miss — some are smaller than a button — yet the machine’s rhythm, safety protection, and yield all ride on these tiny devices.
Why industrial laundry automation comes down to sensor precision and reliability — ELEsenson 05
Because this is exactly our core business.
ELEsenson has made sensors for many years — from industrial-grade photoelectric switches and proximity sensors to the increasingly popular smart sensors and AI vision inspection. We’ve seen too many industries to count — textiles, food, chemicals, logistics — and behind every automation upgrade, sensors do the foundational work.
Laundry is no different. Old-school plants relied on experienced operators watching and adjusting by feel. Today labor is more expensive and throughput demands are higher; one machine processes tons of linen a day, far beyond what the human eye can monitor.
Sensors are the “nerve endings” of industrial automation.
the more sensitive the endings, the smarter and more stable the line.
At the exhibition, we also saw the industry shifting: more and more washing equipment makers are now equipping high-quality sensors from the factory, instead of retrofitting them after a customer hits a problem. That’s a good sign. It means people are finally realizing that
in the automation race, competition often comes down to sensor precision and reliability.
— EPILOGUE —
After half a day at the show, as we walked out of the hall, a colleague said something interesting:
“I used to think of sensors as industrial parts. Now I think of them as the invisible infrastructure of every industry.”
The white towels in your hotel, the clean tablecloths in the restaurant, the sheets in the hospital — behind all of them, a highly automated laundry line is running, and every line is packed with sensors. They don’t speak, but they never stop working.
Looking for reliable photoelectric switches, proximity sensors, and smart sensing solutions for your industrial washing line? Contact ELEsenson for product selection and technical support.
Temperature sensors Product Page
Speed sensors Product Page
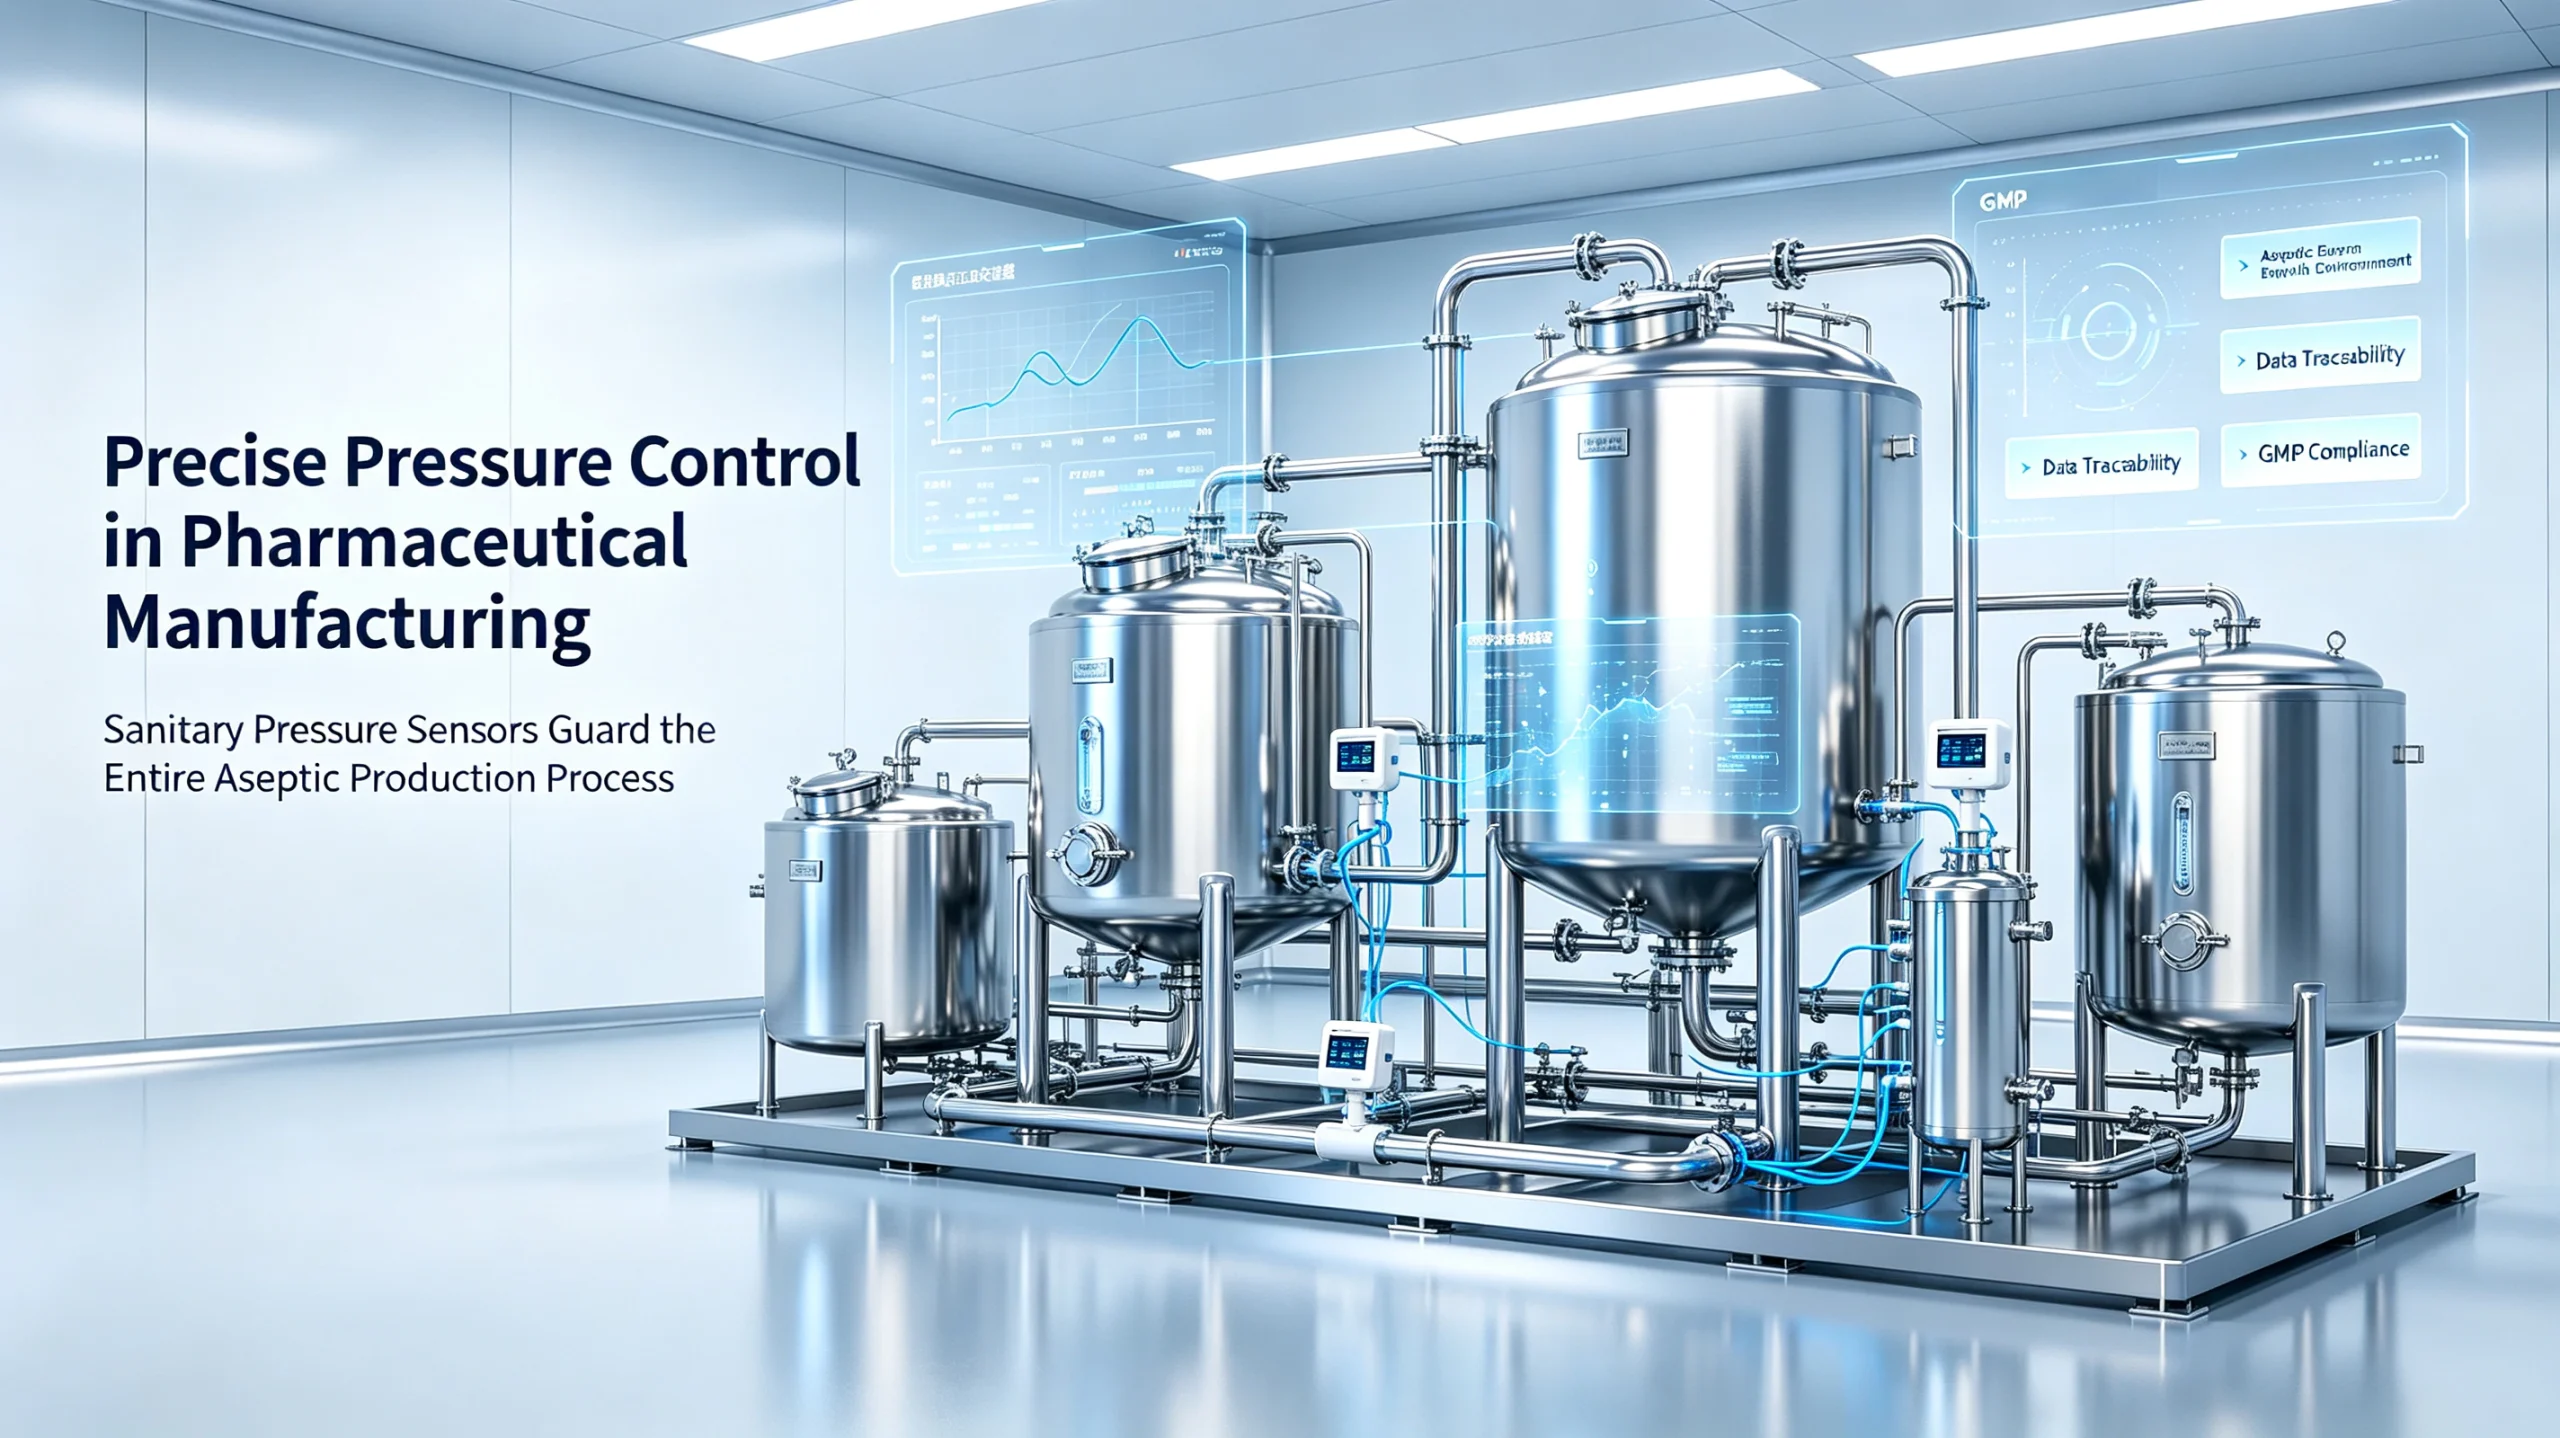
Pressure Monitoring: An Indispensable Part of Pharmaceutical Aseptic Processing
The success of pharmaceutical manufacturing lies in precise pressure control in every subtle process
Pharmaceutical manufacturing is an ultra-rigorous industry where asepsis, cleanliness, full traceability, and zero contamination serve as non-negotiable red lines. Unlike general industrial production, pharmaceutical working conditions involve frequent sterilization, repeated flushing, and ultra-high process precision, which common industrial measuring instruments cannot withstand.
As a core process parameter, pressure directly determines drug quality, production safety, and GMP audit compliance. Stable and accurate pressure monitoring has become a fundamental guarantee for standardized pharmaceutical production.
The full-process functional tanks in pharmaceutical production require sanitary pressure sensors for real-time pressure monitoring. These sensors realize process pressure stabilization, safety protection, and data traceability, covering all core pharmaceutical tank scenarios as follows:
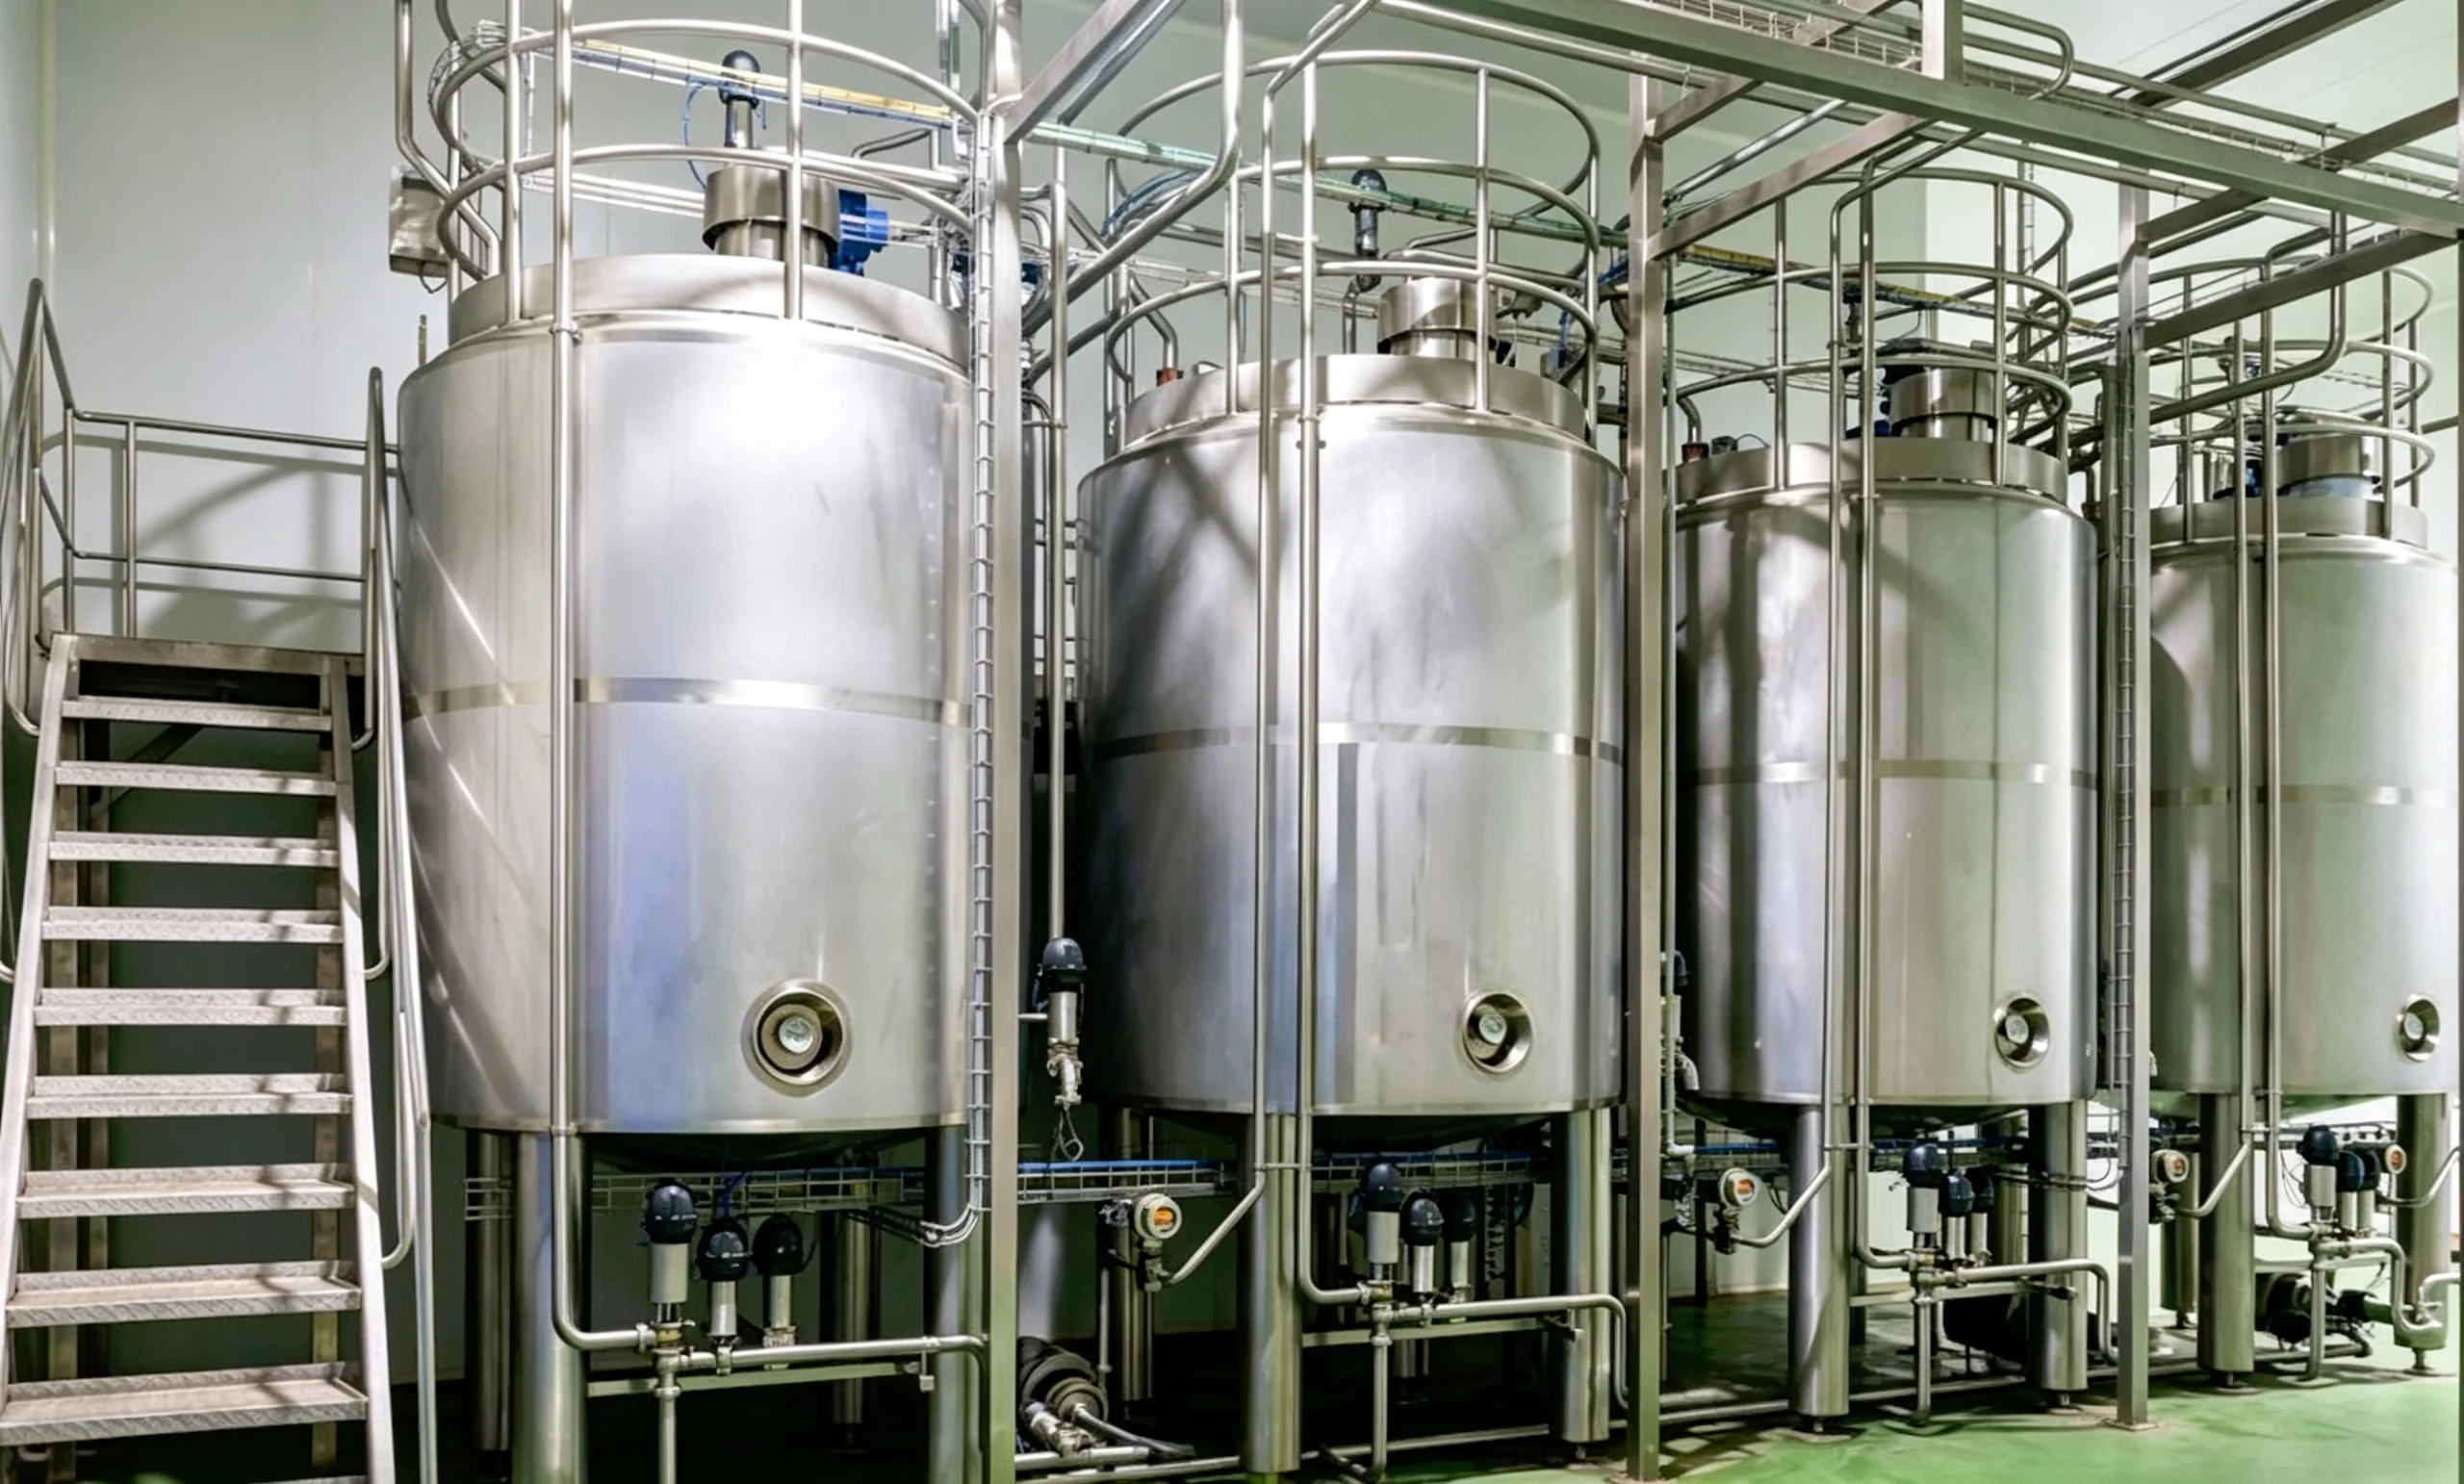
Bioreactors & Strain Culture Tanks
Widely used in the production of vaccines, antibiotics, probiotics, and biological preparations, these tanks are the core reaction vessels in biopharmaceuticals. Internal pressure directly affects strain growth and metabolic efficiency. Excessive positive pressure will damage strain activity, while unbalanced negative pressure will cause external miscellaneous bacteria inhalation, leading to contamination and scrapping of the entire batch of materials. Real-time micro-positive and constant pressure monitoring via sanitary sensors maintains a sterile and stable reaction environment for strain cultivation.
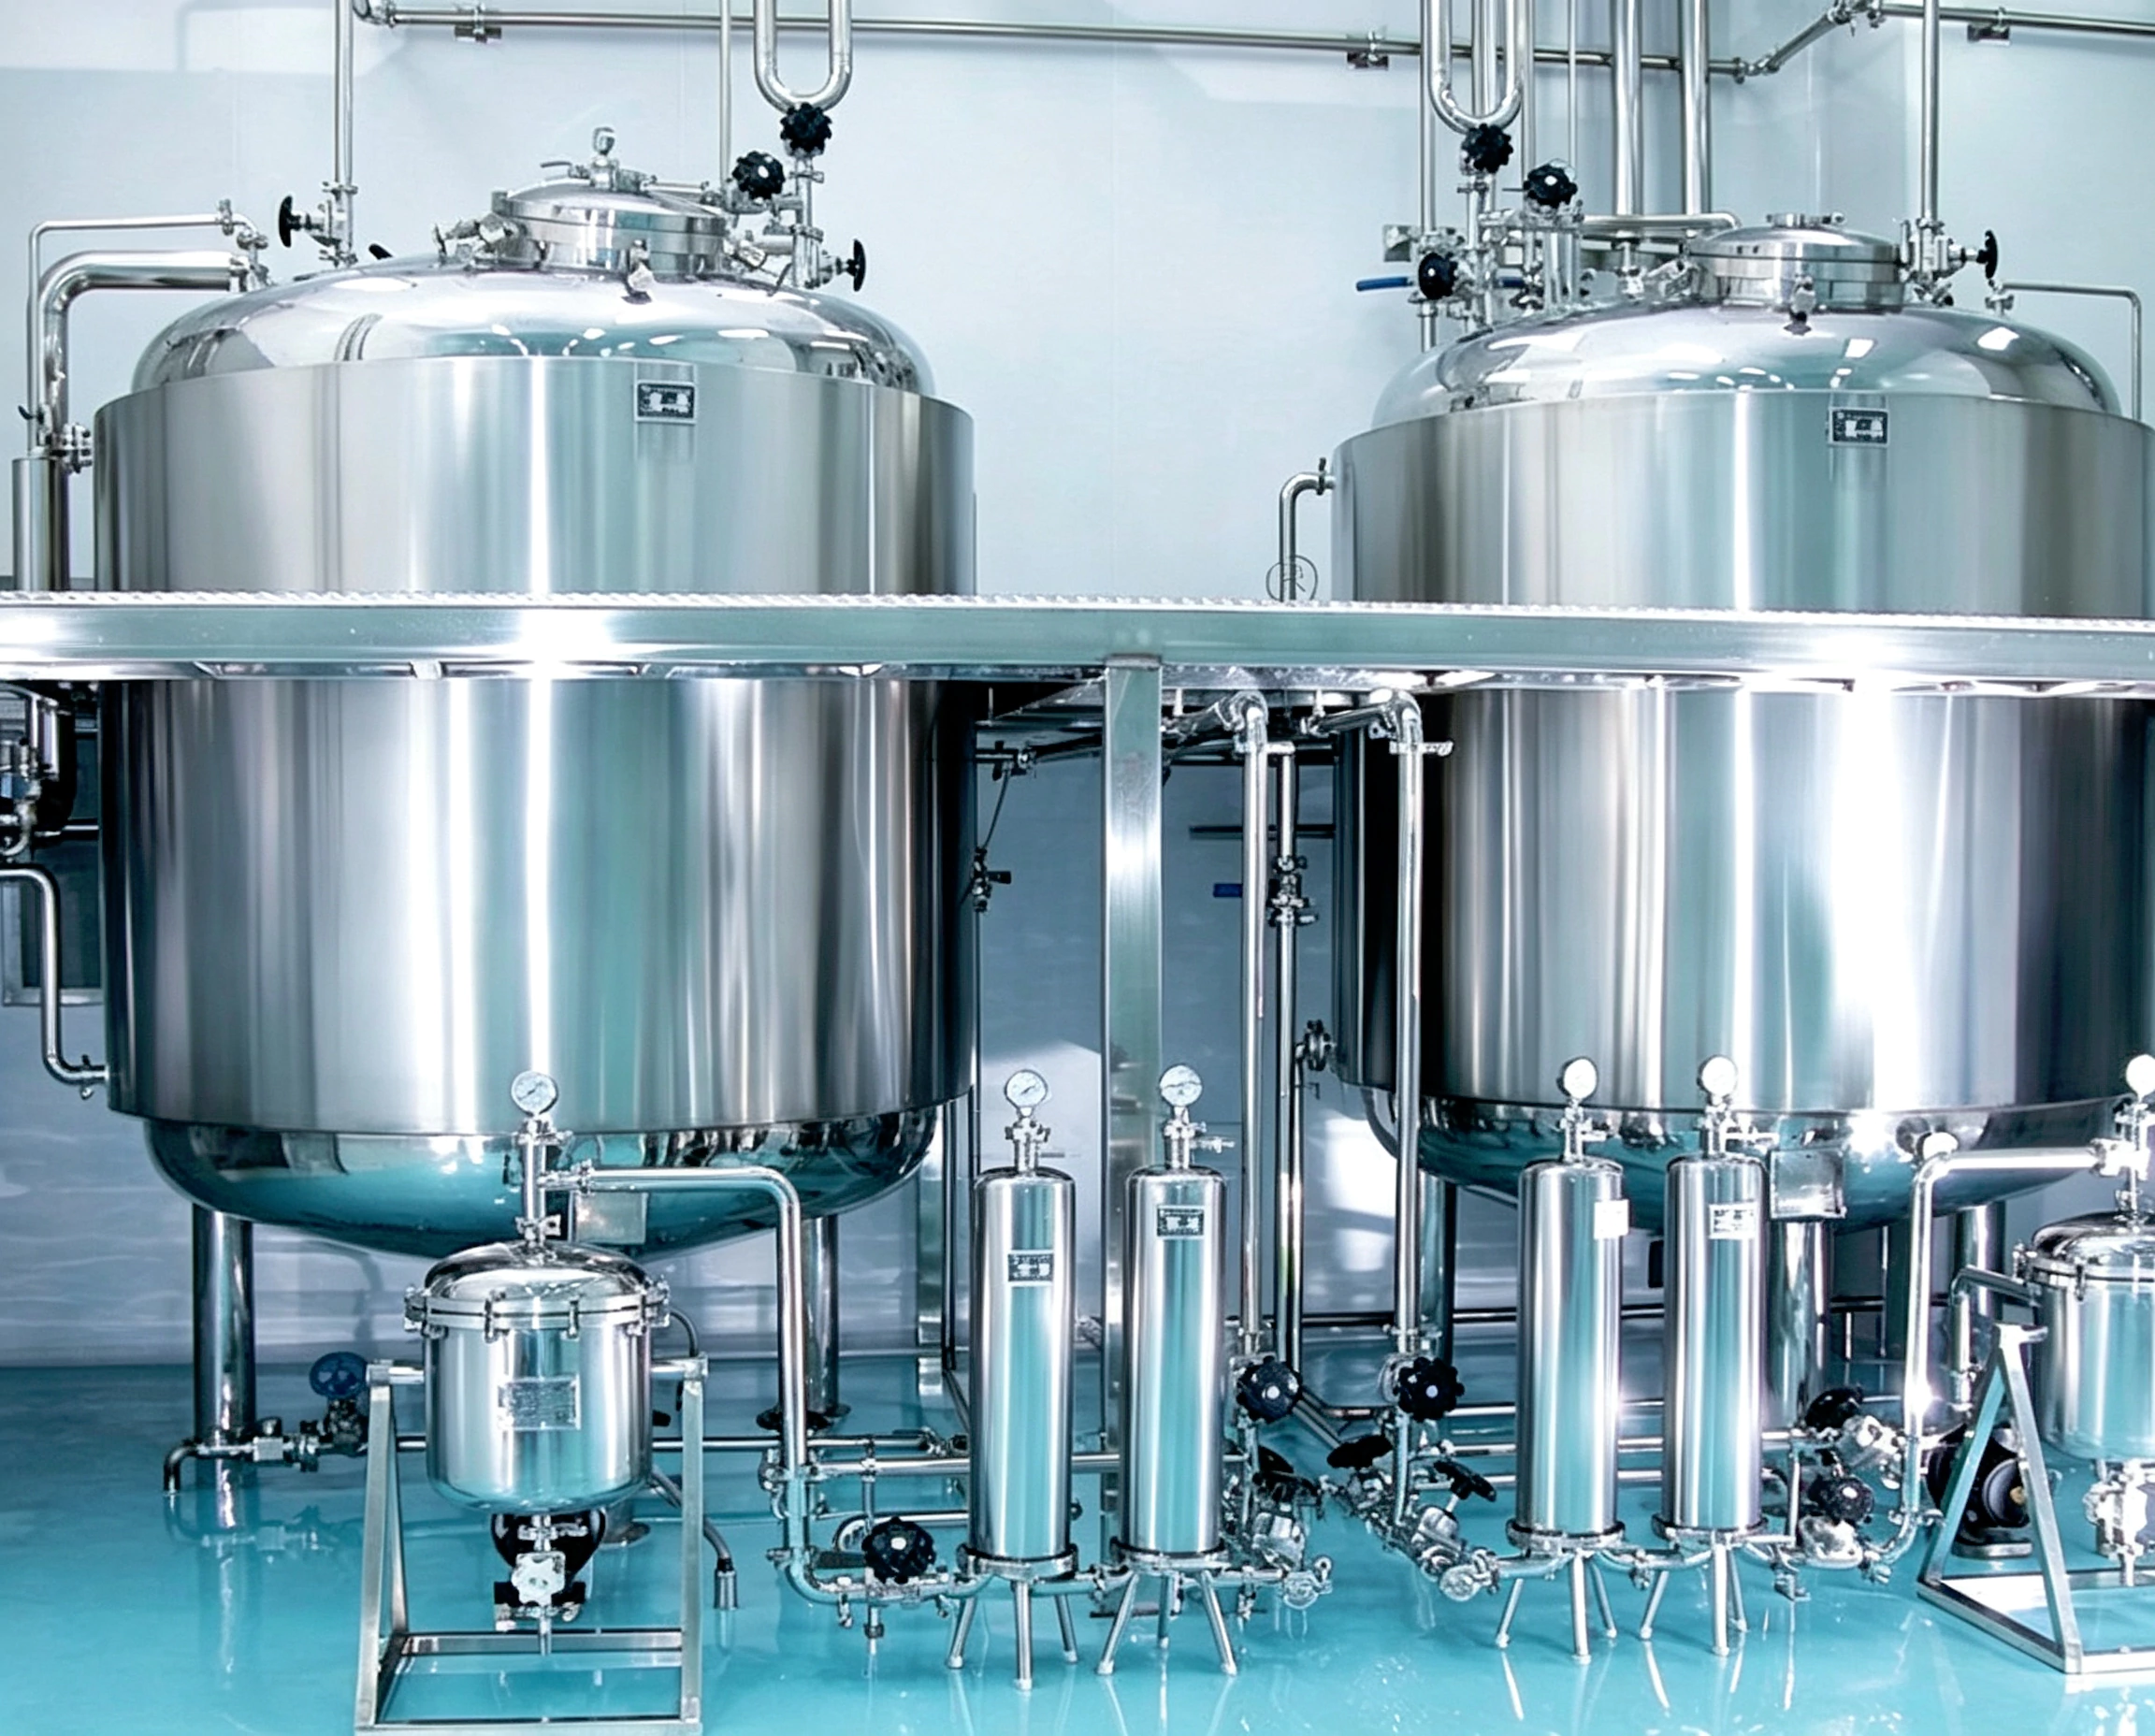
Liquid Preparation & Storage Tanks
These tanks are applied for the batching and temporary storage of injections, oral liquids, sterile preparations, and API materials. Pressure fluctuations will cause unbalanced liquid batching and disordered flow velocity, undermining batch consistency of finished drugs. Continuous pressure monitoring and stabilization effectively avoid material deviation and contamination risks caused by abnormal pressure, ensuring stable liquid preparation processes.
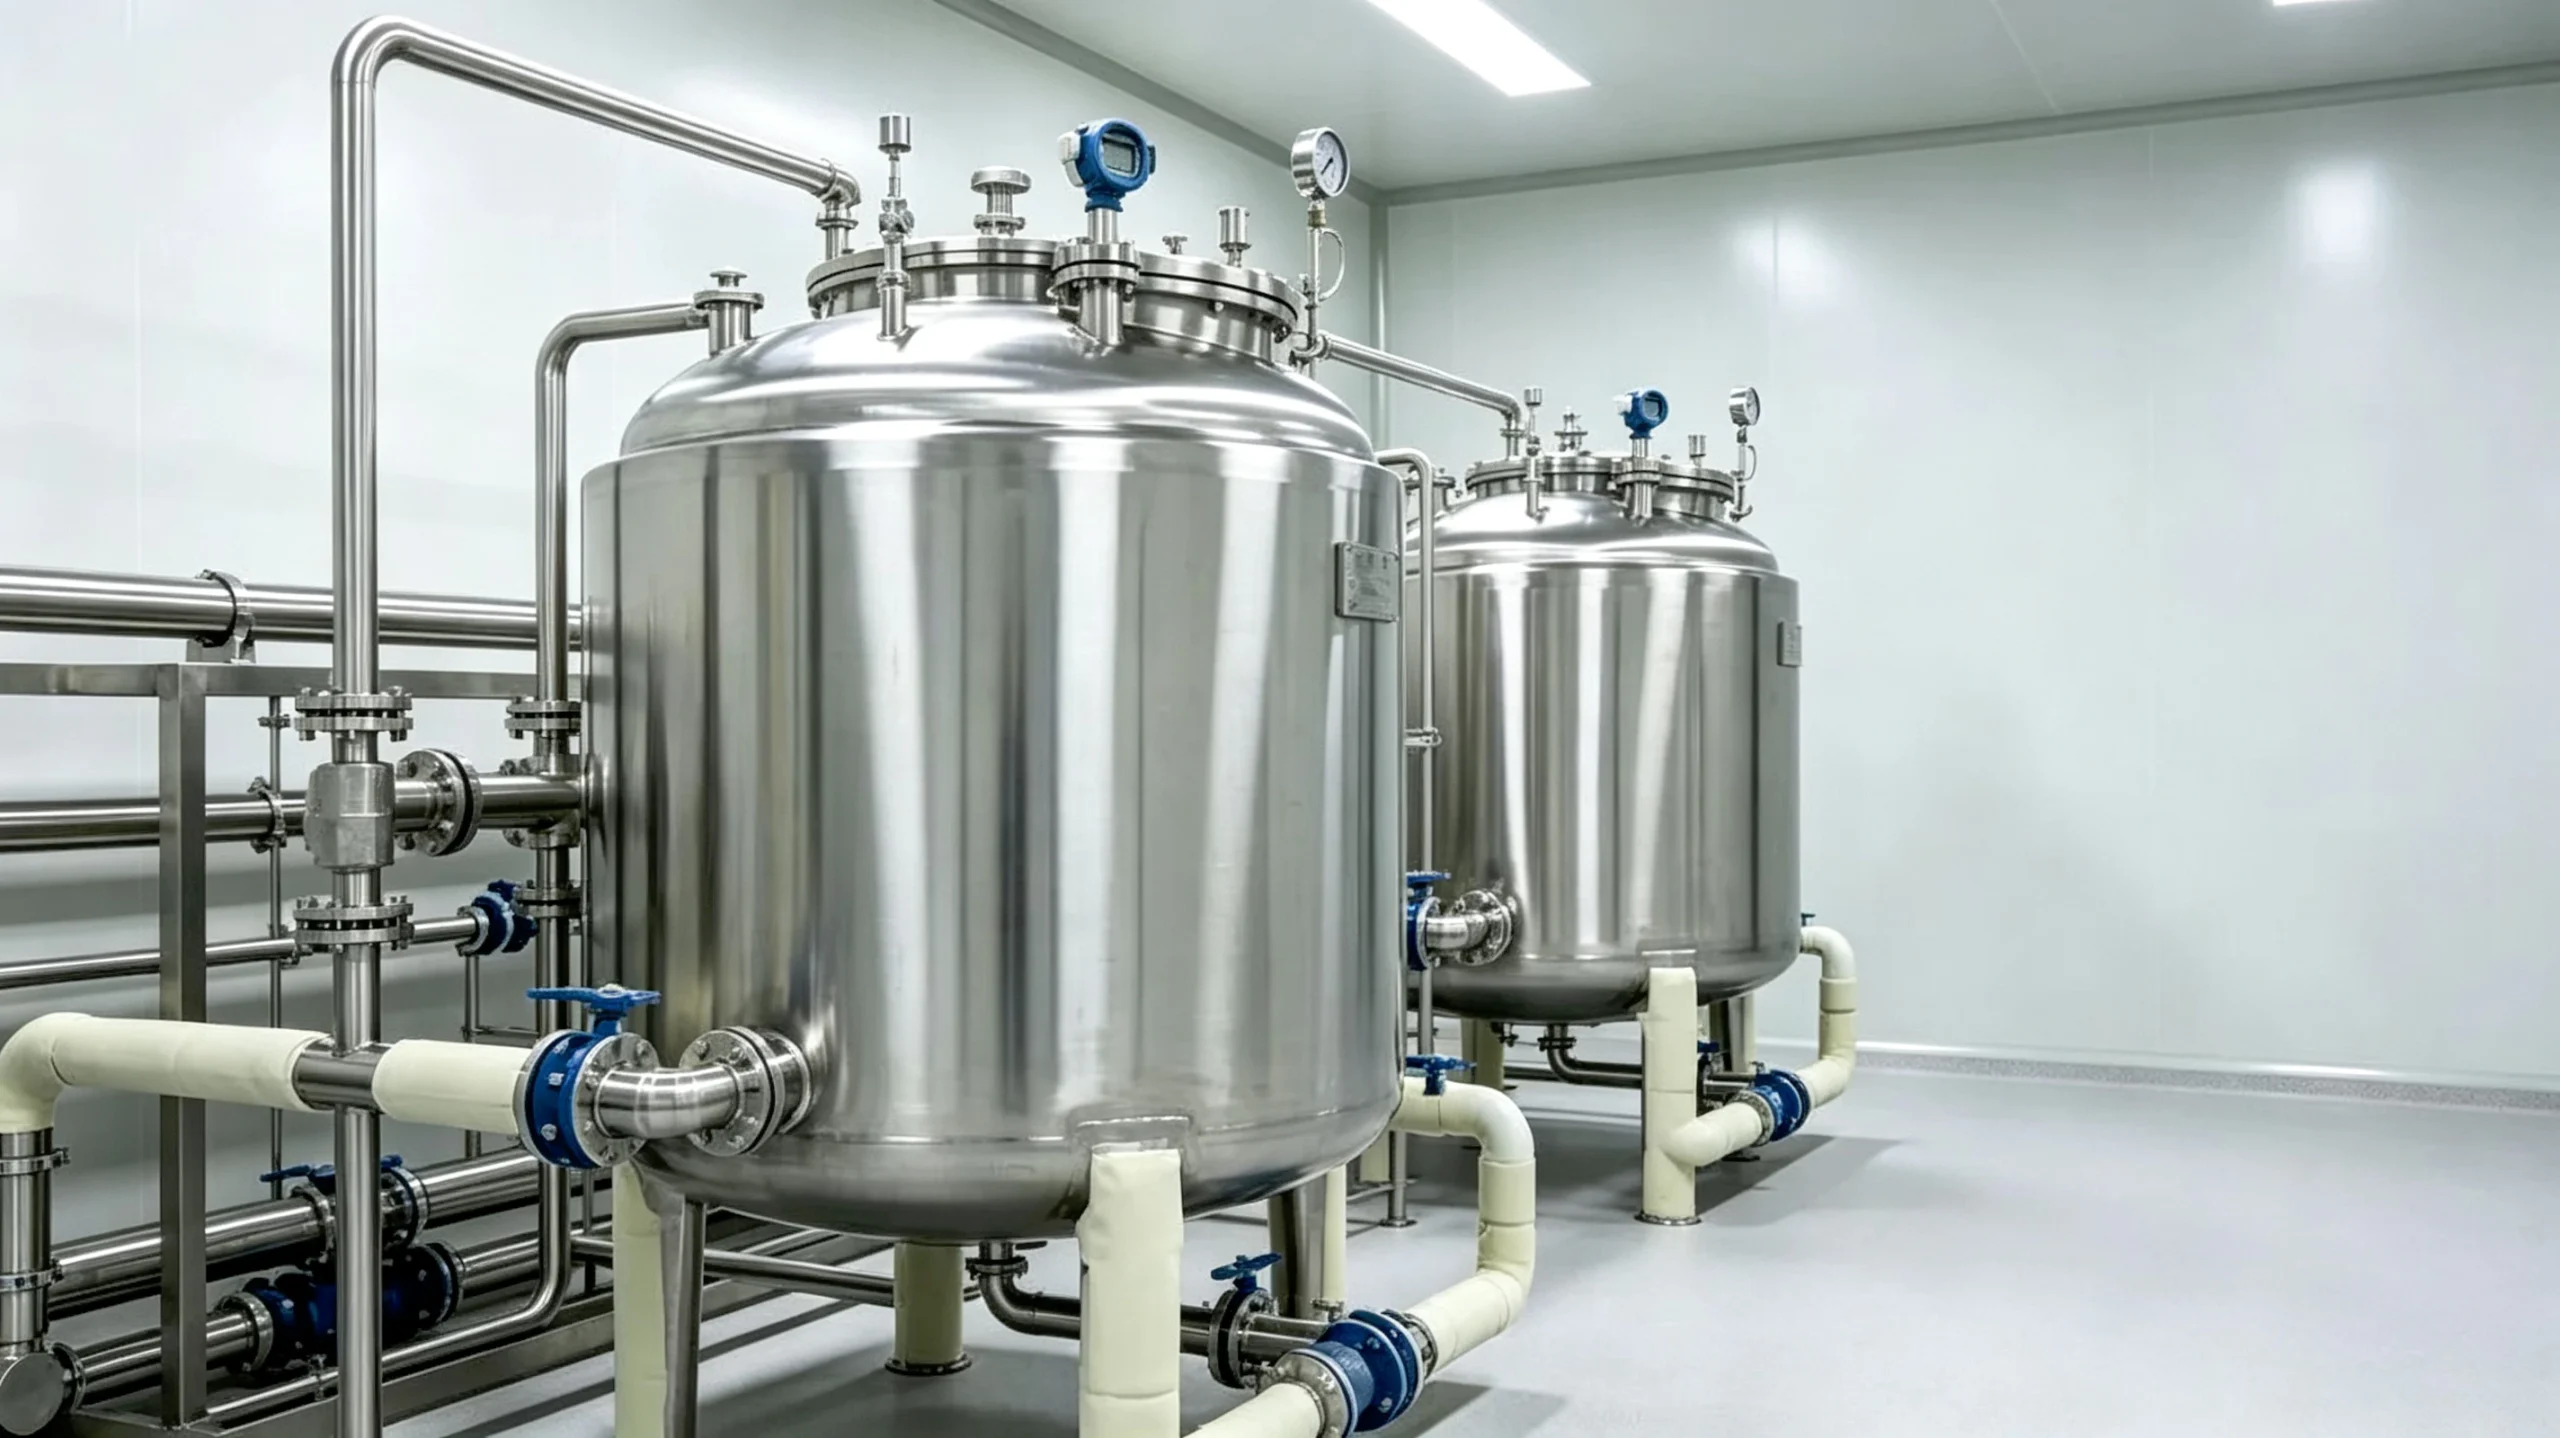
Purified Water & Water for Injection (WFI) Storage Tanks
As core utility equipment in pharmaceutical factories, these tanks store sterile production-grade pure water. Negative pressure imbalance easily causes air backflow and secondary water pollution, which is a key inspection item in GMP audits. Pressure sensors sustain stable positive pressure inside the tanks, eliminating contamination hazards and guaranteeing full-process clean water safety for production.
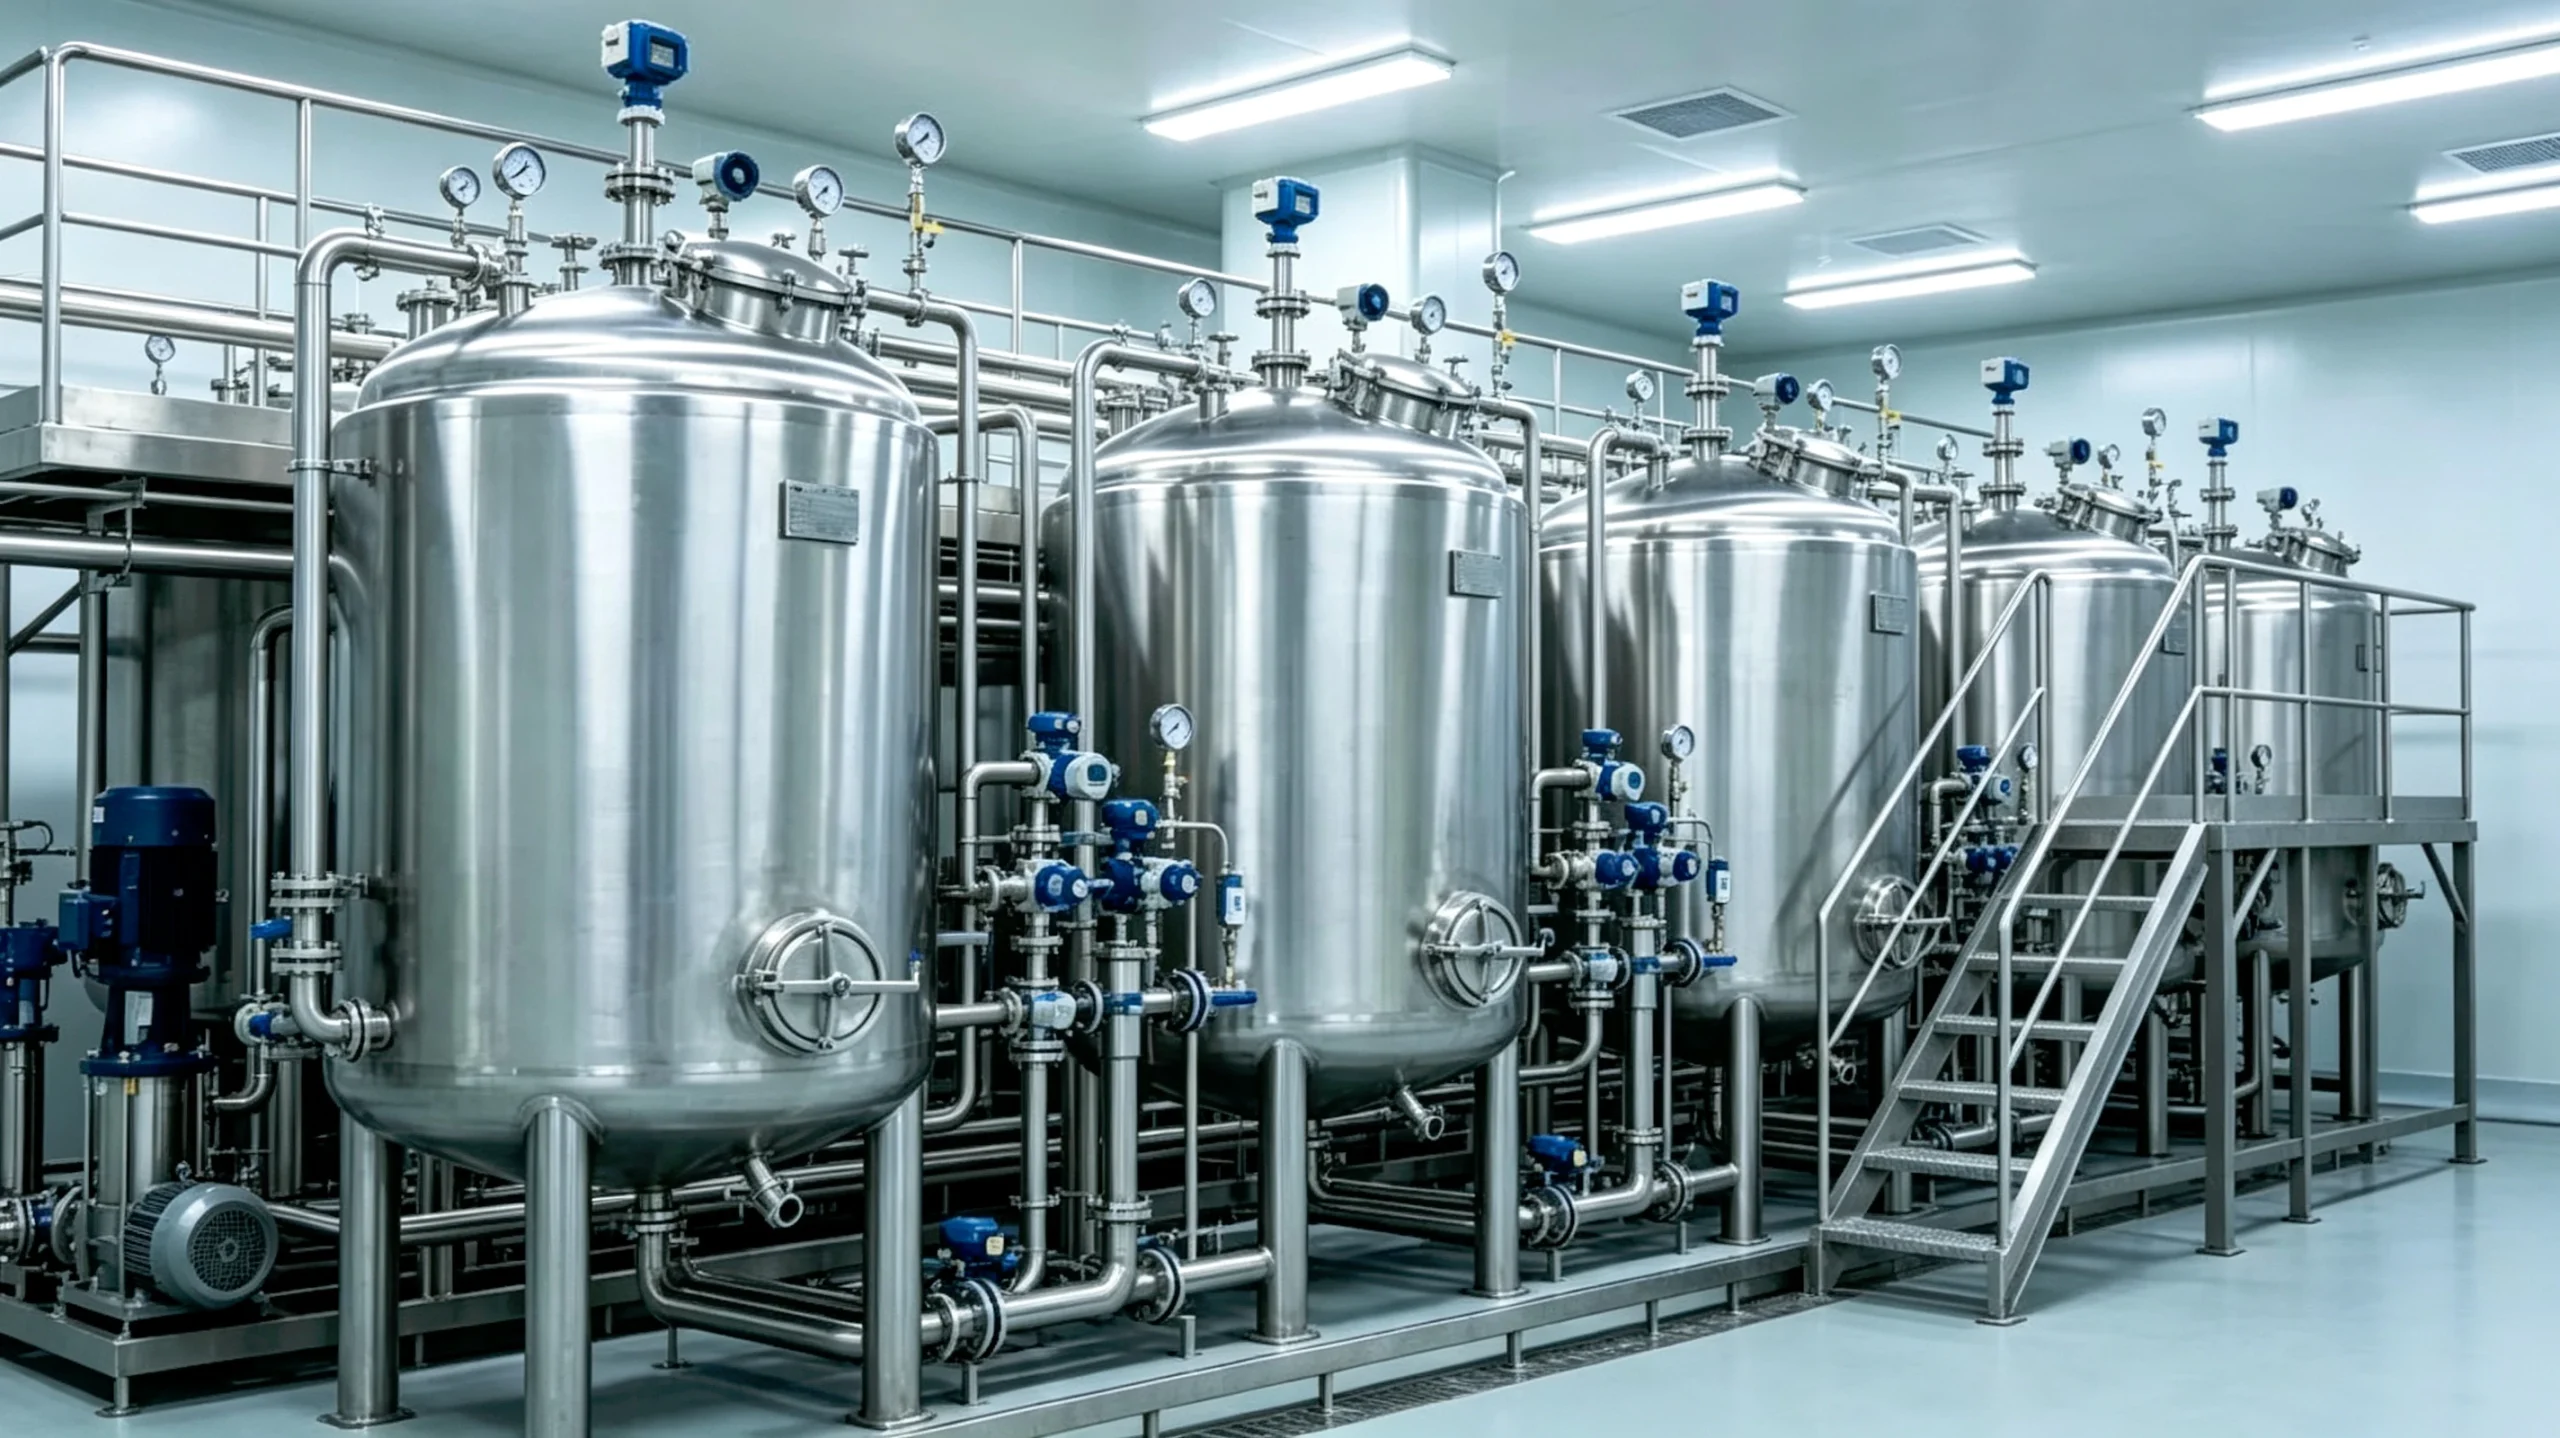
Buffer & Pressure Stabilization Tanks
Designed for pipeline pressure stabilization, airflow buffering, and material transfer, these tanks balance pressure fluctuations in the entire production pipeline. They effectively prevent sudden pressure shocks to tanks and precision equipment, ensuring uninterrupted continuous aseptic production.
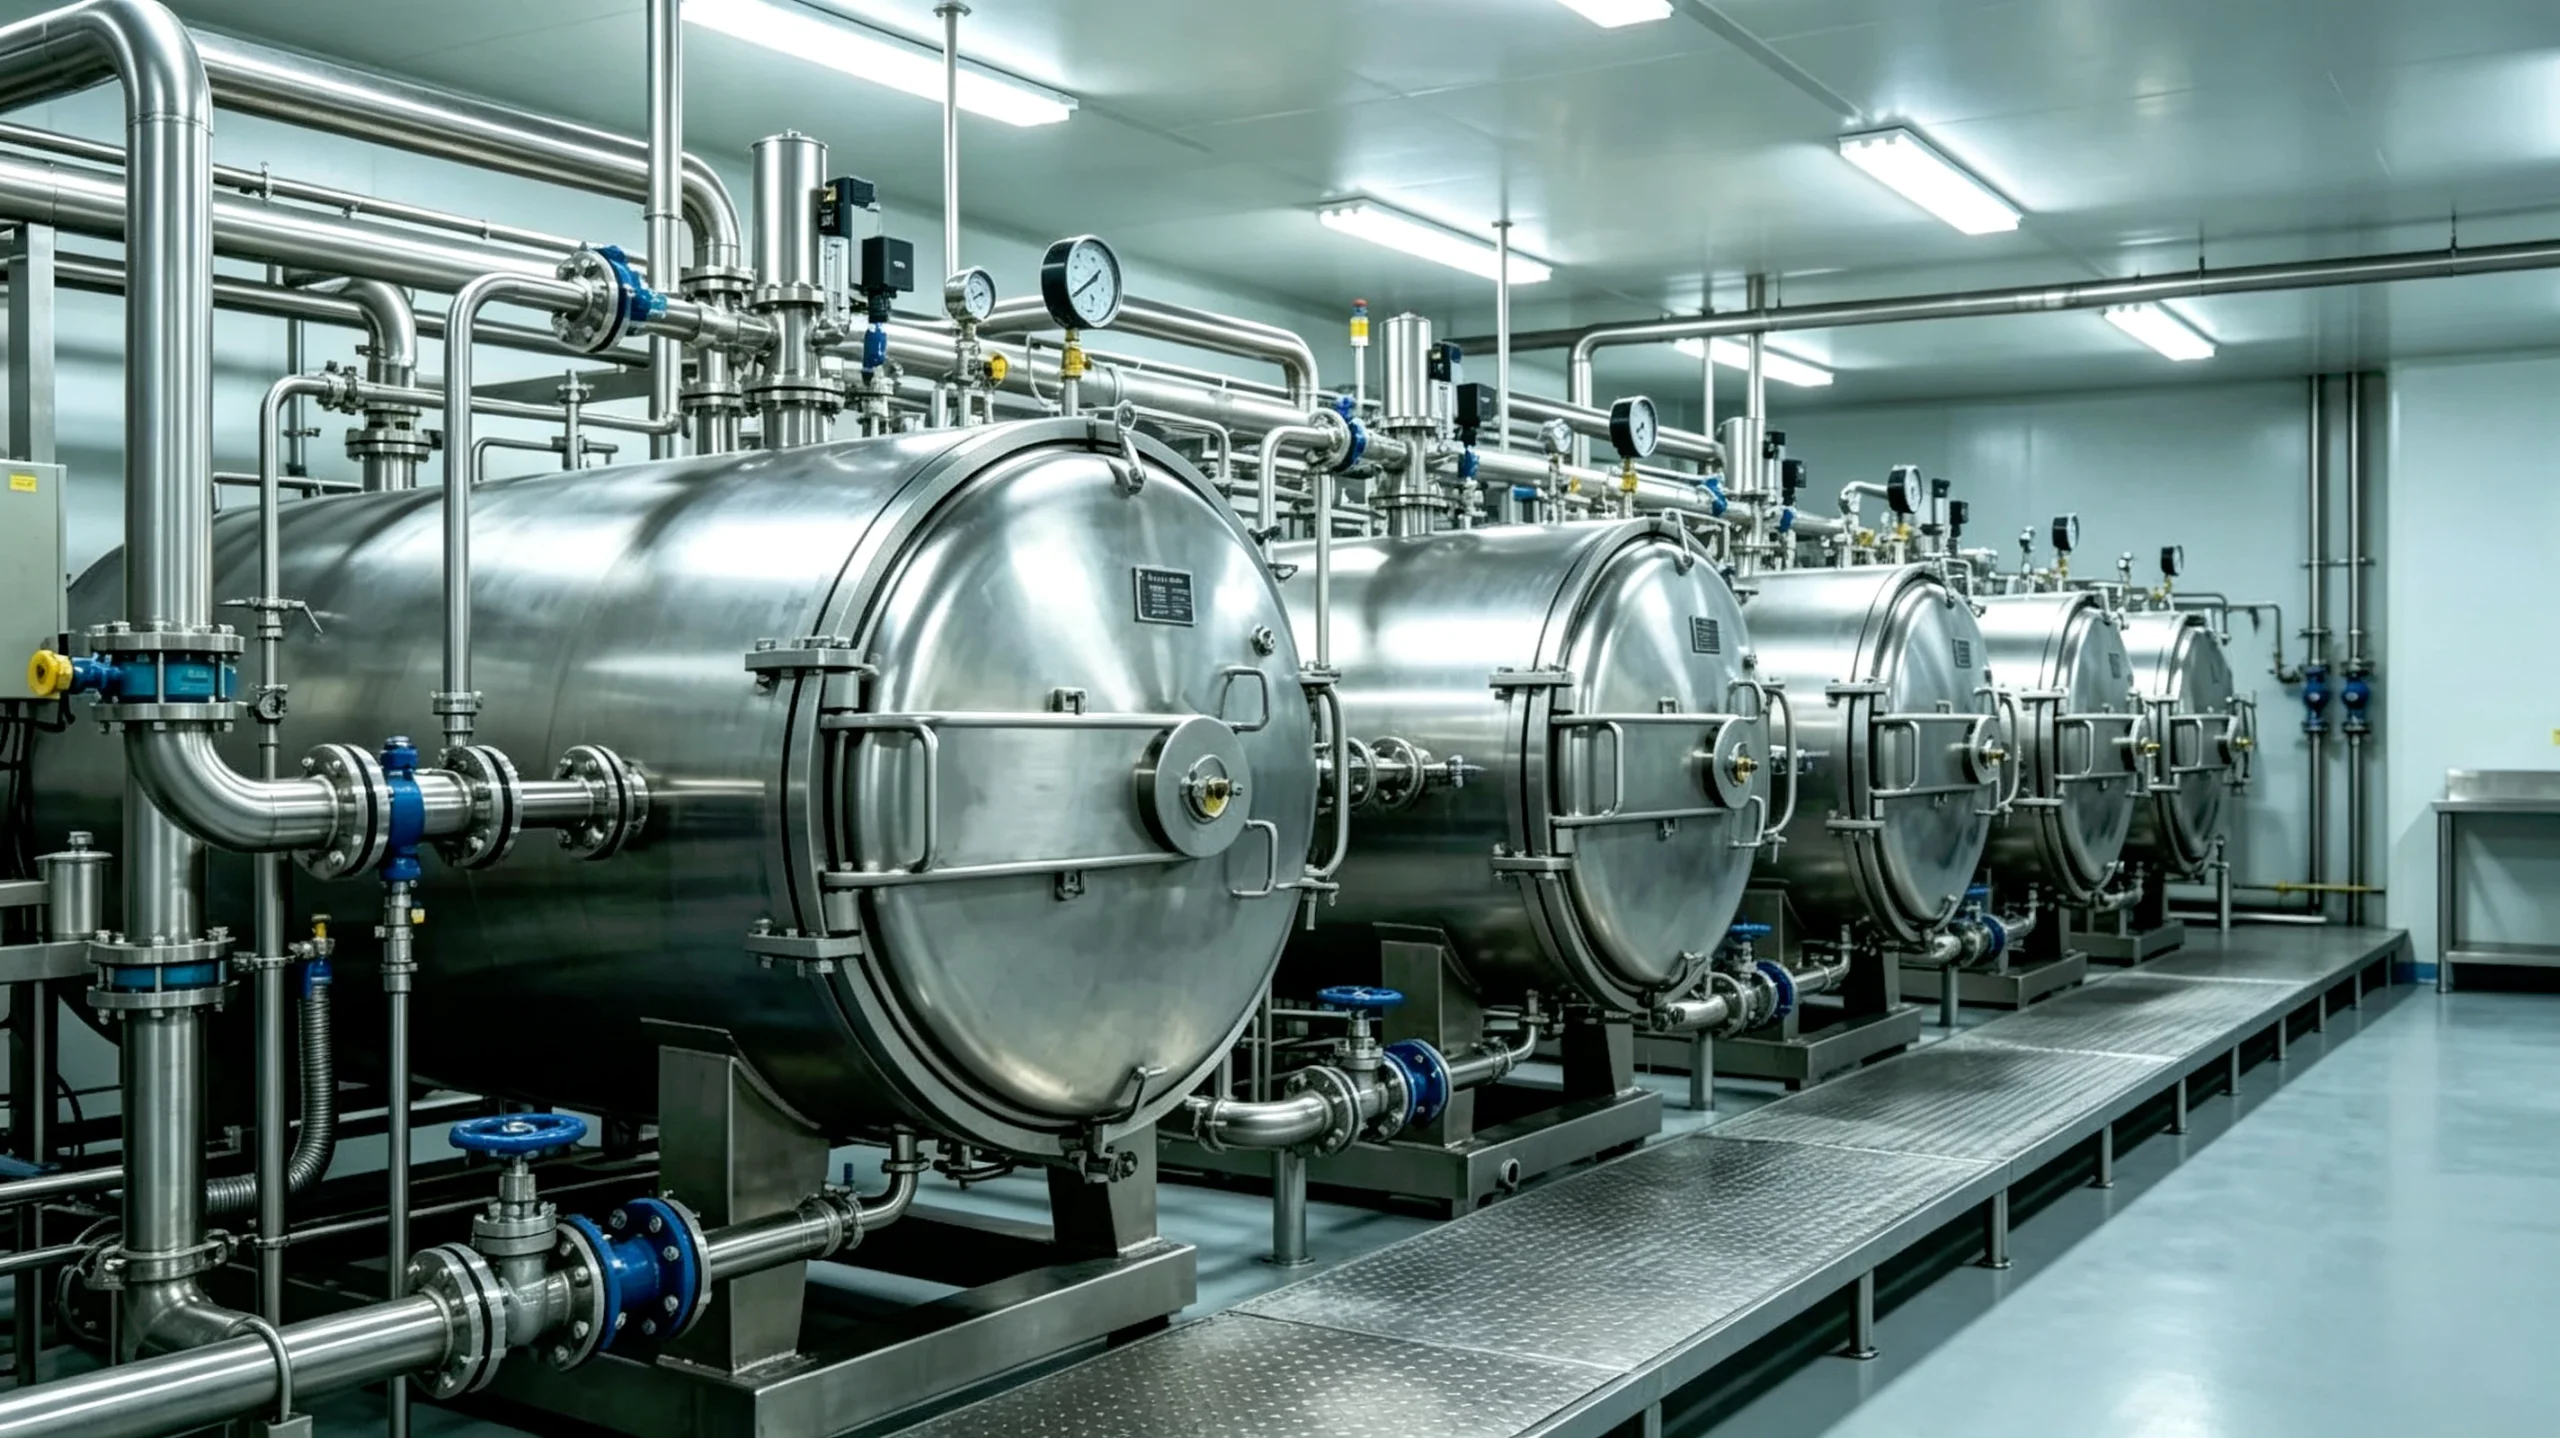
Sterilization Tanks & Autoclave Pressure Vessels
Responsible for SIP high-temperature sterilization of drugs, utensils, and pipelines, these vessels operate under long-term high-temperature (121℃-134℃) steam and high-pressure working conditions. Sensors monitor pressure parameters throughout the sterilization process to ensure compliant sterilization temperature and pressure, meeting process verification and GMP data traceability requirements.
Vacuum Concentration & Freeze-Drying Supporting Tanks
Used for liquid concentration, low-temperature purification, and freeze-drying pretreatment, these tanks work under long-term negative vacuum conditions. High-precision negative pressure monitoring optimizes liquid concentration efficiency, prevents loss of active pharmaceutical ingredients, and maintains a sterile vacuum production environment.
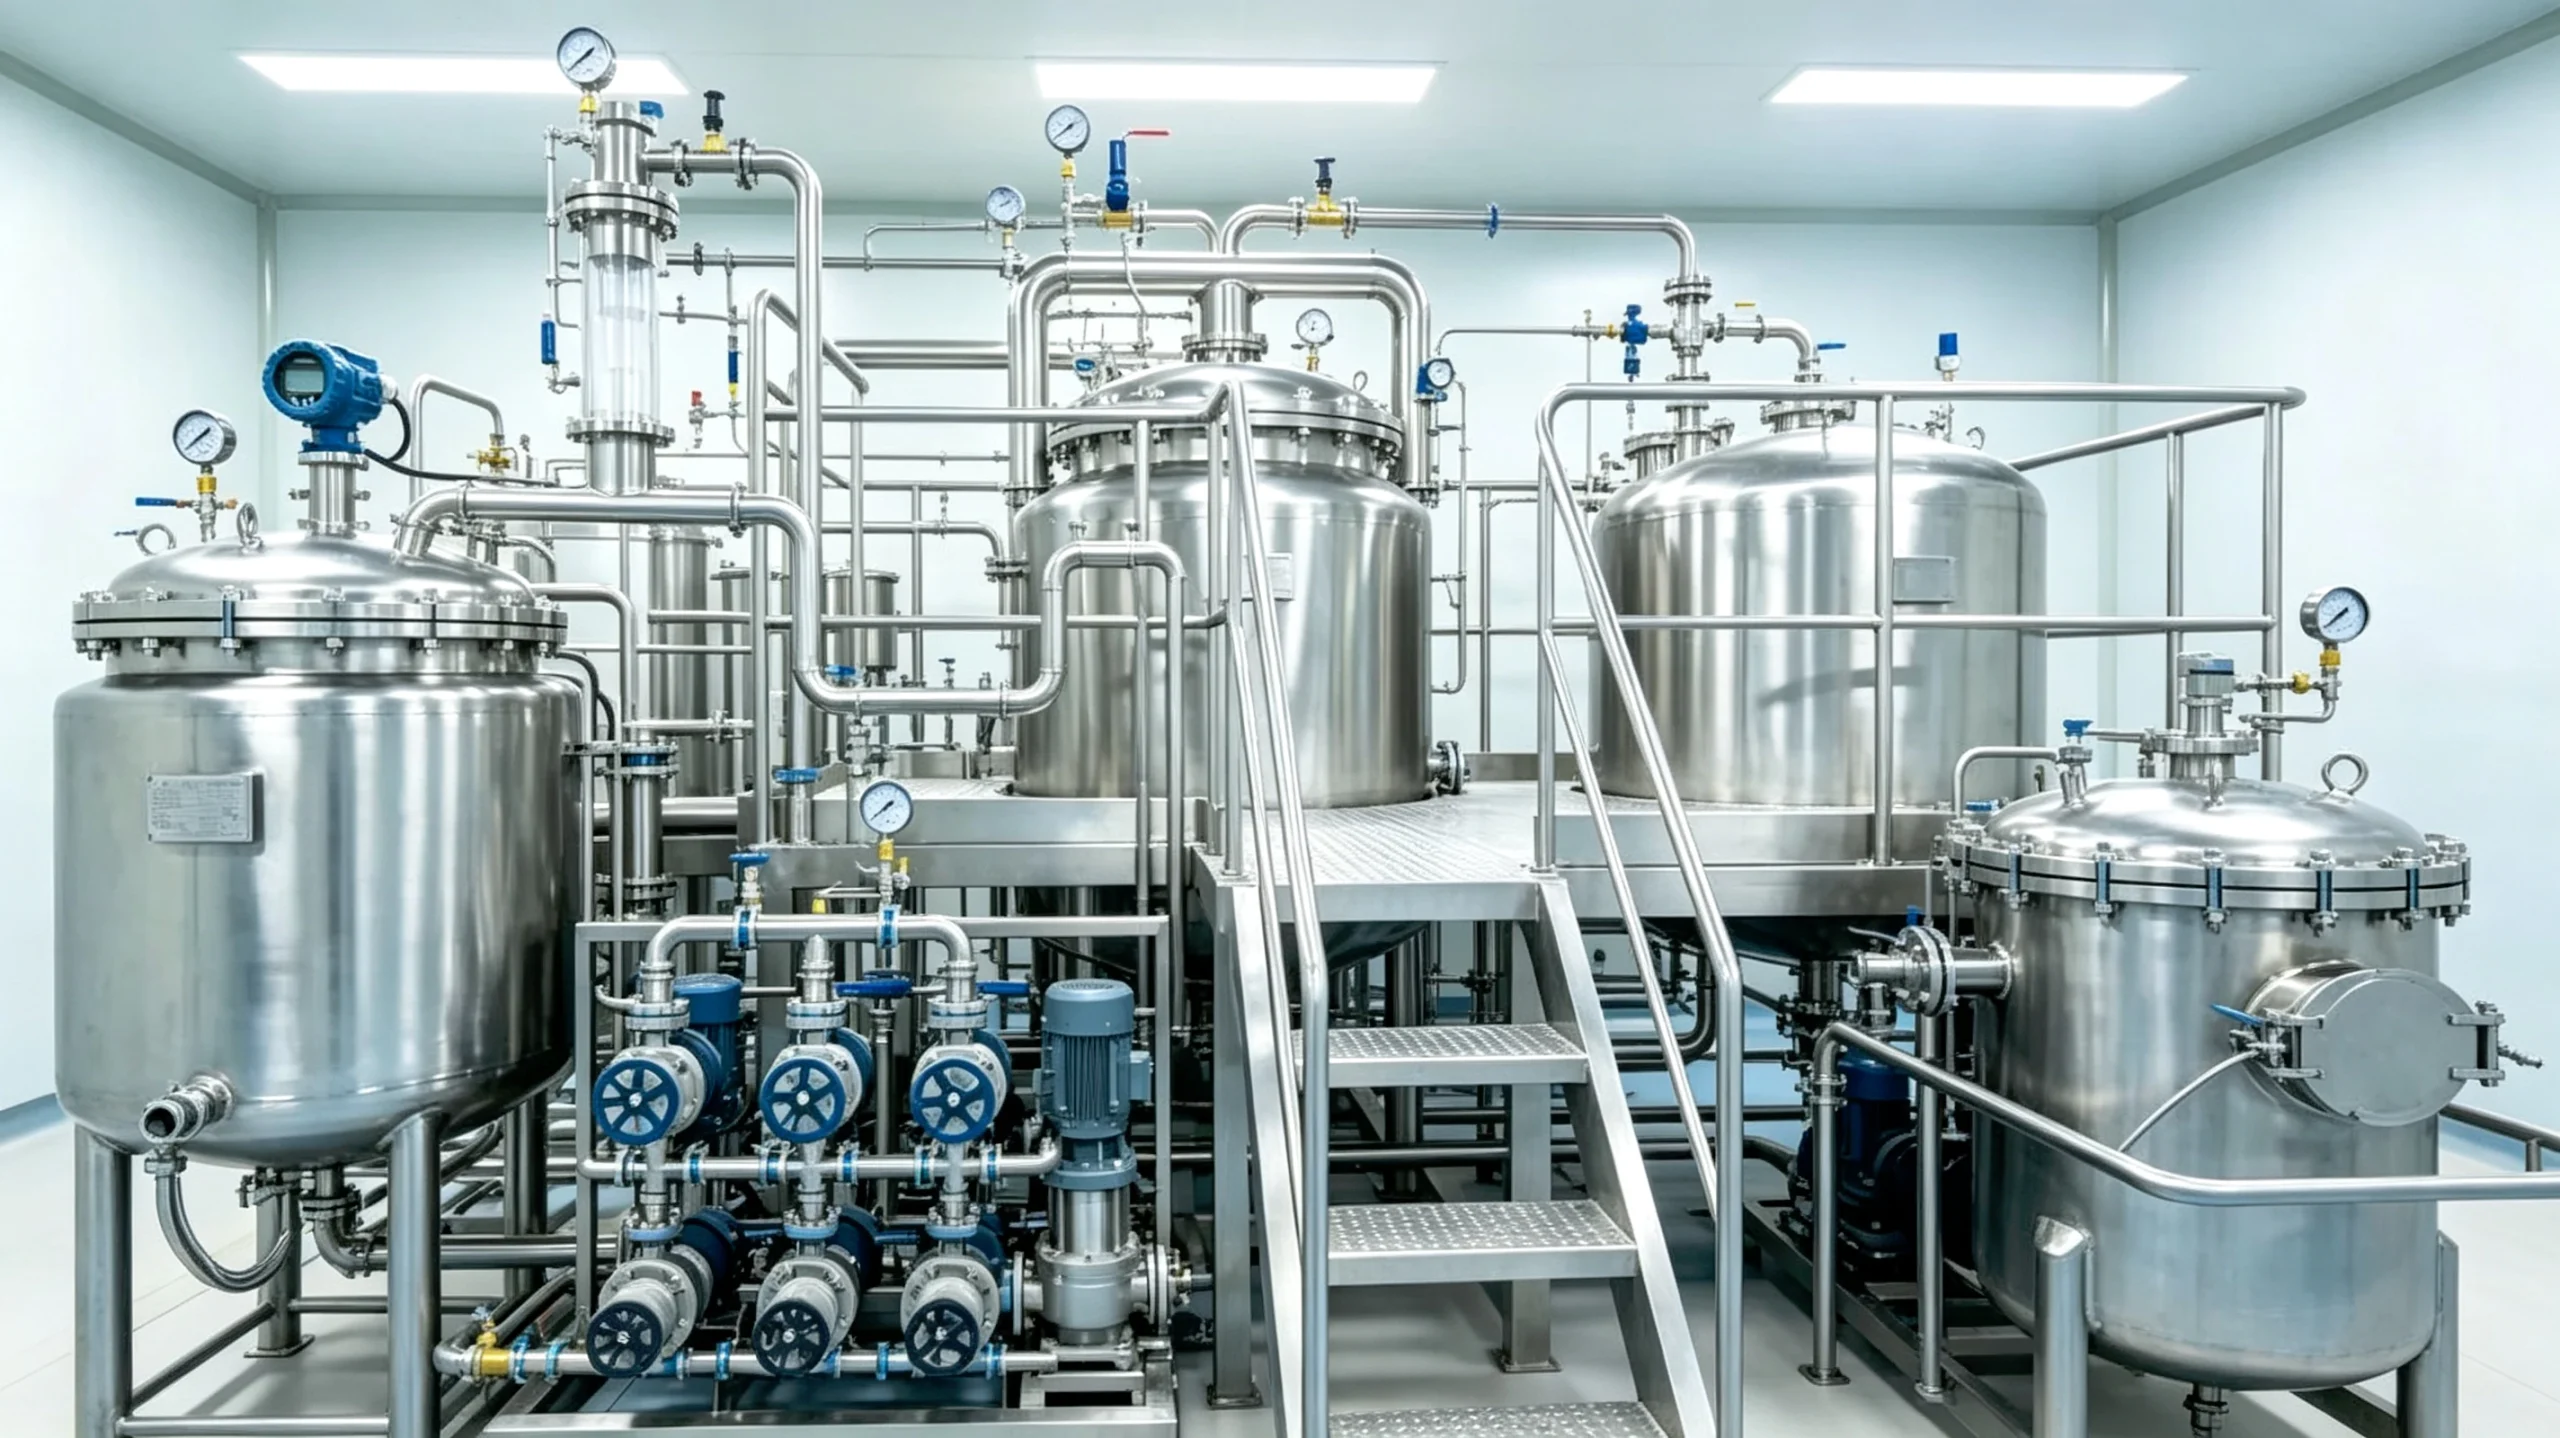
Pharmaceutical tank sensors are in direct contact with drugs, strains, and sterile pure water, facing high-frequency sterilization and zero-tolerance cleanliness conditions. Therefore, sanitary pressure sensors for pharmaceuticals have exclusive industry-hardened standards, which are core selection criteria for pharmaceutical enterprises:
Dead-Zone Free Sanitary Structure to Eliminate Residue Contamination
Pharmaceutical media containing protein, polysaccharides, and solutes are prone to adhesion and residue. Ordinary sensors with concave diaphragms and thread gaps accumulate materials and breed bacteria and molds, destroying the sterile tank environment. Professional pharmaceutical pressure sensors adopt a flush diaphragm integrated dead-zone free design, with smooth, seamless and groove-free wetted surfaces and integral seamless welding. The structure allows thorough cleaning via CIP flushing, completely eliminating residual contamination and passing pharmaceutical sterile cleaning verification.
316L Stainless Steel Material with Zero Precipitation & Zero Medium Contamination
Since sensors are directly connected to sterile tanks and contact pharmaceutical raw materials, the industry mandates 316L stainless steel wetted parts with mirror polishing treatment. The material features excellent corrosion resistance and oxidation resistance, avoiding chemical reactions with liquids and acid-base sterilization media. It achieves zero heavy metal precipitation and qualified biocompatibility, completely preventing secondary contamination of pharmaceutical materials.
Resistant to Frequent CIP/SIP Sterilization for Long-Term Stable Operation
Pharmaceutical tanks undergo daily CIP online cleaning and SIP high-temperature steam sterilization, with frequent cold and heat alternation and acid-base corrosion. Ordinary sensors suffer from seal aging, data drift, and water ingress failure in such harsh conditions. Professional pharmaceutical sensors adapt to high-frequency sterilization scenarios, enduring long-term 134℃ high-temperature steam scouring and acid-base corrosion. They maintain consistent measurement accuracy before and after sterilization without frequent calibration, matching daily sterile disinfection workflows.
Quick Sanitary Clamp Interface for Clean & Efficient Maintenance
Pharmaceutical tanks require regular opening disinfection, equipment calibration, and disassembly maintenance. Threaded connections with dead corners are forbidden to avoid dust and bacterial accumulation. Adopting standard sanitary quick clamp interfaces, the sensors feature convenient disassembly and tight seamless docking. The maintenance process will not damage the sterile environment of clean workshops, fully complying with standardized pharmaceutical factory operation and maintenance specifications.
High Precision & Full Traceability for GMP Audit Compliance
Tank pressure data is the core basis for pharmaceutical process verification and official GMP audits. Equipped with high-precision cores, pharmaceutical pressure sensors capture subtle fluctuations in micro-pressure, negative pressure and high pressure with stable and jitter-free data. Supporting 4-20mA and RS485 signal output, they seamlessly connect with pharmaceutical MES and PLC systems to automatically record full-process pressure data. The traceable and tamper-proof data provides solid technical support for process compliance and batch quality control.
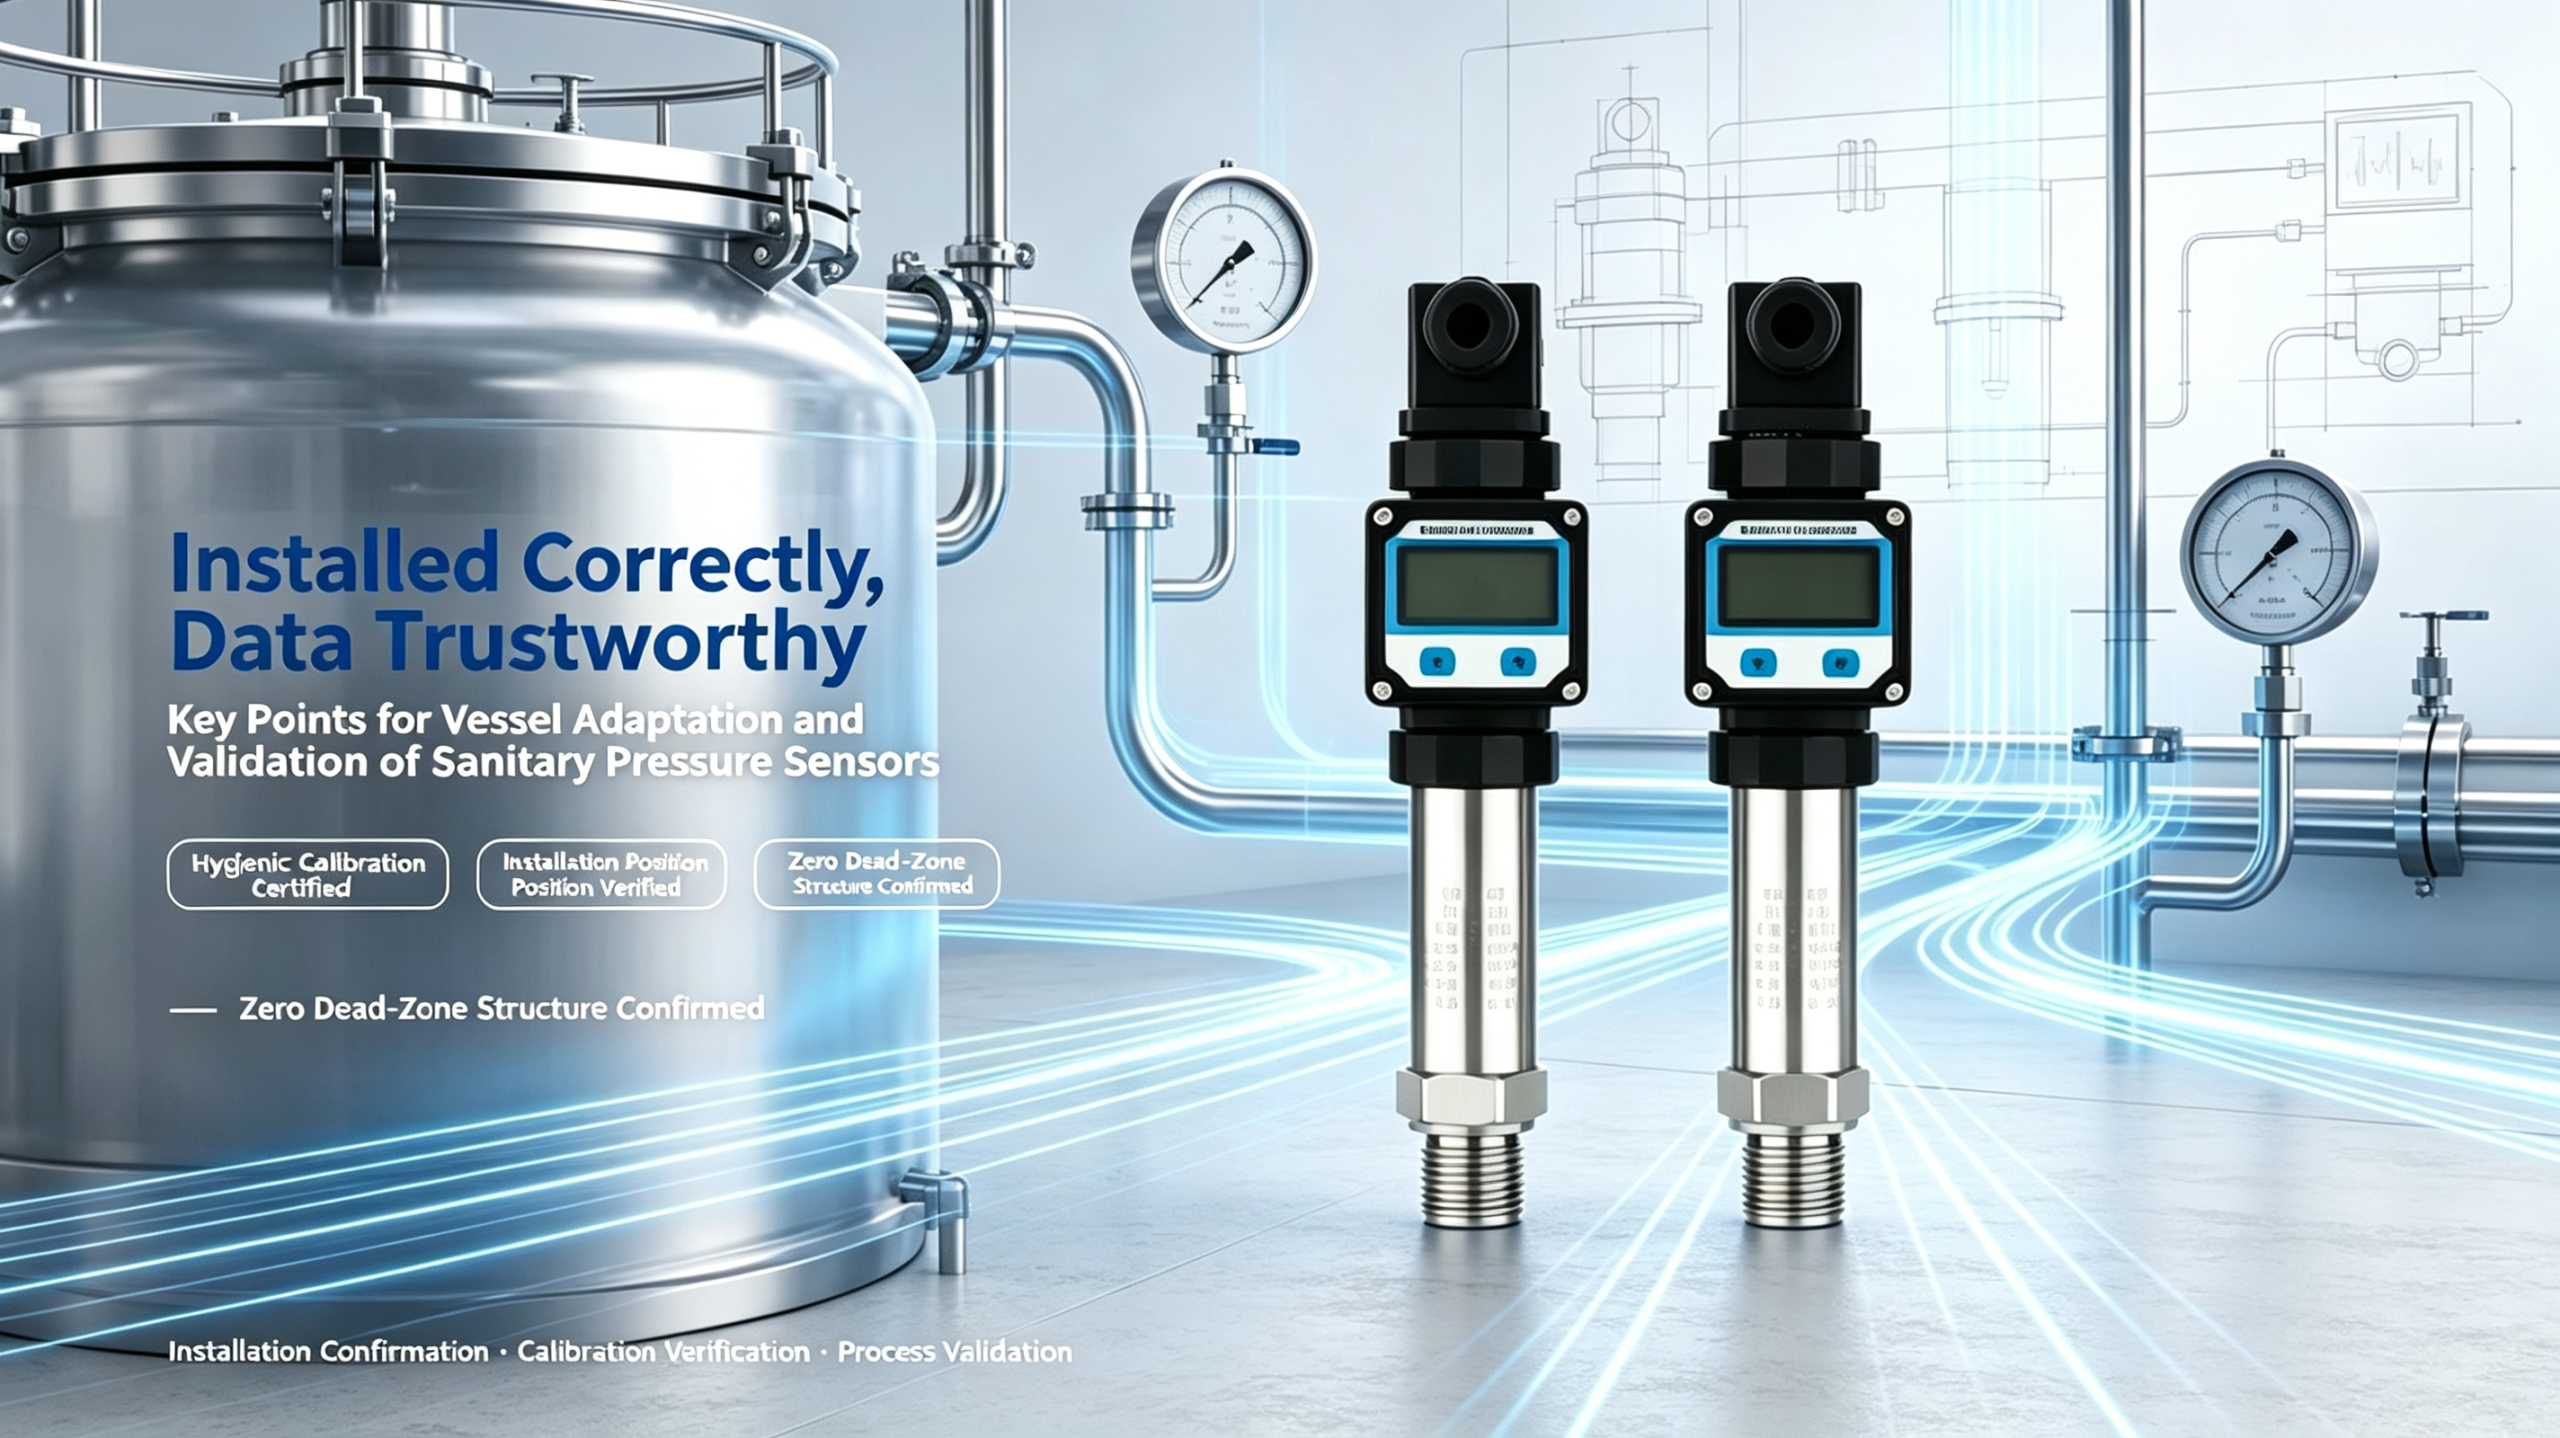
From strain cultivation and liquid preparation to pure water storage and high-temperature sterilization, the aseptic safety of all pharmaceutical process tanks relies on accurate monitoring and stable control of sanitary pressure sensors. Different from general industrial monitoring, pharmaceutical sensing technology prioritizes sanitation, supplemented by high precision, and based on full compliance.
With professional and reliable sensor technology, we guard every link of pharmaceutical aseptic production and build a solid safety line for high-quality drug manufacturing.
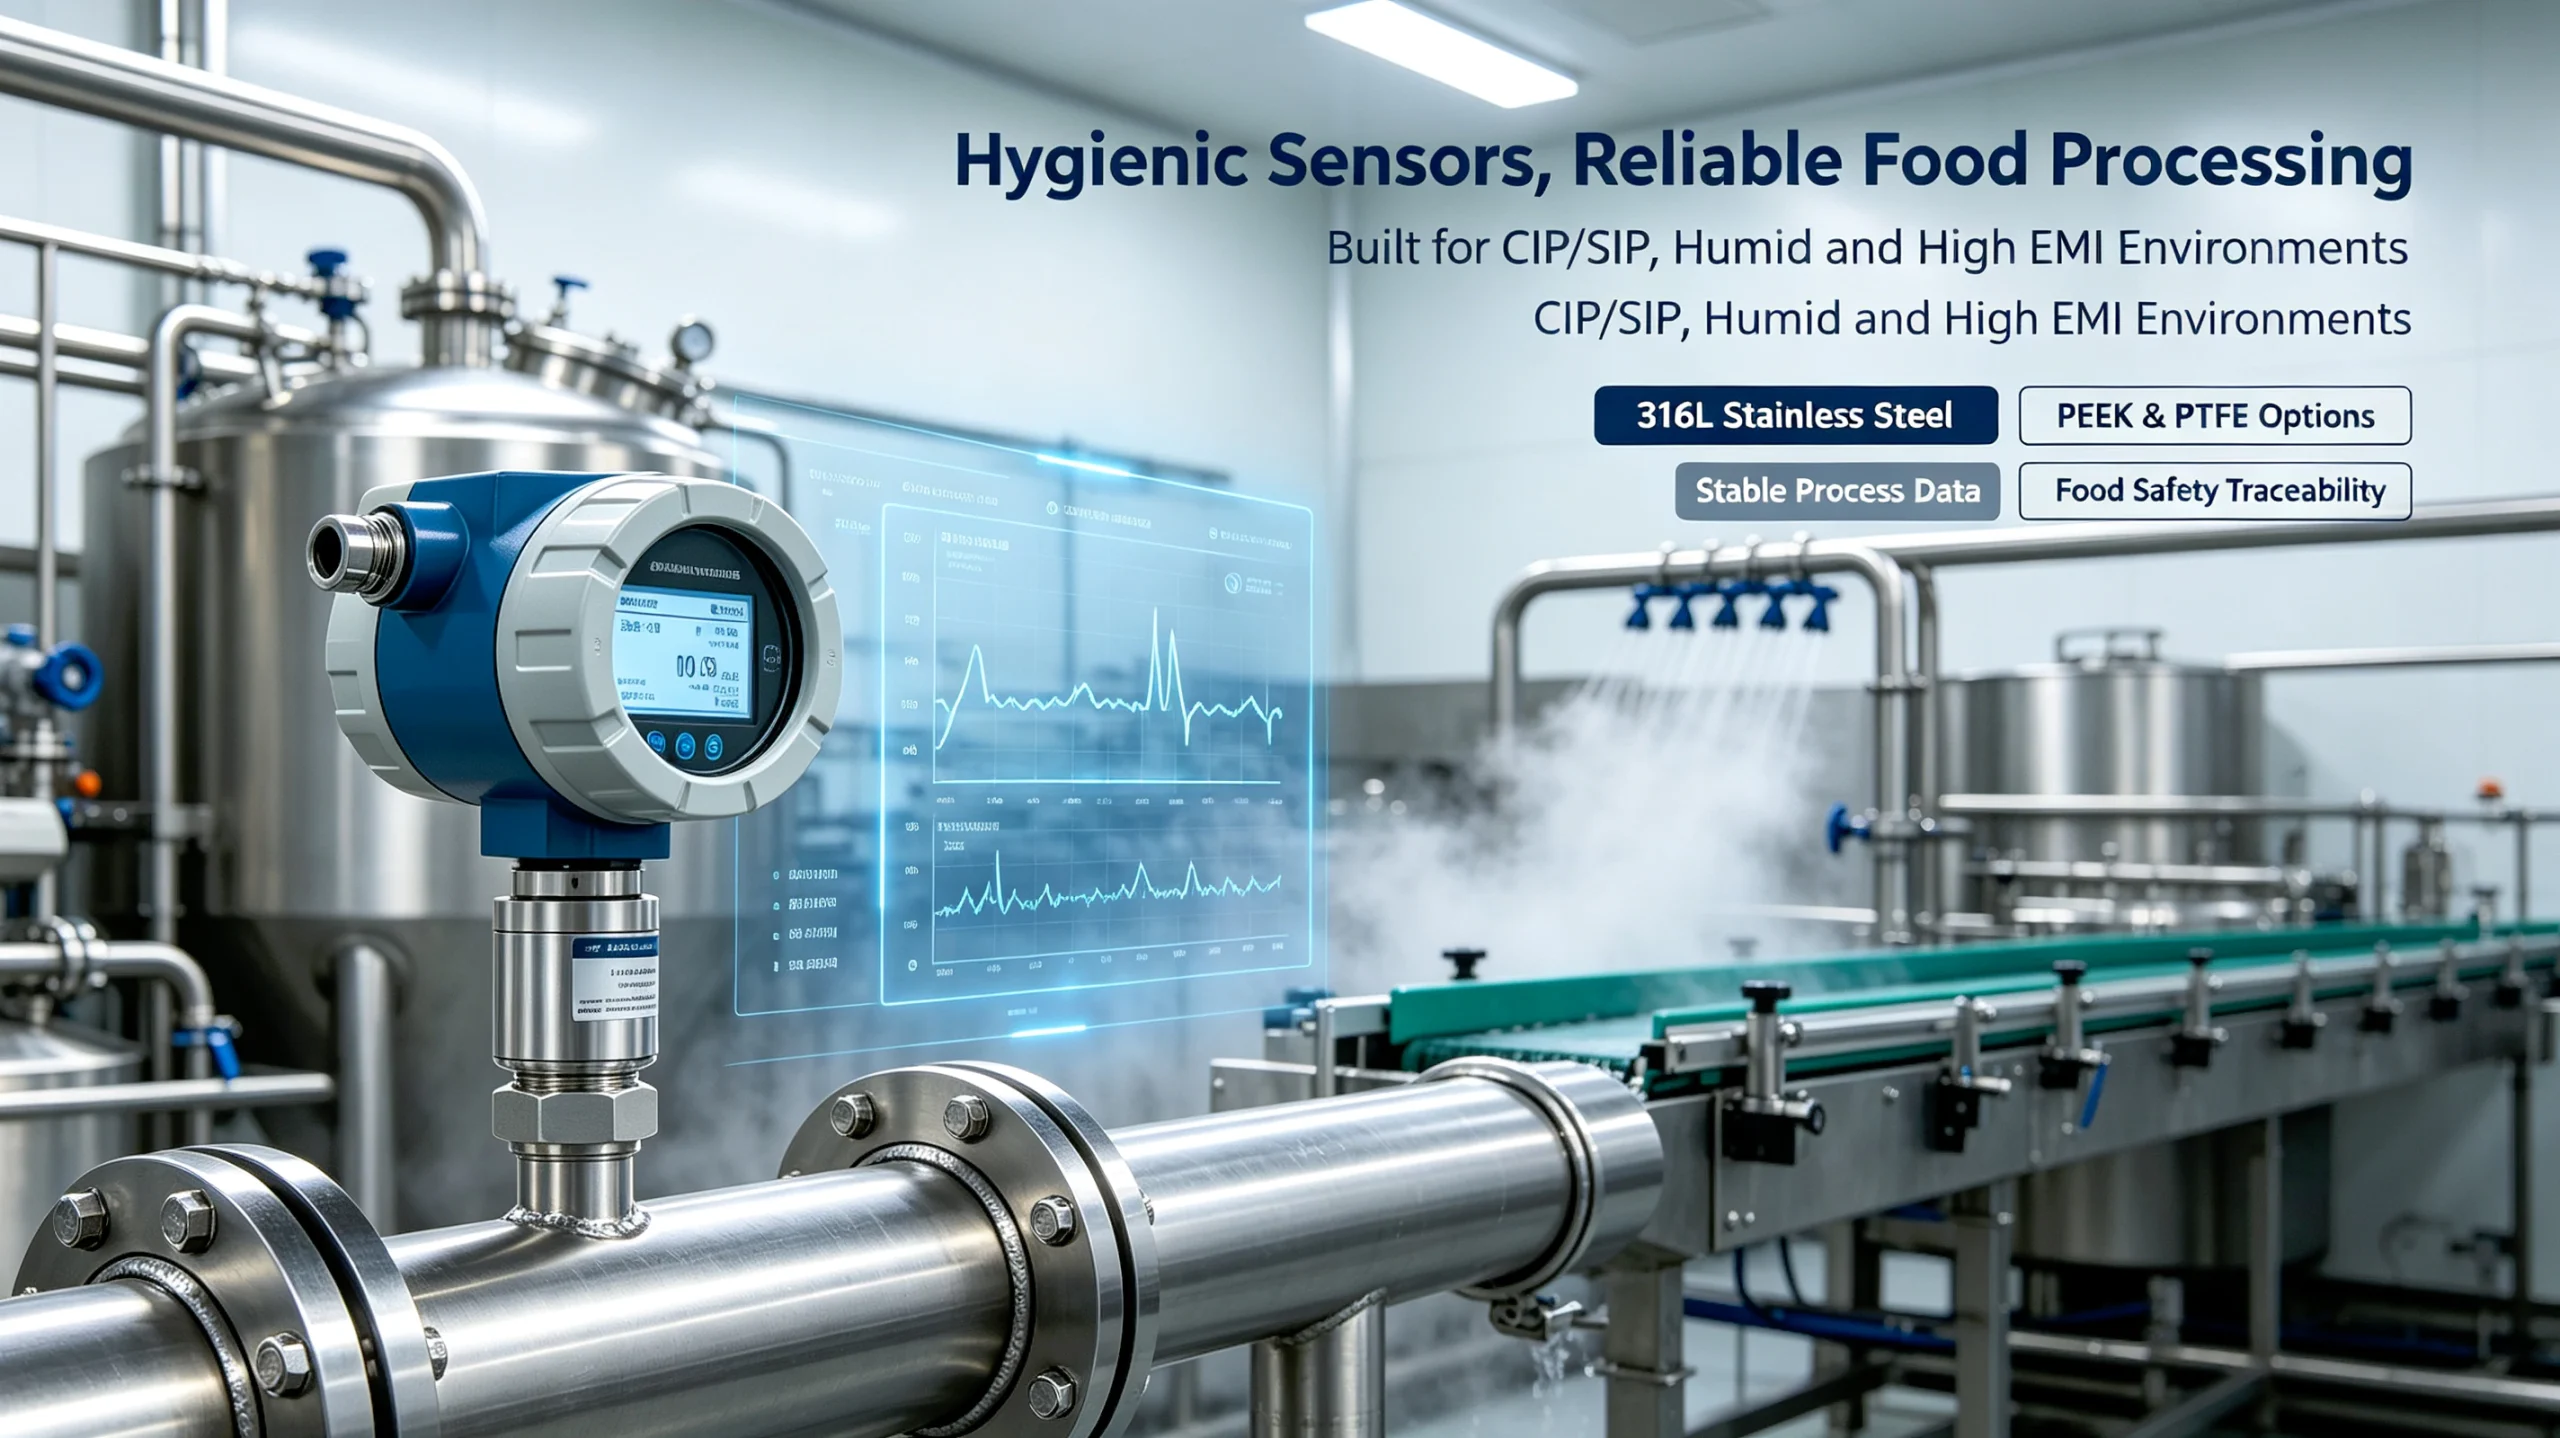
Guarding Food Production Lines: Reliable Sensing Is Key
Compliance Barriers Under Harsh Operating Conditions
Dual Tests of Hygiene and Performance
Mandatory Standards for Food Safety Protection
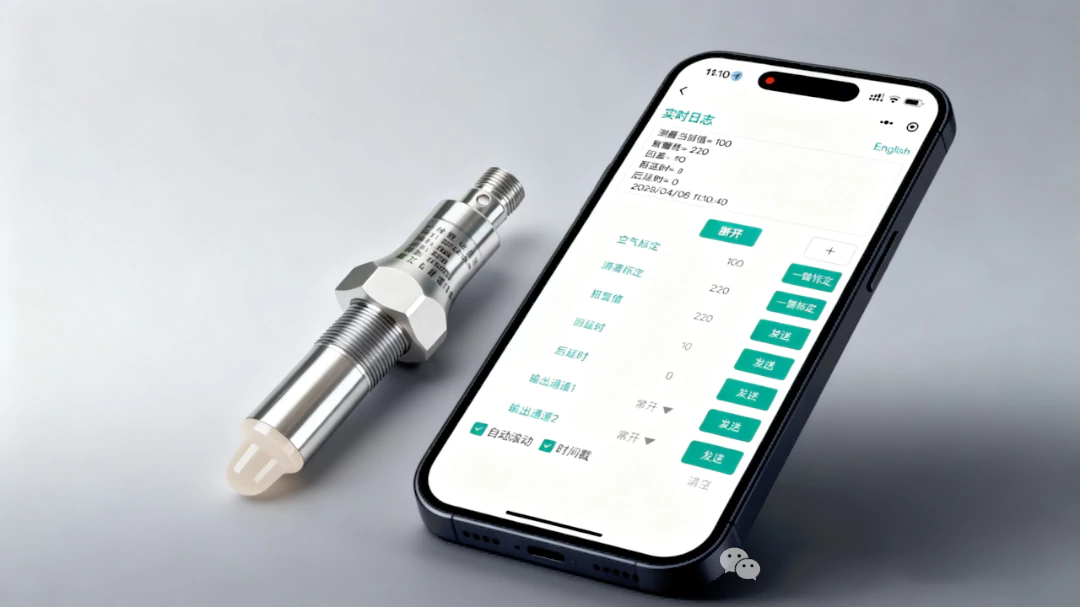
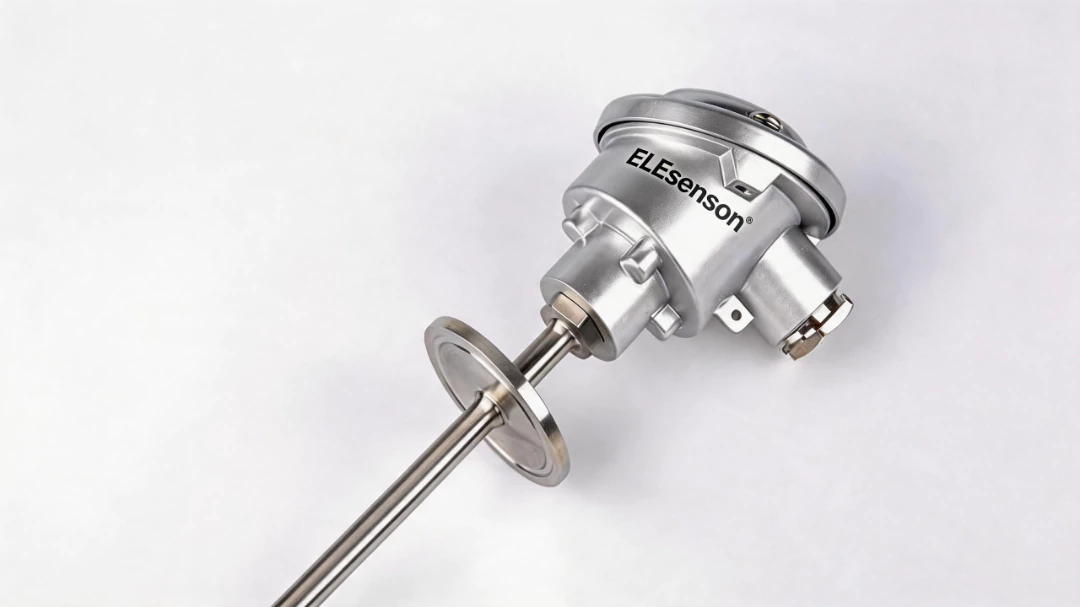
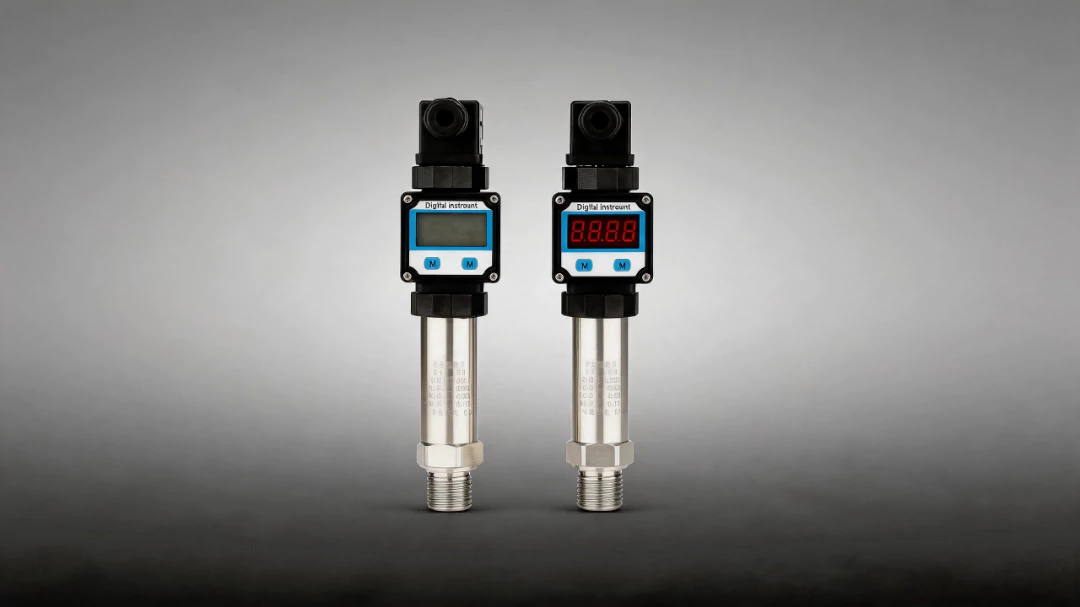
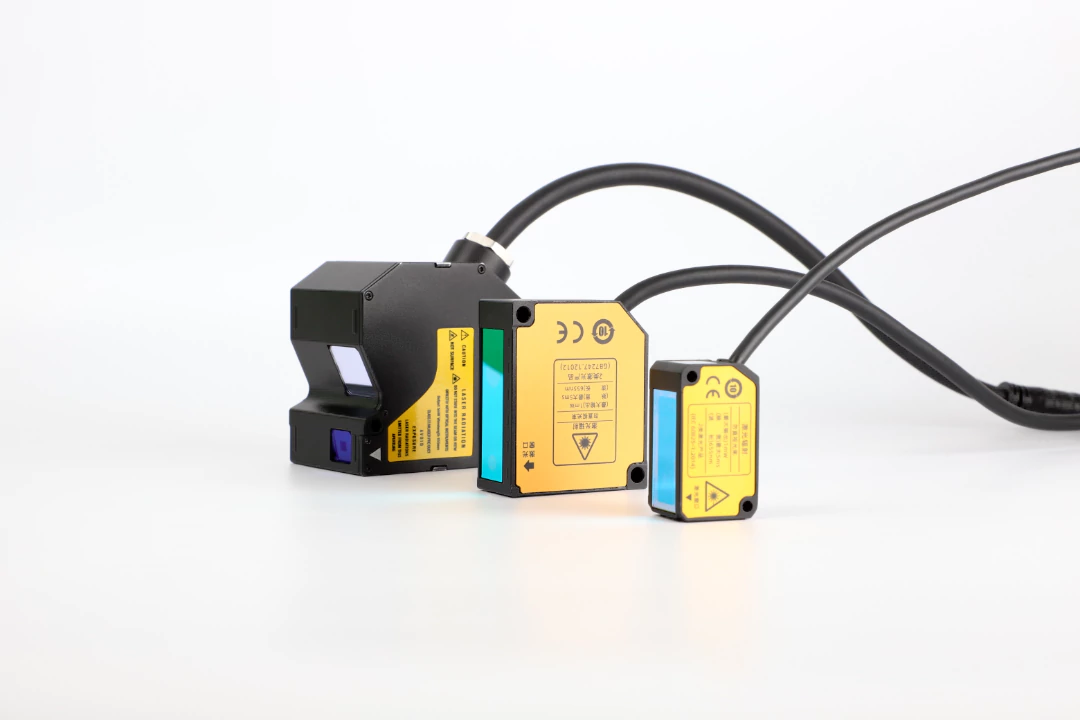
Balancing Hygiene Standards and Long-term Stable Operation
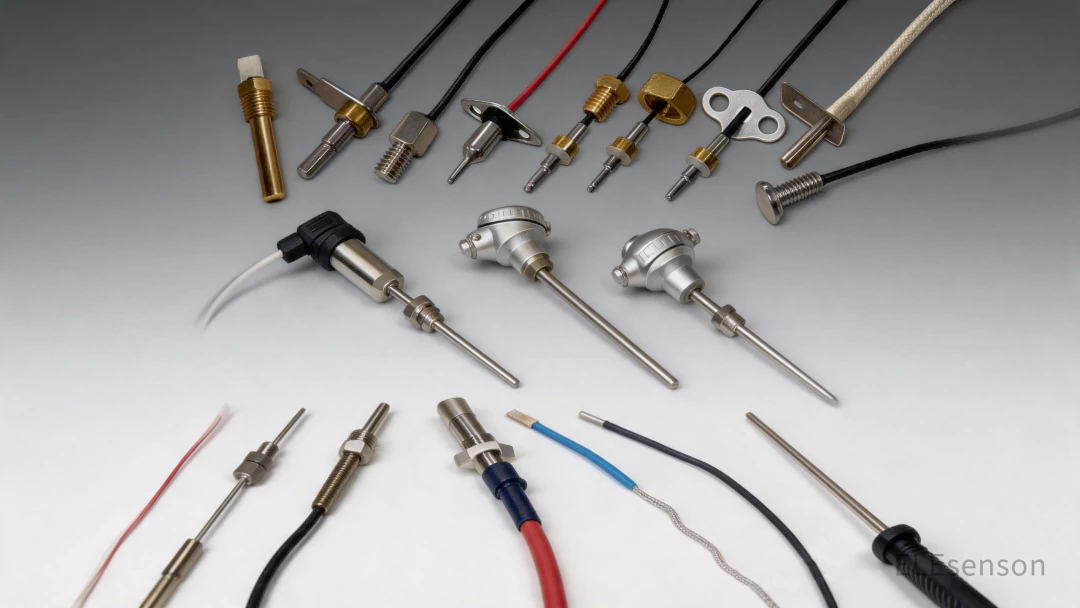
Railway Temperature Sensors: Safeguarding High‑Speed Train Operations
Railway temperature sensors are the quiet guardians behind every high-speed train journey. As high-speed trains travel across continents, reliable thermal monitoring stands at the heart of safe, stable rail operation.
High-speed trains run across vast territories, exposed to intense vibration, dramatic temperature swings and heavy electromagnetic interference. In these harsh on-board environments, railway temperature sensors act as the thermal nerve system of rolling stock, delivering continuous, precise temperature readings for critical train components. 🚄
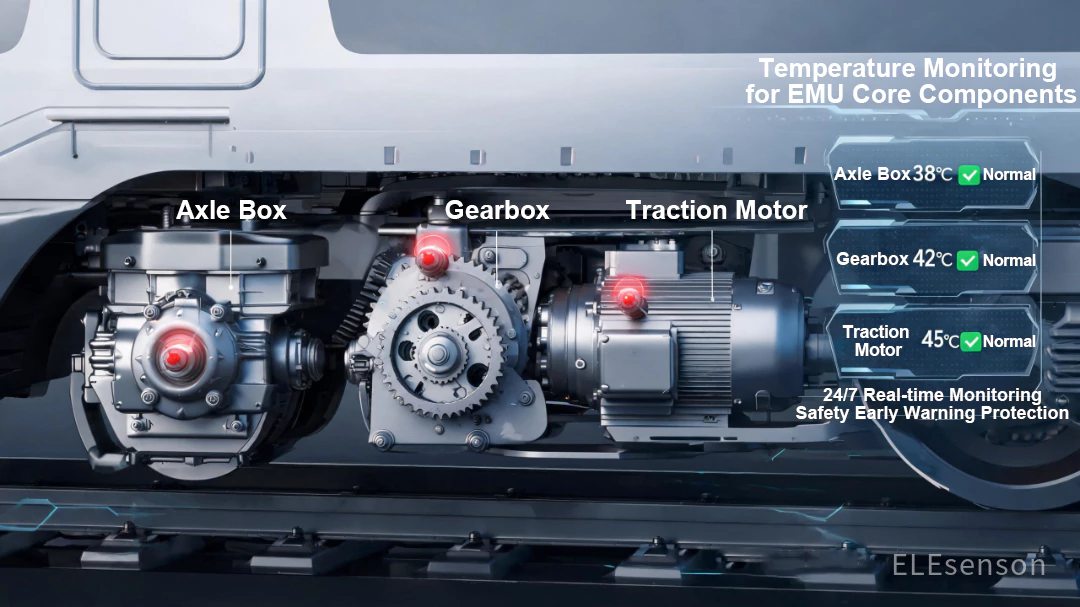
Axle boxes, gearboxes and traction motors are core rotating assemblies of high-speed trains. Sustained friction during high-speed operation can trigger unexpected temperature spikes, representing major safety risks. Our temperature sensors are mounted at key positions to collect 24/7 thermal data and capture minor temperature variations. Once overheating is detected, the system sends instant alerts and initiates speed reduction protection. This actively prevents hot axle box incidents and mechanical failures, securing the baseline safety of railway operation. This is where a high-quality railway temperature sensor proves its value.⚙️
Traction converters serve as the power core of high-speed trains and generate substantial heat under prolonged heavy loads. Excessive heat may cause power degradation, component breakdown or emergency shutdown. A dedicated railway temperature sensor monitors power modules and cooling ducts in real time. Working alongside cooling systems, they dynamically adjust thermal management parameters to avoid overheating and overload. This maintains stable, efficient performance of the traction system and delivers consistent power support for high-speed travel.
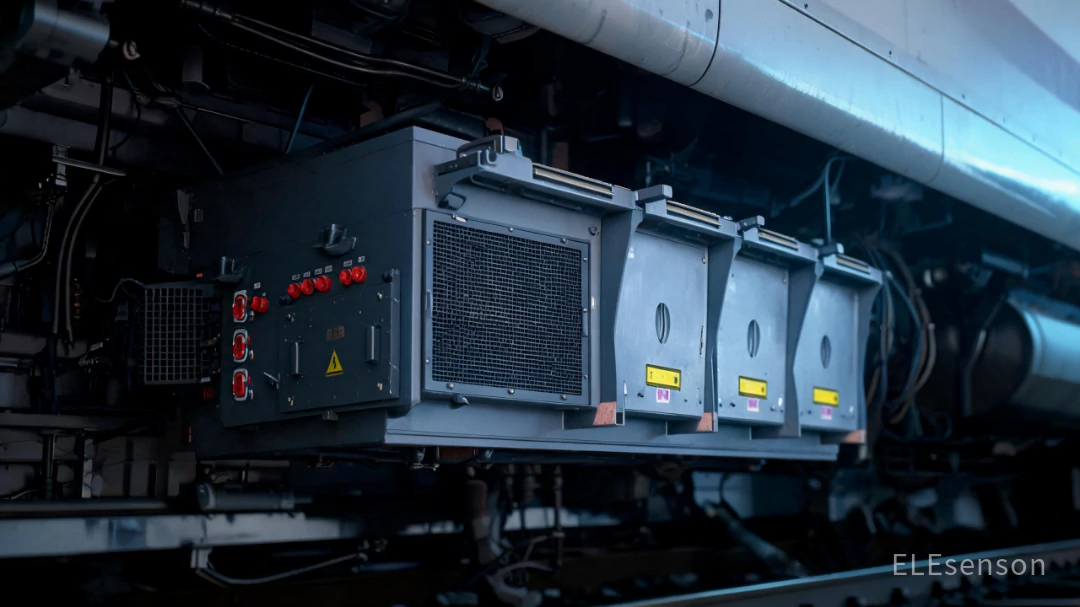
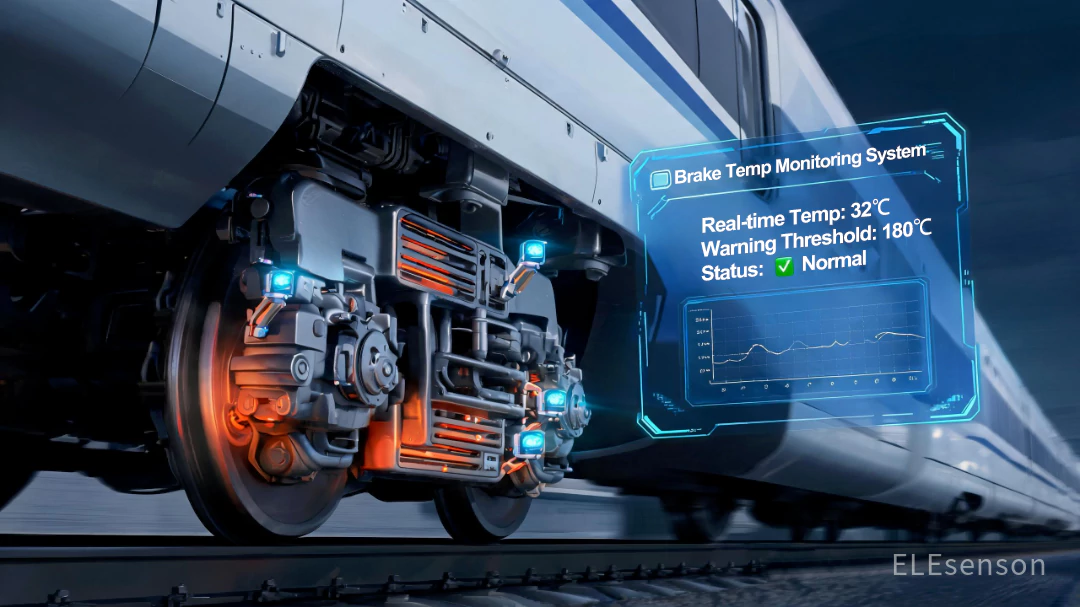
Repeated acceleration and braking lead to rapid heat accumulation on brake calipers and braking resistors. Rising temperatures can degrade brake performance or even cause brake failure. A rugged railway temperature sensor continuously tracks thermal conditions of braking components.. They flag high-temperature anomalies promptly, prevent thermal failure of braking systems and preserve reliable braking performance for every stop and start. 🛑
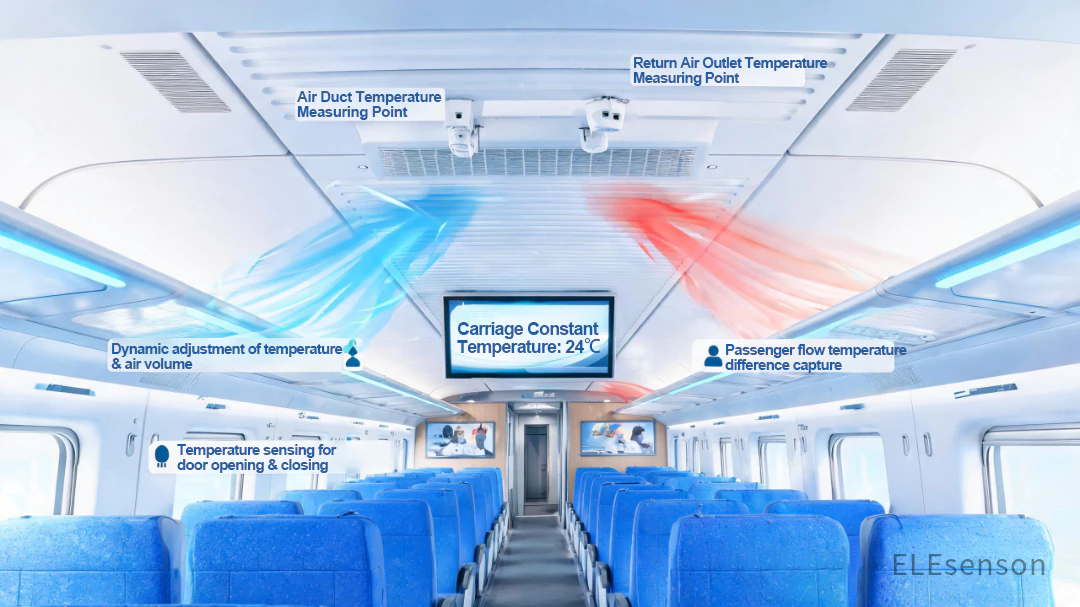
Beyond operational safety, temperature sensors also improve passenger comfort. Sensors fitted inside air ducts and return air grilles continuously measure cabin temperature. An in-cabin railway temperature sensor compensates for temperature fluctuations caused by door operation., varying passenger loads and day-night thermal differences. Paired with HVAC systems, they regulate heating, cooling and airflow automatically to maintain steady cabin temperature and enhance passenger riding experience. 💺
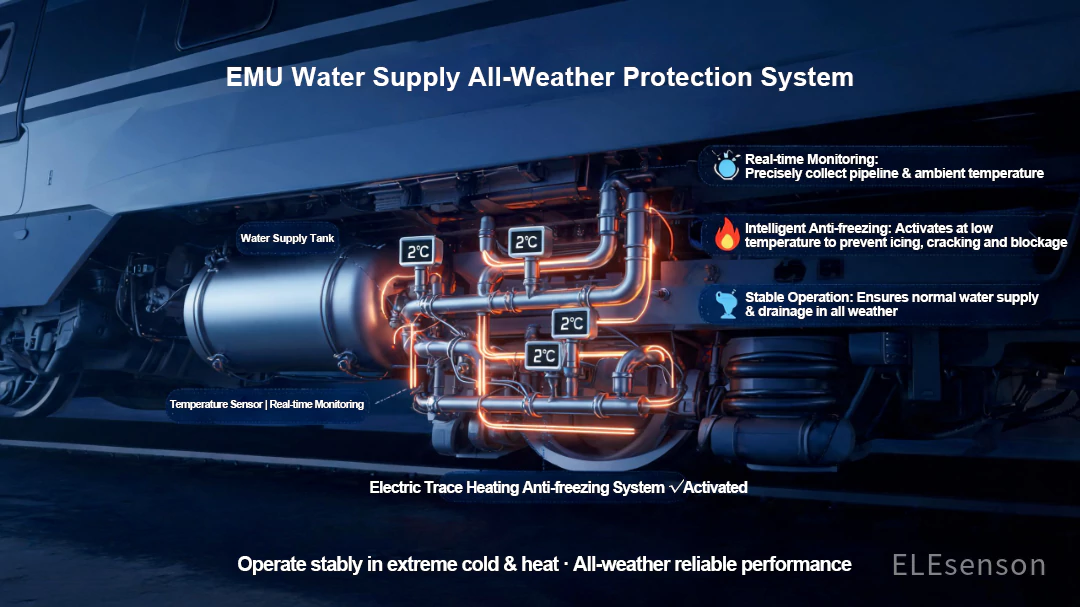
In extreme cold or hot climates, train water supply and drainage pipes face risks of freezing, cracking and blockage. A pipe-mounted railway temperature sensor monitors ambient and water temperatures.. When temperatures drop below thresholds, the system activates electric trace heating for anti-freeze protection. It protects pipework from frost damage and ensures water systems operate reliably all year round, enabling trains to run stably under all weather conditions. ❄️
Compact railway temperature sensors deliver critical functions across train safety, powertrain control, braking management, passenger comfort and pipeline anti-freeze protection. Built for rail transit’s demanding working conditions, they feature accurate thermal measurement, strong anti-interference capability and long-term stability. These railway temperature sensors quietly protect every train trip… ✨
High-Frequency Opening & Closing of High-Speed Train Doors: How Can Touch Switches Withstand Intense Working Conditions?
01.Working Condition Analysis
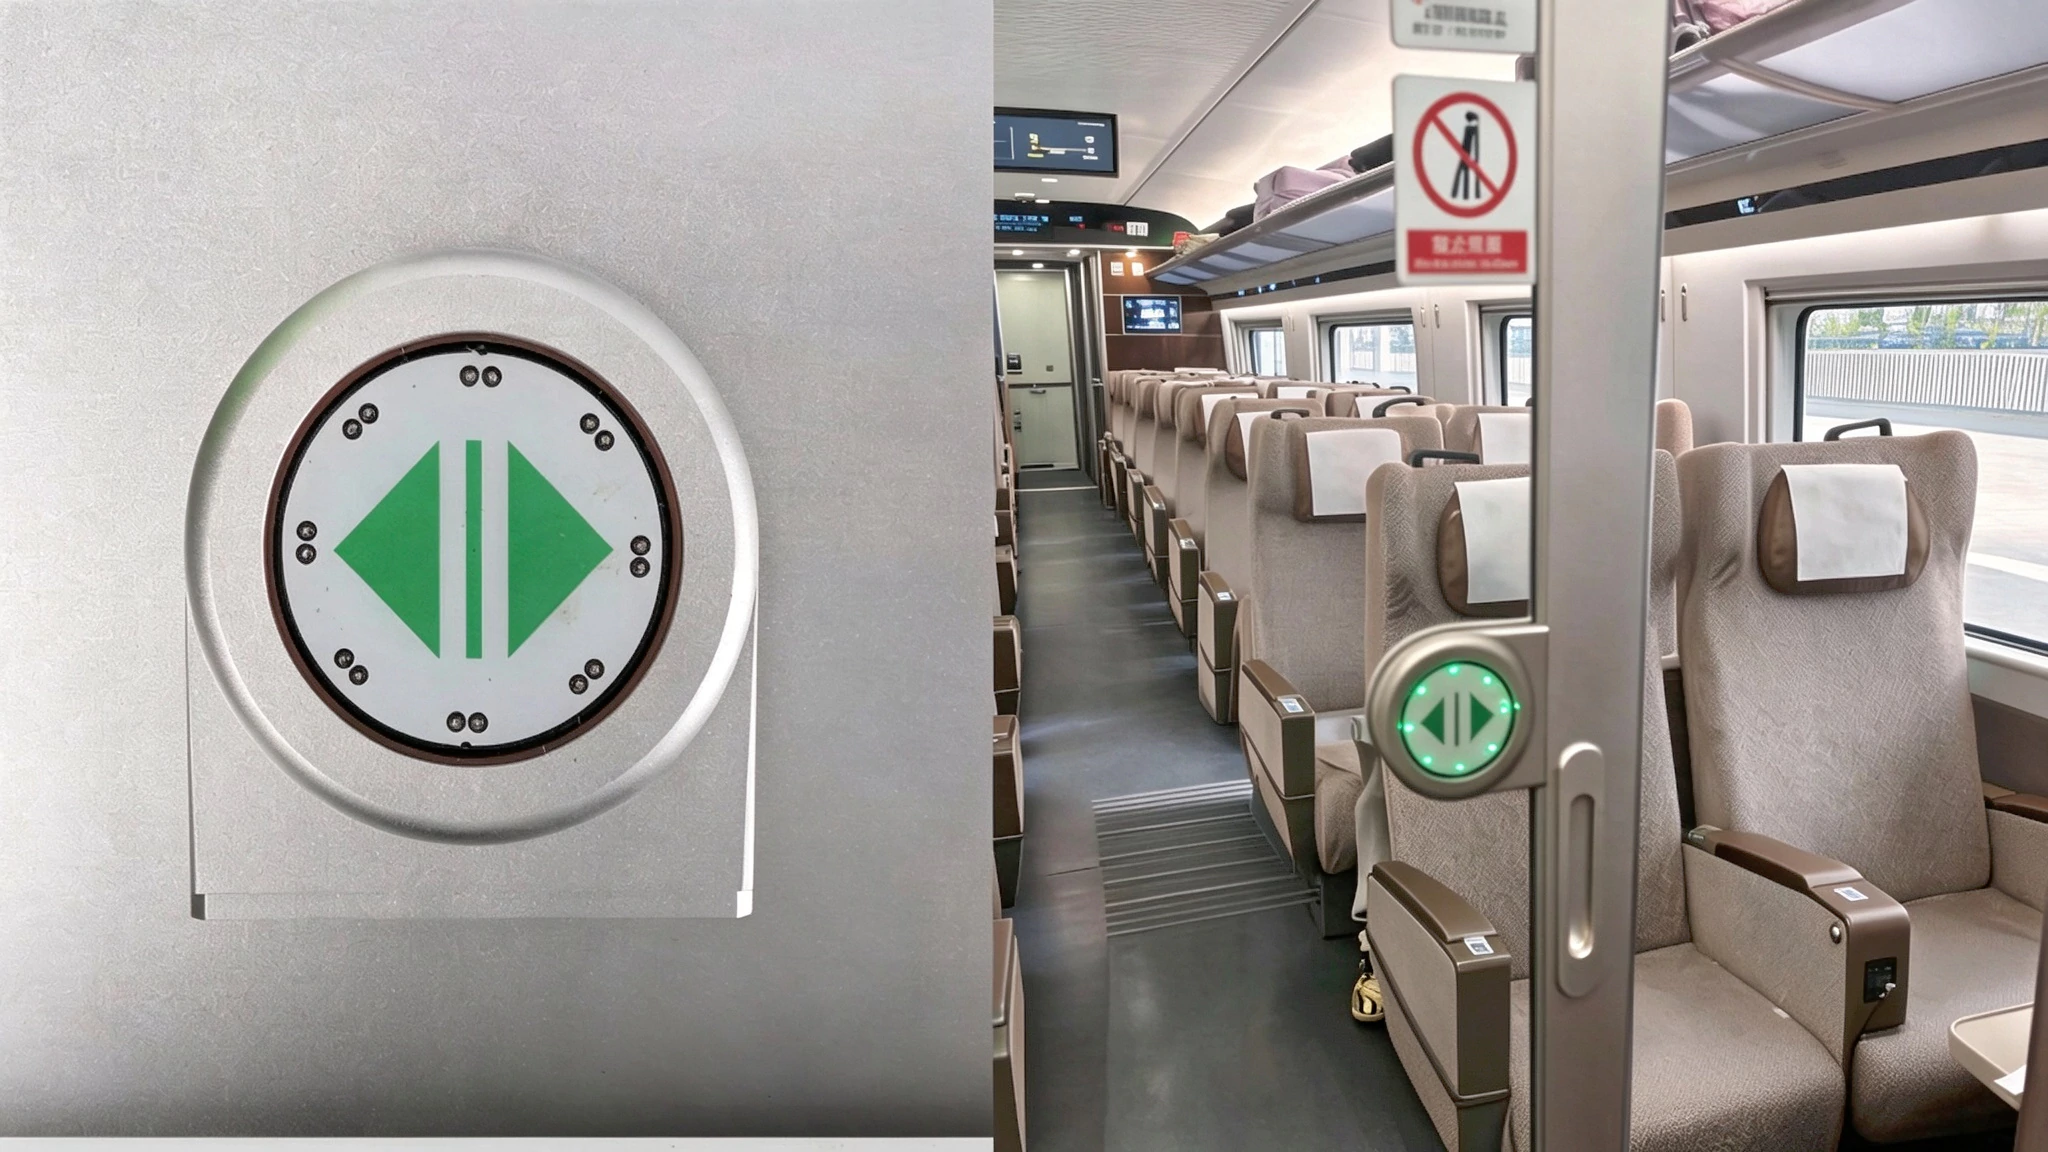
High-speed train doors perform repeated opening and closing cycles every day under complex operating environments. ELEsenson industrial touch switches are fully adapted to all working scenarios of rail vehicle doors, delivering dependable sensing support for safe and stable door operation.
High-speed EMU exterior door:
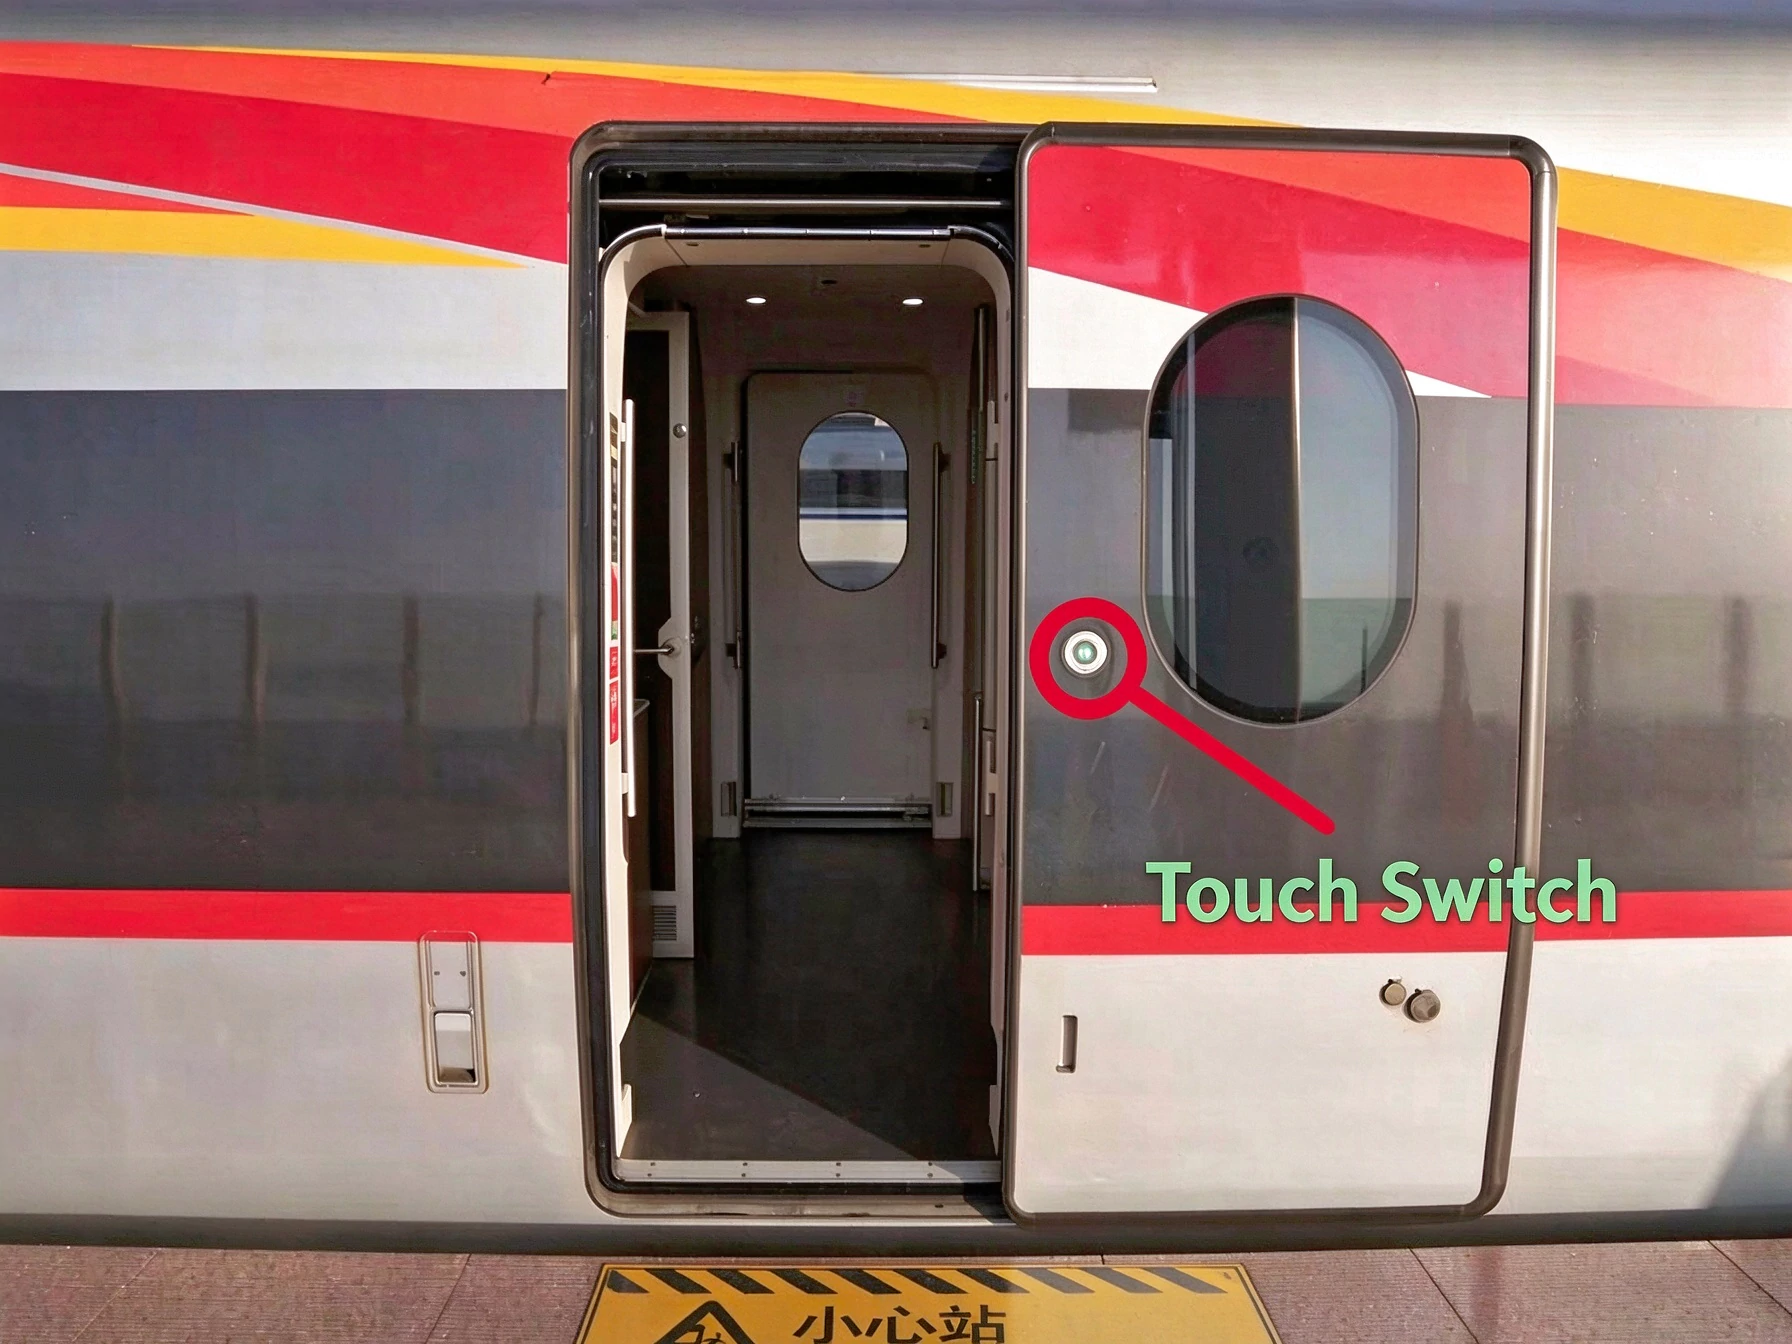
EMU exterior door
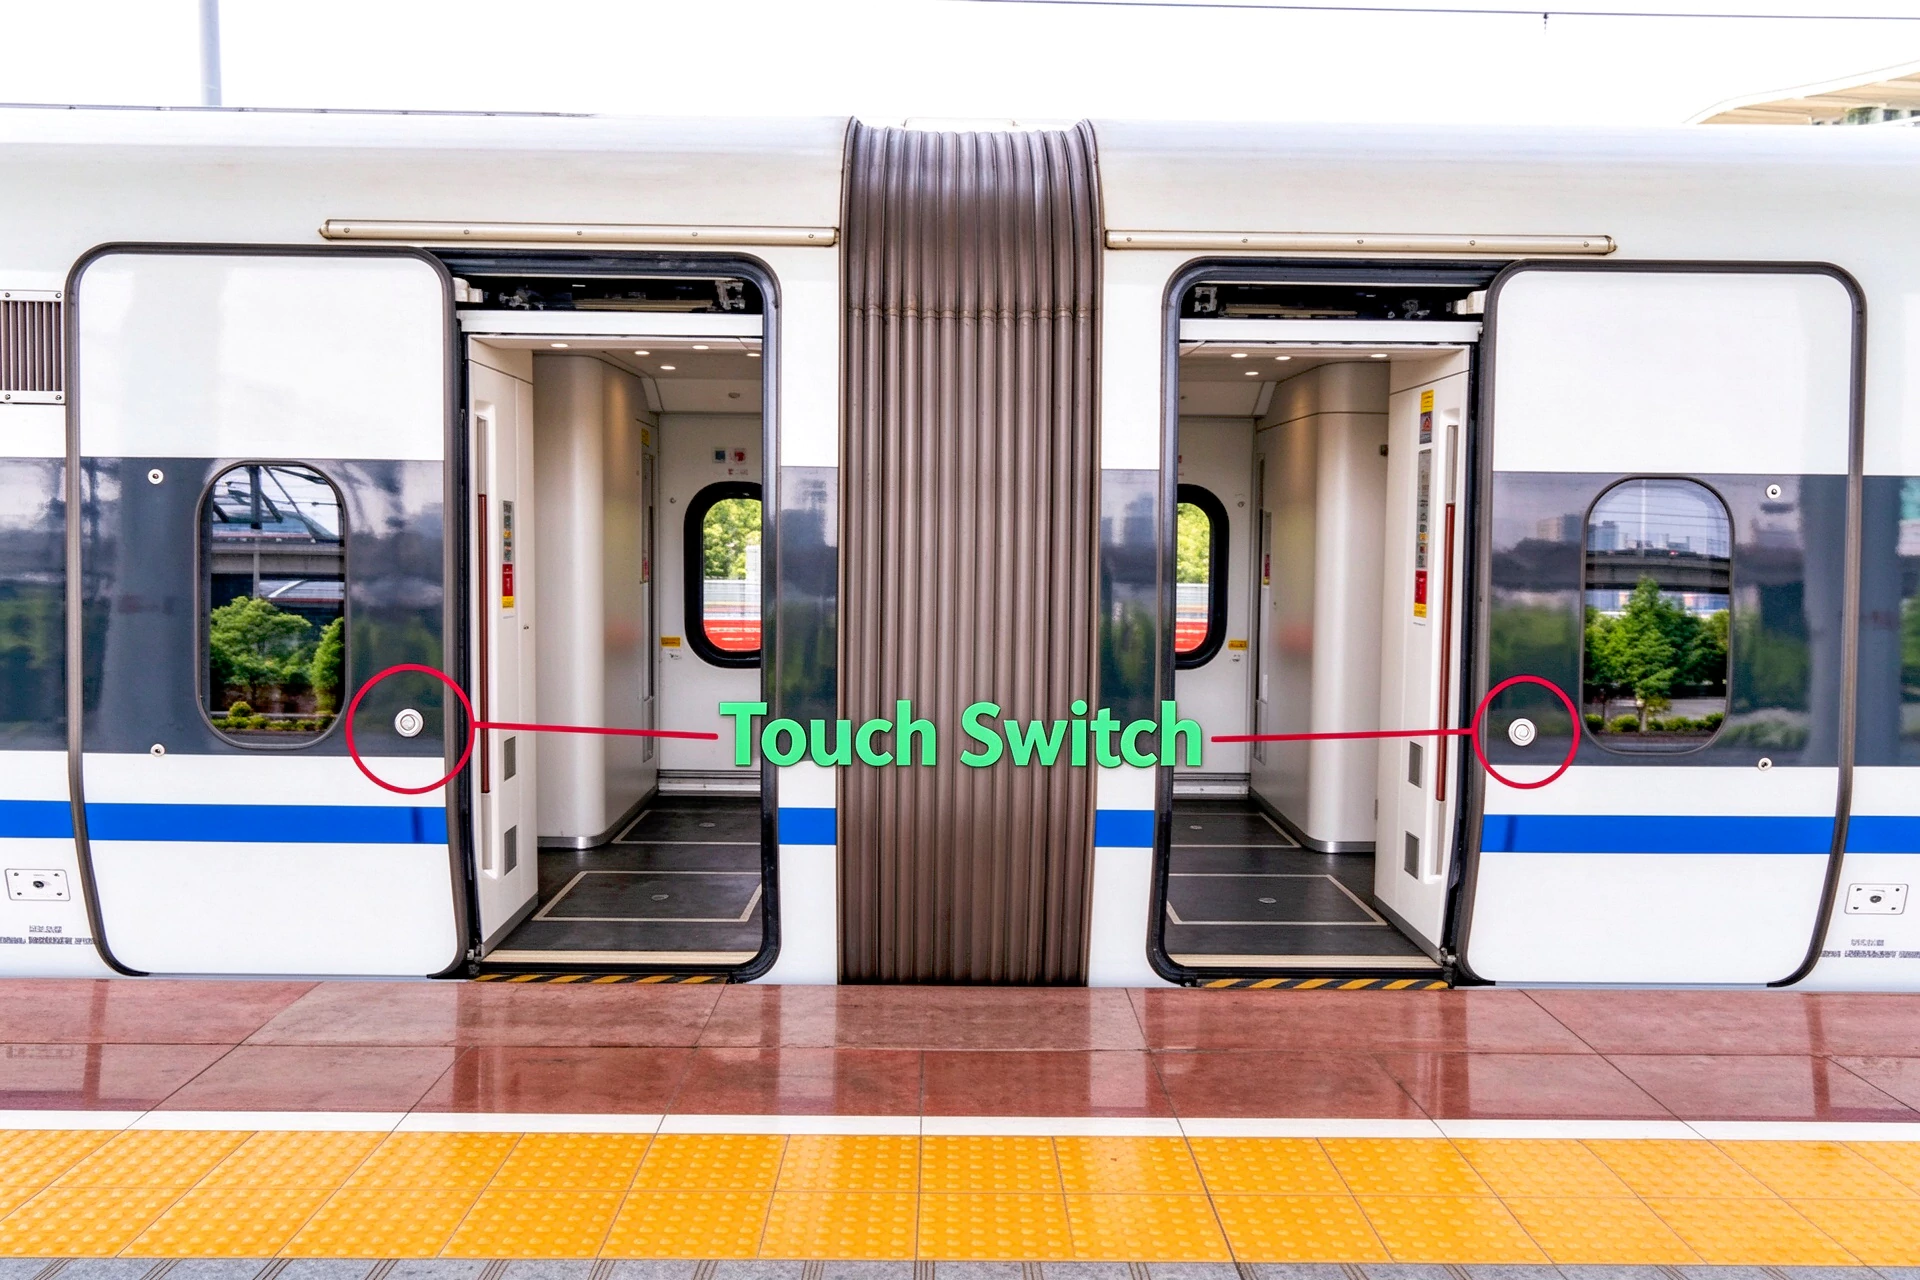
02.Technical Core
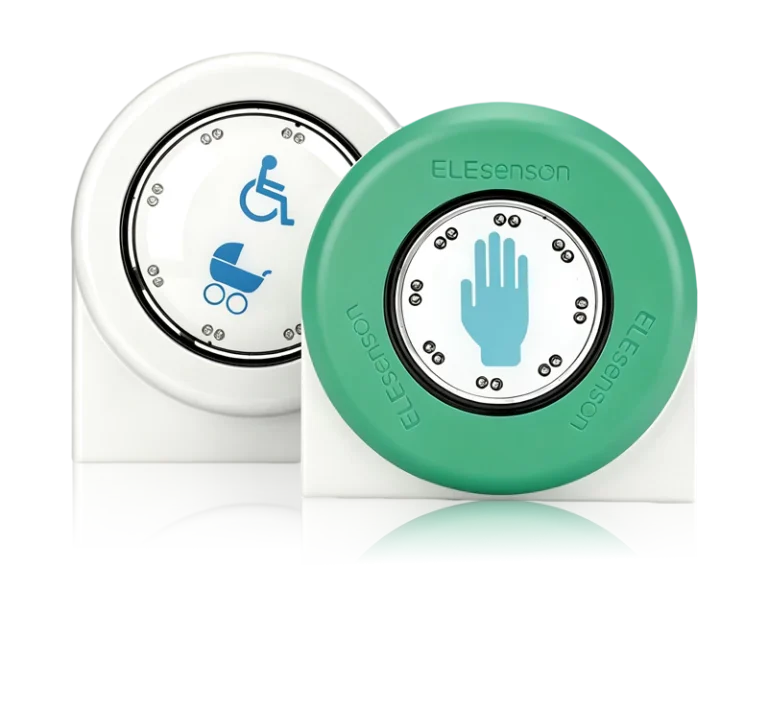
ELEsenson industrial-grade touch switches are customized for both interior and exterior door applications of high-speed trains. Adopting mechanical-contact-free intelligent touch technology, the switches are well suited to the harsh working conditions of rail transit and empower performance upgrades for train door control systems.
03.Exterior Application
Train exterior doors are exposed to the open air all year round, enduring wind, rain, sunlight, drastic temperature swings, strong vibration during travel and intense light interference, which set strict reliability requirements for components. Built with high-precision anti-interference touch chips, ELEsenson touch switches resist strong light, moisture, extreme cold and heat. Even with coated panels, they maintain accurate and fast response, preventing false triggering and missed touch failures.
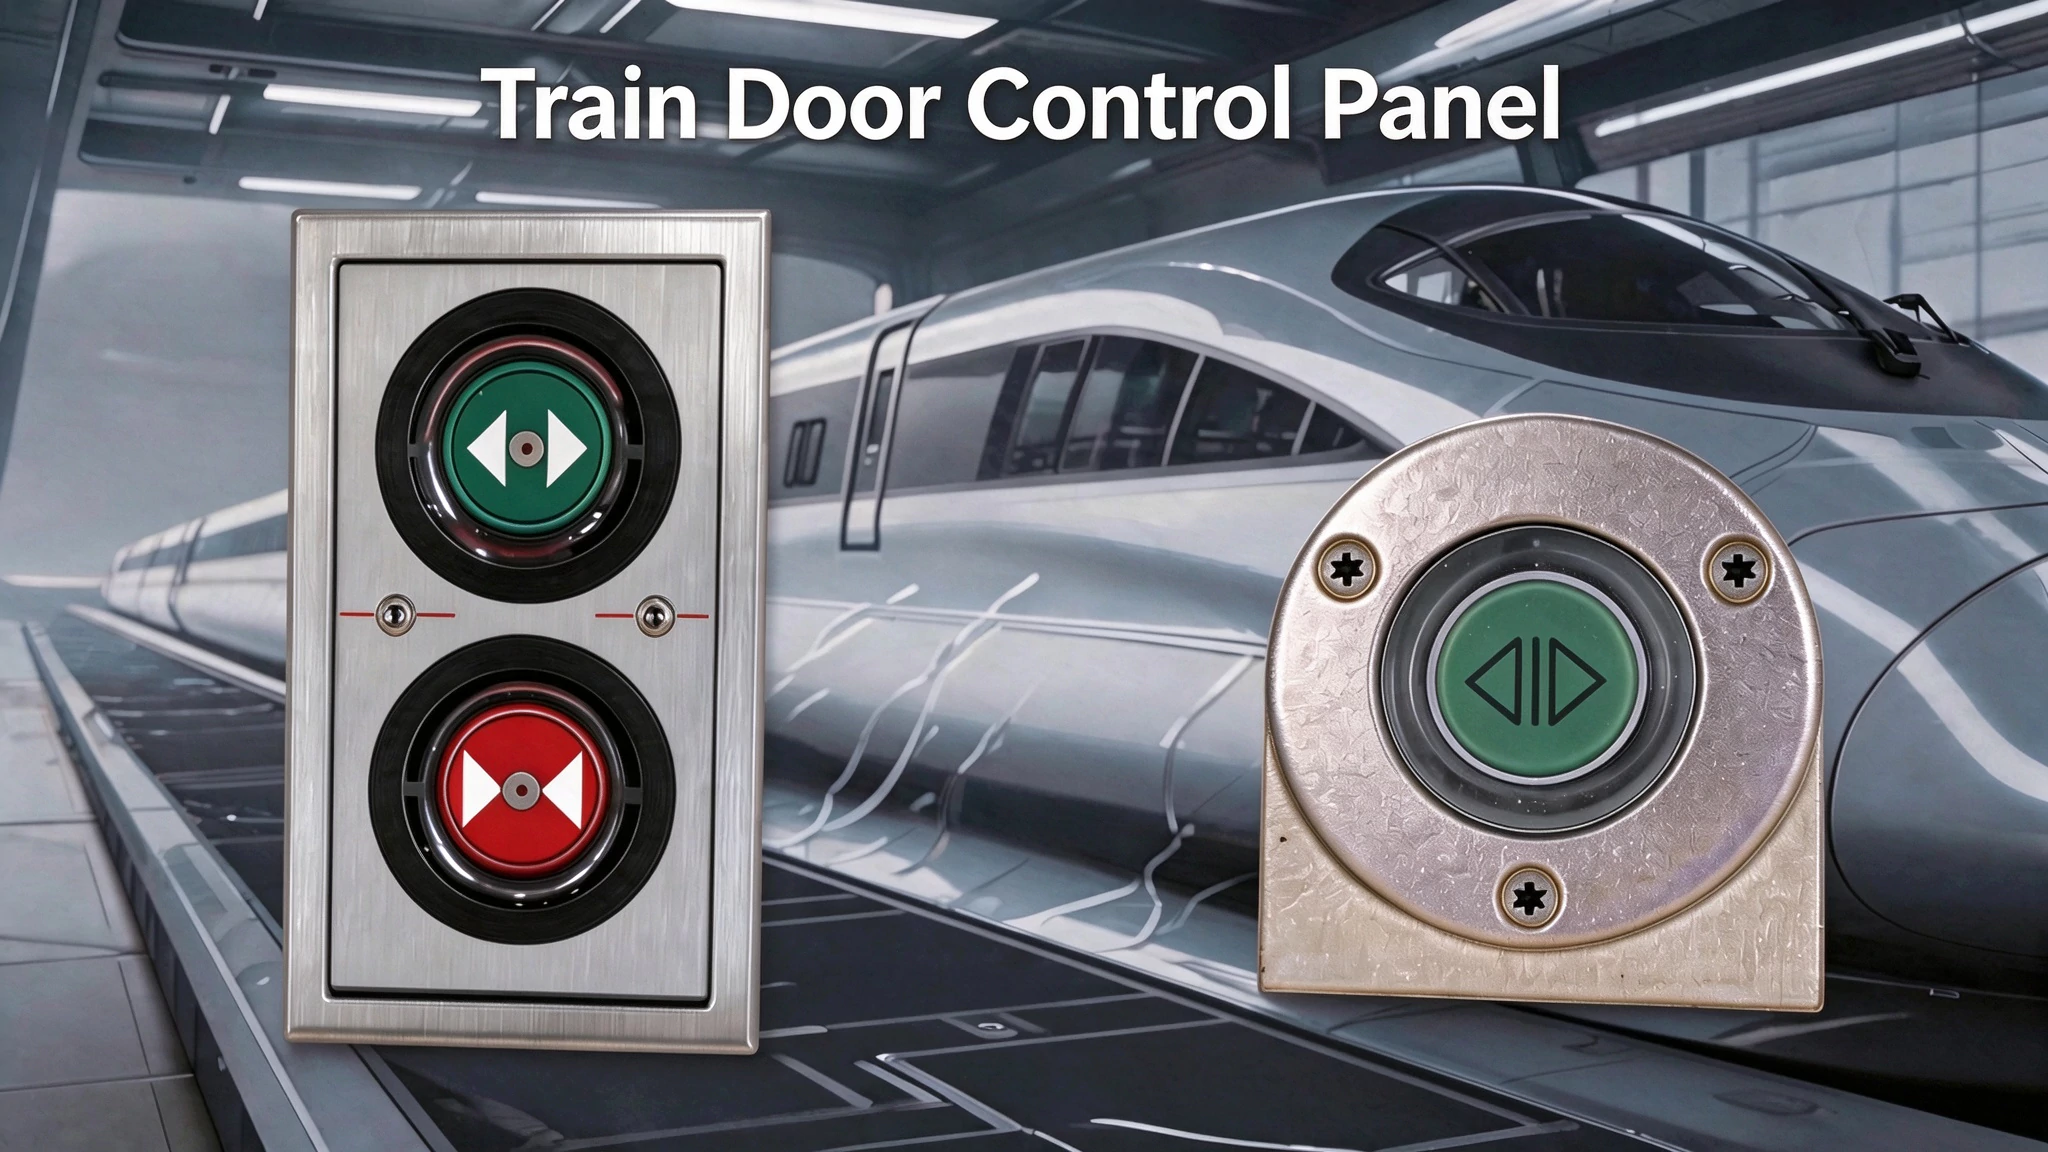
04.Interior Application
For carriage interior doors, quiet operation and simple control are prioritized. Removing traditional mechanical pressing structures, ELEsenson touch switches respond to a light fingertip tap. The whole operation runs silently without clattering noise, preserving a quiet and comfortable riding environment inside the carriage.
05.Conclusion
Featuring full-scenario compatibility, high stability, long service life and low maintenance cost, ELEsenson touch switches fully meet the requirements for high-speed train interior and exterior doors. With robust industrial quality, we safeguard rail transit operation safety and continuously improve passenger travel experience.
Laser Displacement Sensor | Non-Contact High-Precision Industrial Position Detection
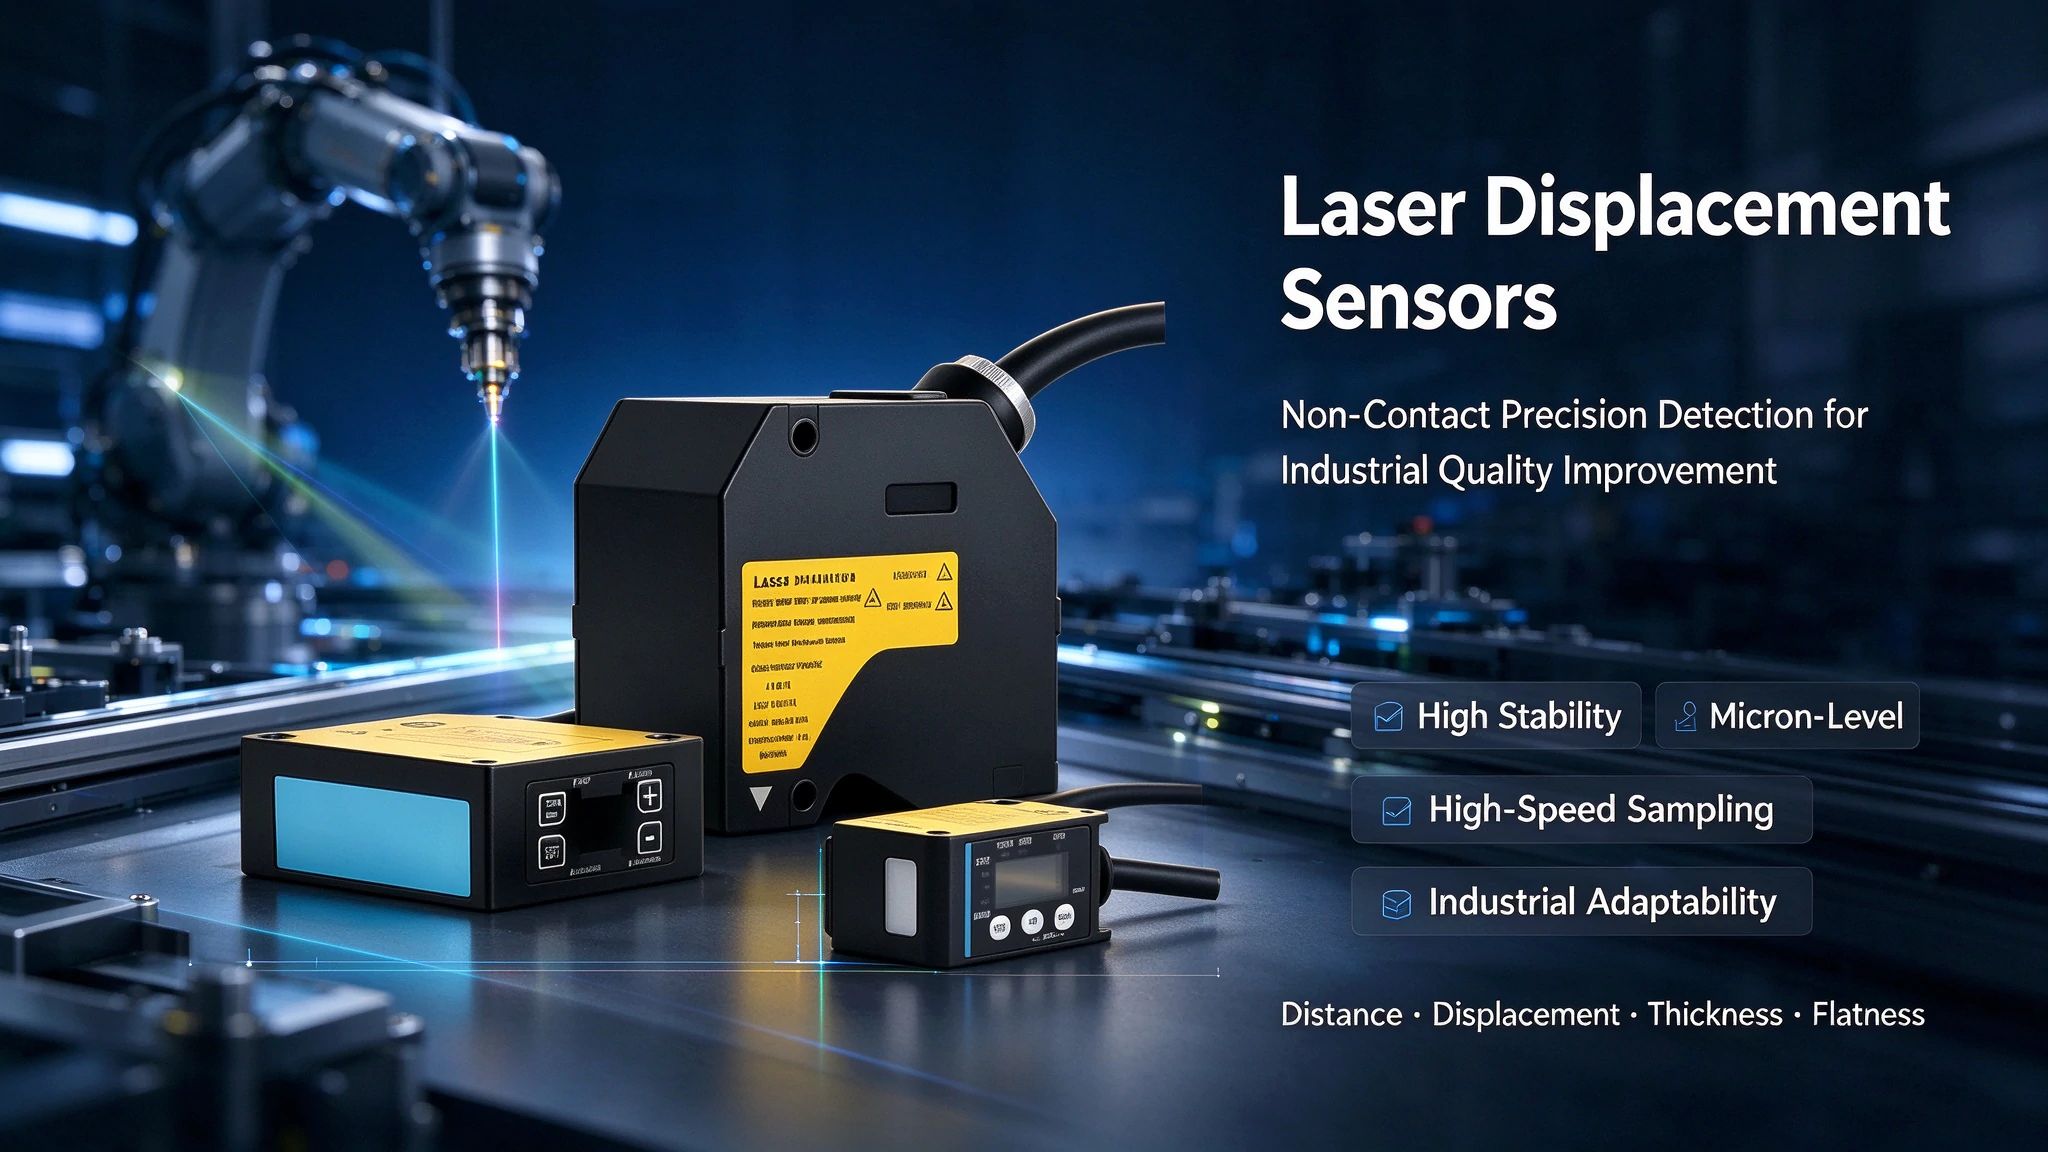
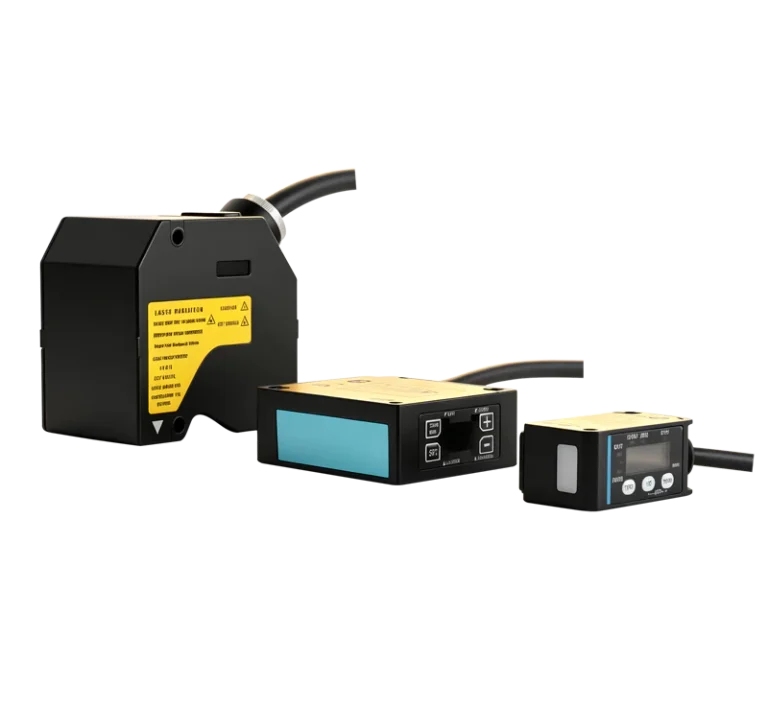
With the continuous upgrading of intelligent manufacturing, non‑contact precision detection has become an indispensable core link for production line quality improvement and efficiency optimization. ELEsenson laser displacement sensors adopt mature laser triangulation principle to realize high‑stability collection of distance, displacement, thickness, and flatness data. As high‑performance industrial perception hardware, the sensors deliver reliable and repeatable measurement data for automated equipment, widely covering precision inspection, dimensional monitoring, and closed‑loop control scenarios in modern industrial production.
Non‑Contact & Damage‑Free Measurement
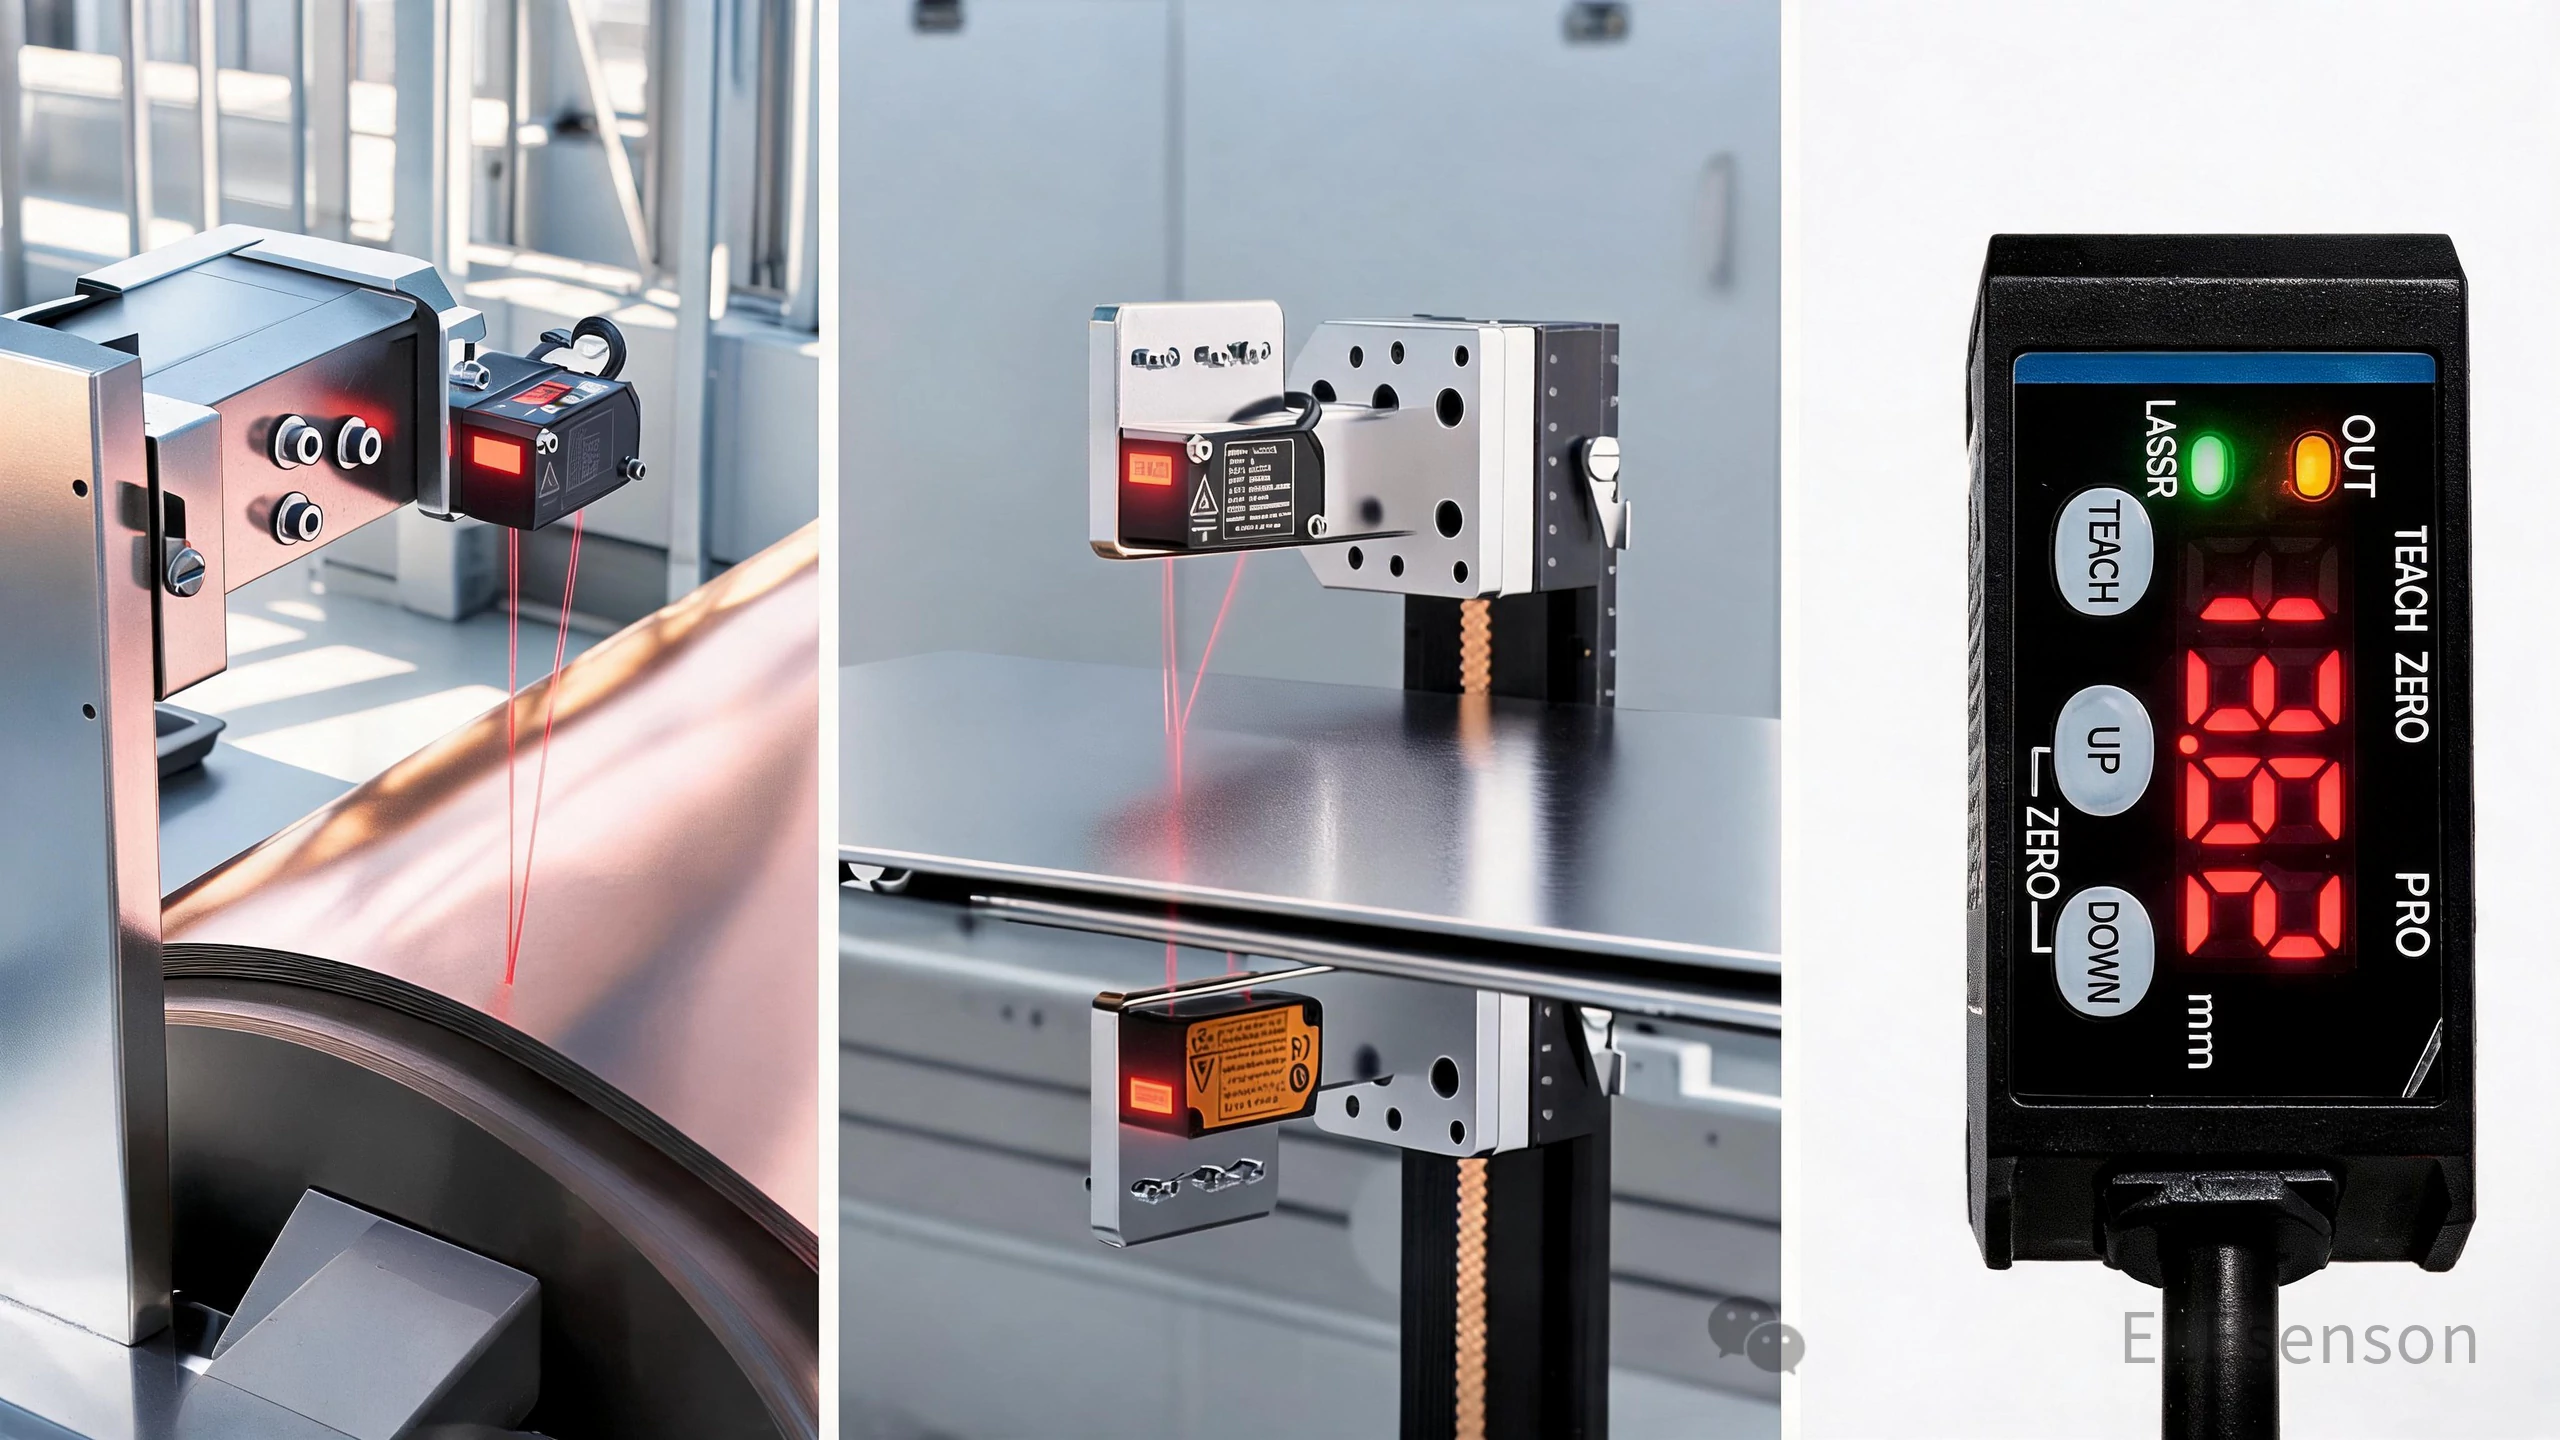
Adopting fully non‑contact laser detection mode, the sensor requires no physical contact with the workpiece surface. It completely avoids surface scratches, extrusion deformation, and contact detection errors. It is highly compatible with precision parts, flexible materials, and high‑gloss surfaces, supporting high‑speed dynamic online measurement with zero damage to workpieces.
High‑Precision & High‑Speed Dynamic Performance
Featuring stable micron‑level measurement accuracy, the sensor accurately captures tiny changes in height difference, thickness, flatness, deformation, and gaps. With ultra‑fast sampling response speed, it perfectly adapts to high‑frequency and high‑speed continuous operation of automated production lines, maintaining stable and consistent data output even in dynamic motion scenarios.
Strong Industrial Environmental Adaptability
Equipped with advanced anti‑ambient‑light interference algorithms, the sensor effectively resists complex light changes in workshop environments. The compact industrial‑grade structure tolerates industrial dust and slight oil pollution, ensuring long‑term stable operation. Supporting multiple standard signal outputs, it features simple installation and flexible debugging, enabling fast integration with various standard and non‑standard automated equipment.
Automated & Custom Non‑Standard Equipment
Widely used for workpiece positioning, height difference detection, and gap measurement on automated production lines. It assists robotic arms in precise picking and assembly, monitors real‑time fixture deformation, and provides accurate data support for equipment closed‑loop control, effectively improving assembly accuracy and production consistency.
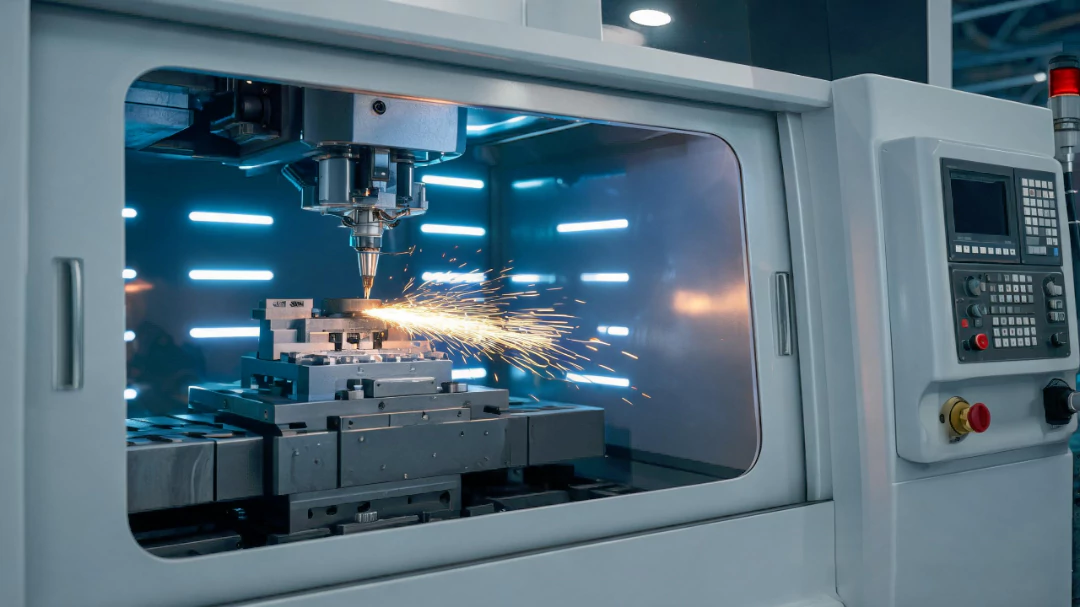
3C & Precision Component Manufacturing
Ideal for online quality inspection of electronic components, plastic parts, and hardware micro‑parts. It precisely detects product thickness, flatness, warpage deformation, and surface defects. It also monitors thickness fluctuation of flexible materials such as films and thin sheets, ensuring strict quality control for high‑precision miniature products.
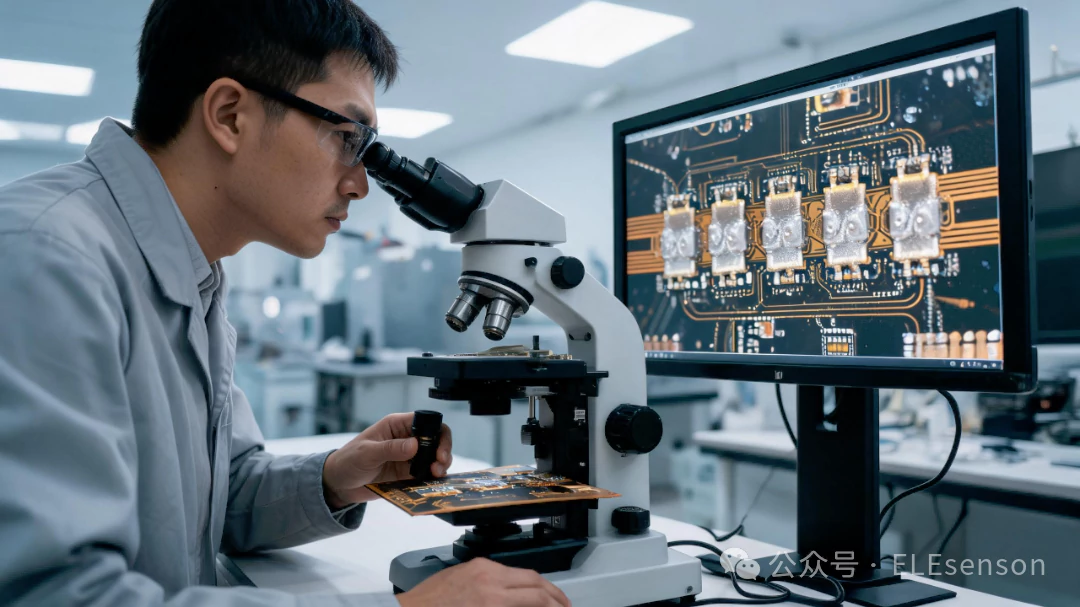
Automotive Parts Industry
Applied for dimensional verification, flatness detection, and assembly gap calibration of automotive components. It dynamically monitors machining deformation and operational vibration displacement, providing reliable data support for product quality inspection, process optimization, and equipment operational condition monitoring in automotive manufacturing.
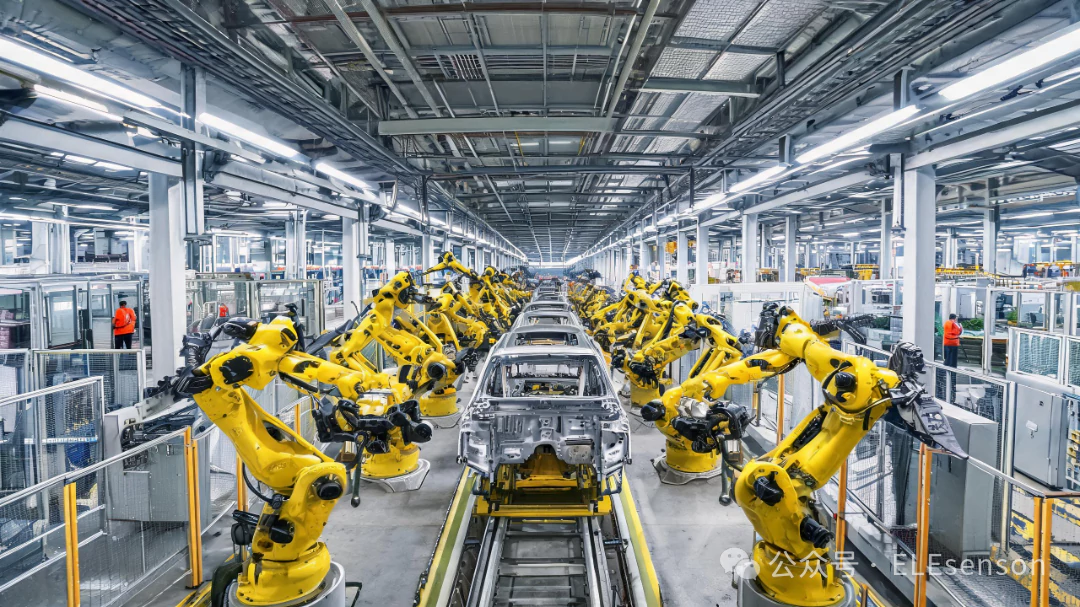
Metal Processing Industry
Suitable for thickness, flatness, and contour height detection of metal plates and profiles. It captures real‑time workpiece displacement changes during stamping, cutting, grinding, and other processing procedures, helping enterprises optimize processing parameters, improve machining accuracy, and increase finished product yield.
Logistics & Warehouse Automation
Easily integrated into intelligent warehousing and sorting equipment to realize cargo height detection, goods position positioning, and stacking state identification. It provides accurate spatial perception data for automated sorting and storage systems, ensuring efficient and stable operation of smart logistics scenarios.
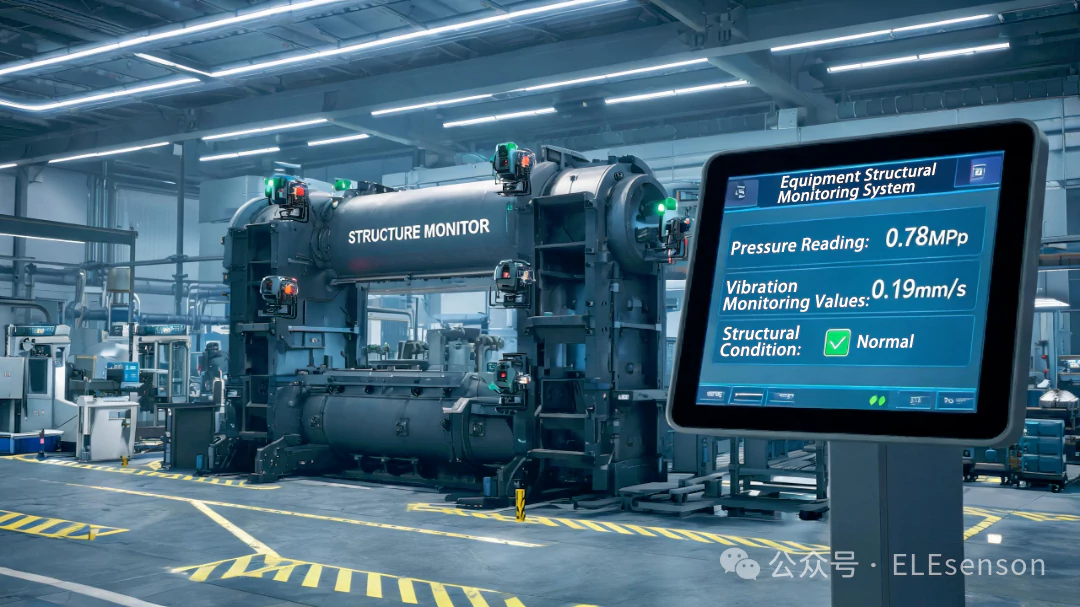
Structural Monitoring & New Material Testing
Capable of long‑term online monitoring of industrial equipment structural deformation and vibration amplitude, assisting equipment predictive maintenance and hidden danger troubleshooting. It also applies to deformation testing and performance analysis of new materials in laboratories, providing precise and repeatable measurement data for material research and process improvement.
No manual measurement required — precise laser perception covers all detection needs. ELEsenson laser displacement sensors turn tiny distance changes into controllable, visible, and accurate data. With reliable industrial performance and all‑scenario adaptability, they bring stable precision and efficient intelligent detection to modern manufacturing.
Sweep Frequency Level Sensor for Jam Production | Food-Grade Detection
01.Jam Production Pain Points | Why Ordinary Level Sensors Fail
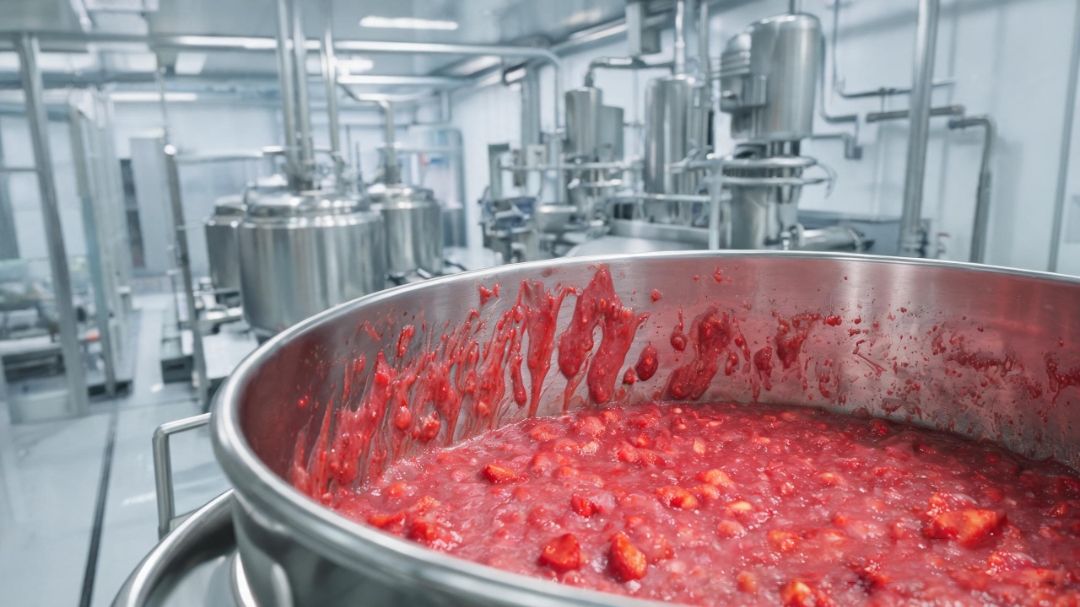
Jam production features highly viscous raw materials mixed with dense fruit pulp, which easily adheres to equipment surfaces. During stirring, boiling, and automated filling processes, materials frequently produce foam, steam, and turbulent liquid fluctuations. Conventional standard level sensors are unable to distinguish between residue buildup, foam interference, and real liquid level changes, resulting in frequent false alarms, signal instability, and inaccurate level feedback. These defects easily cause production interruptions, material overflow, equipment idling, and unstable batch quality, becoming a key bottleneck restricting automated and continuous jam production.
02.Working Principle | Intelligent RF Sweep Frequency Detection Technology
ELEsenson sweep frequency level sensor adopts advanced intelligent RF sweep frequency detection technology. It emits high-frequency variable sweep signals to monitor real-time changes in medium impedance and admittance. Equipped with self-developed intelligent algorithm logic, the sensor accurately identifies and distinguishes air, surface foam, probe residue, and real jam medium. It automatically filters various interference signals caused by viscosity, adhesion, and foaming, outputs stable and true level data, and supports real-time monitoring and full-process automatic control for jam production lines.
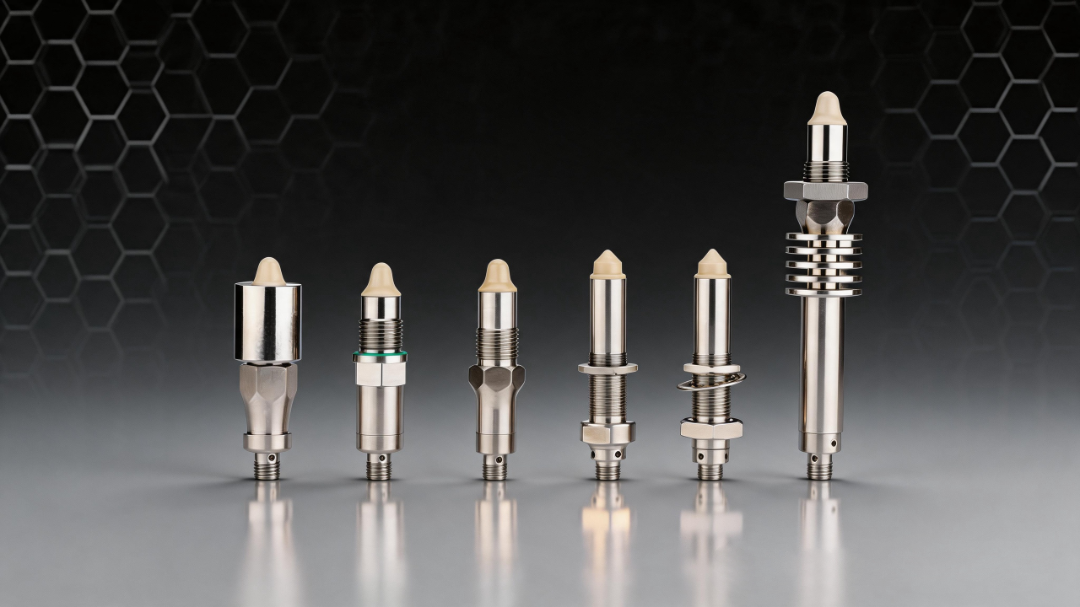
03.Core Advantages of Food-Grade Sweep Frequency Level Sensor
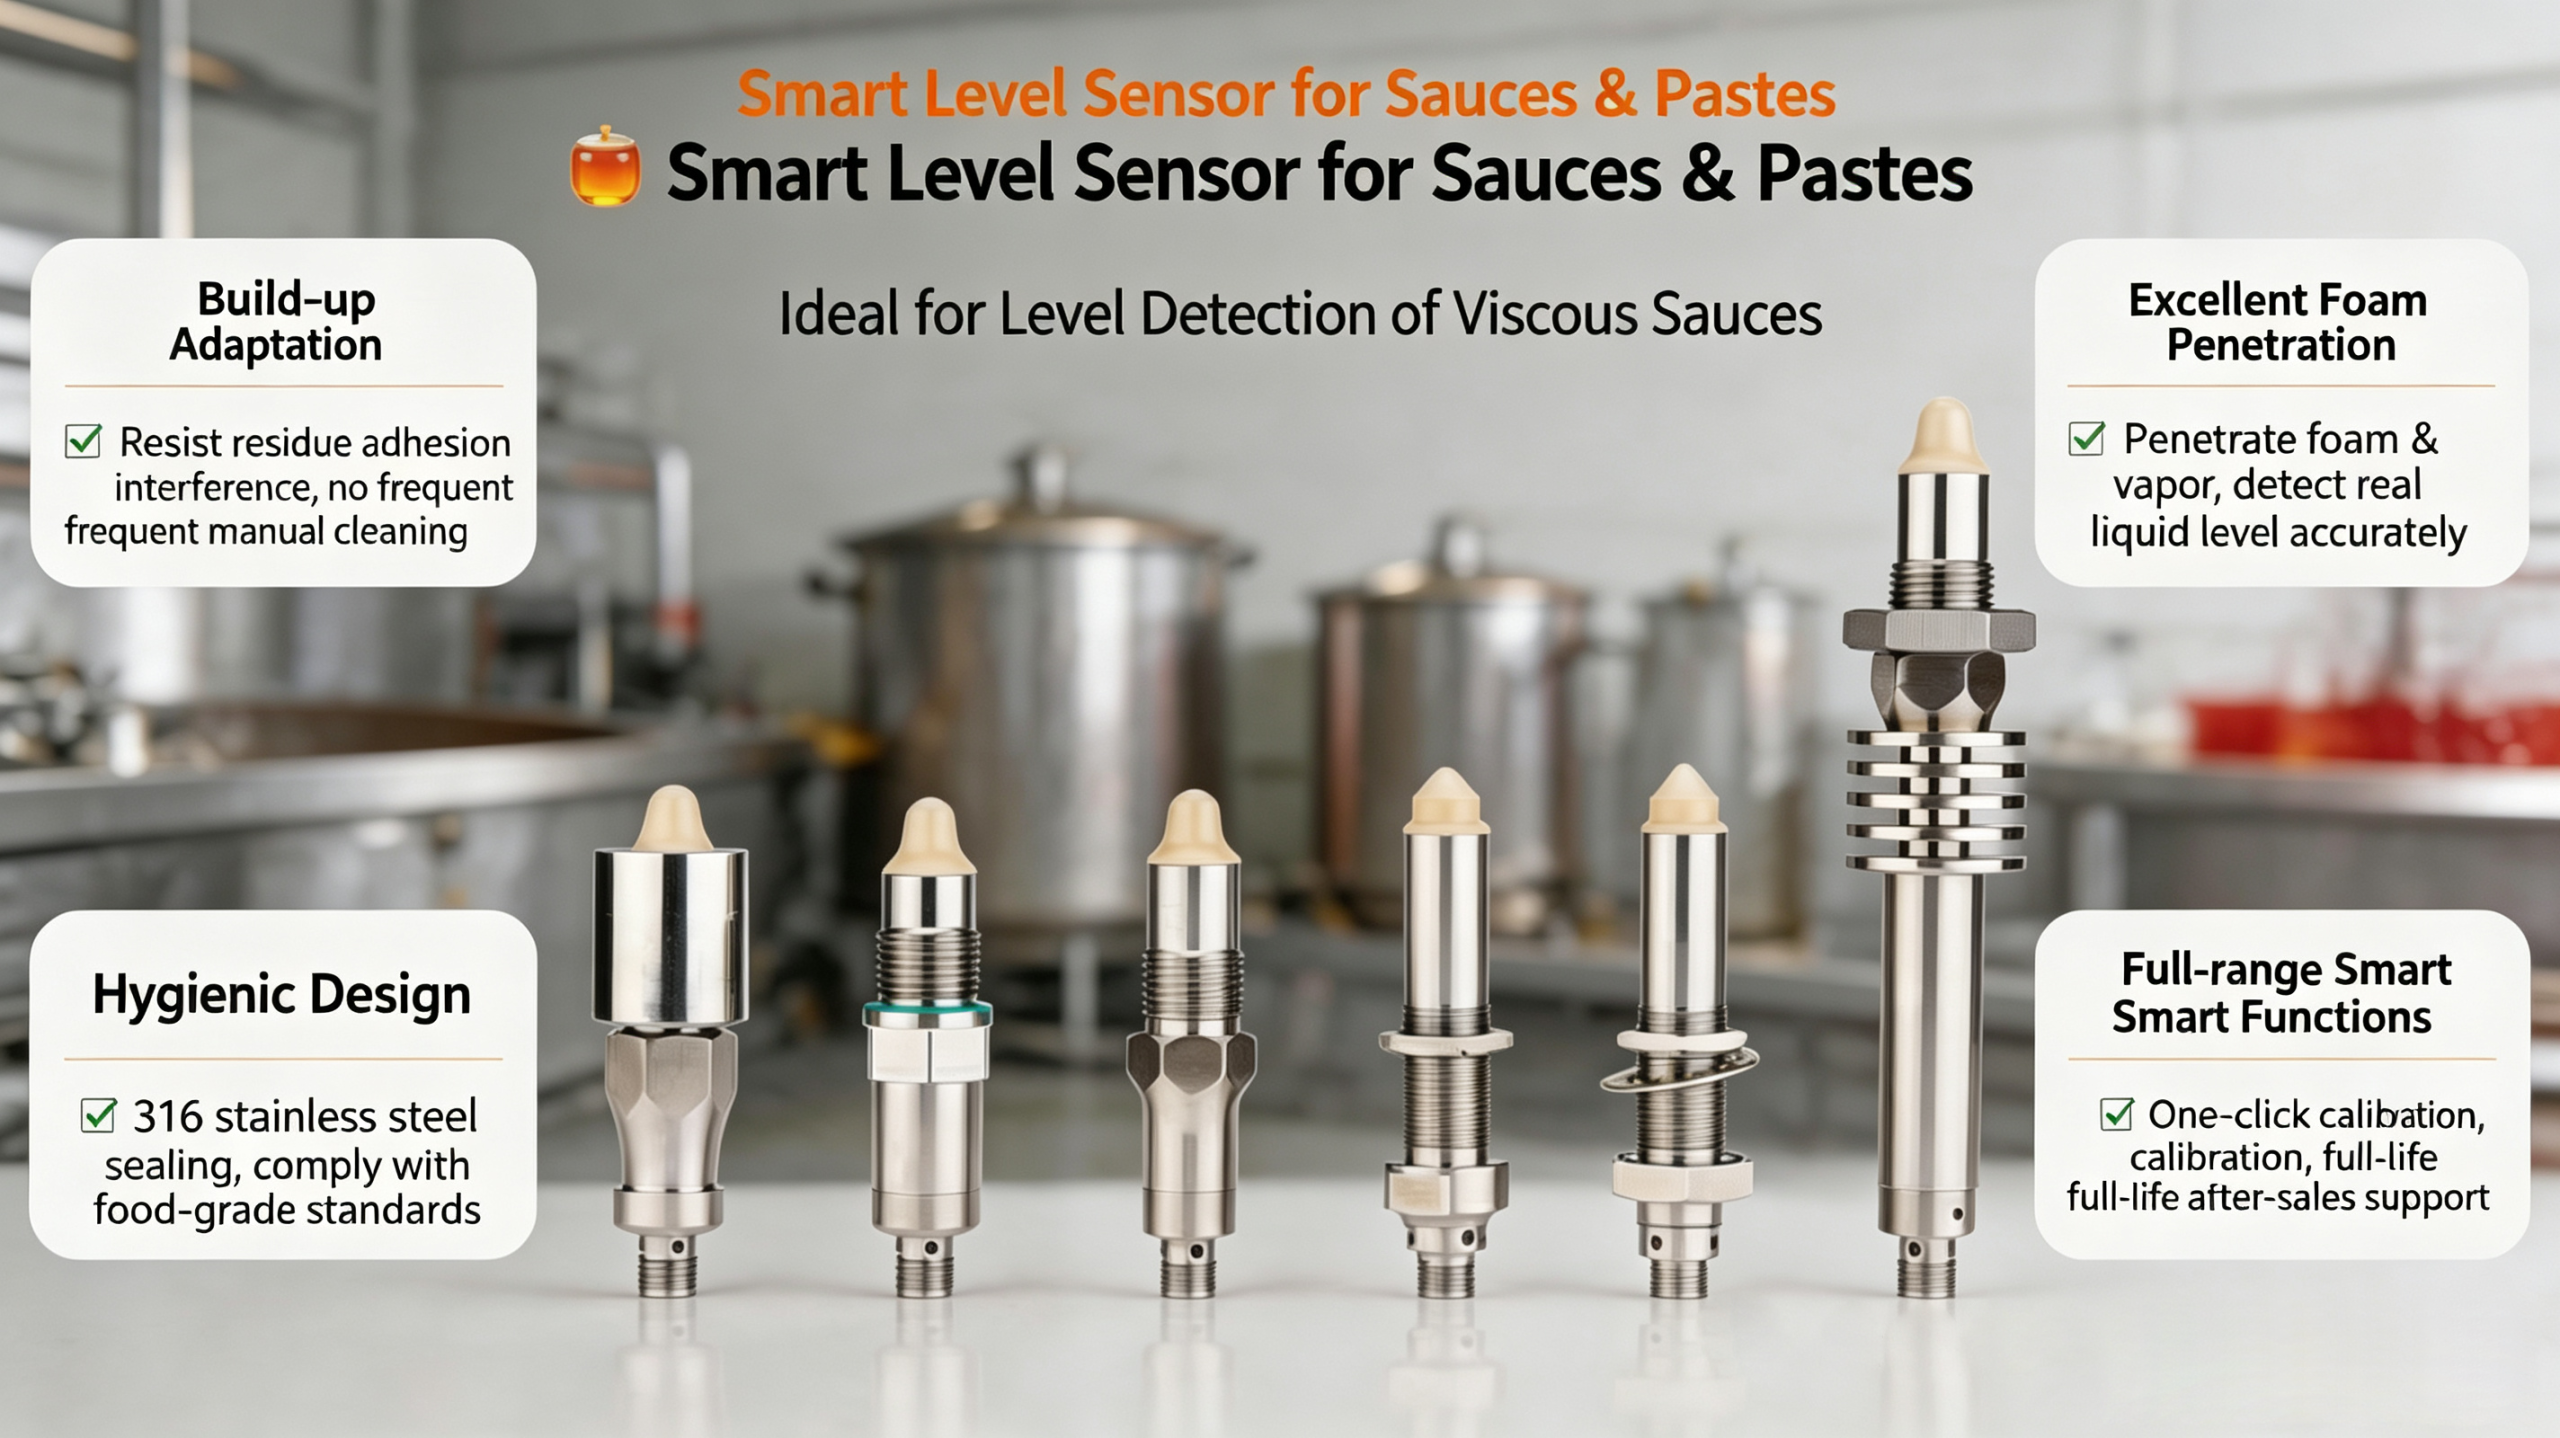
3.1 Adaptive Residue Suppression, Stable Detection Without False Alarms
Built with an adaptive residue suppression algorithm, the sensor effectively filters interference caused by thin sauce layers and pulp residue adhering to the probe surface. It only responds to real material level fluctuations and ignores static adhesion residue. It eliminates frequent manual cleaning work, completely solves the industry pain point of false alarms caused by viscous jam buildup, and ensures long-term stable and drift-free detection.
3.2 Strong Foam Penetration Capability, True & Accurate Liquid Level
Aiming at massive foam and steam generated during high-speed stirring and boiling of jam raw materials, the sensor features powerful foam penetration performance. It effectively ignores liquid surface turbulence and floating foam interference, locks the real medium liquid level, eliminates foam-induced false level alarms, and ensures continuous and stable production rhythm without frequent equipment shutdown and adjustment.
3.3 Food-Grade Sterile Structure, Fully Compliant with Food Safety Standards
The whole machine adopts integrated sealed 316 stainless steel structure, with no detection dead corners and no residual gaps. It supports CIP online cleaning and high-temperature sterilization, features excellent corrosion resistance and no medium contamination. It fully meets food-grade production specifications and hygienic processing requirements, ensuring safe and standardized jam food production.
3.4 Full-Medium Compatibility, Wide Adaptability for Jam Production
The sensor is universally compatible with all types of jam media, adapting to different viscosity, pulp content, and sugar concentration conditions. It supports high/low level alarm, overflow prevention, and dry-run protection functions. It can be perfectly matched with core production equipment such as stirring reaction kettles, finished product storage tanks, and filling hoppers, covering the whole-process monitoring needs of jam production.
3.5 Intelligent Debugging & Zero-Maintenance Stable Operation
Supporting one-click intelligent calibration, the equipment realizes simple and fast on-site commissioning without professional operation. With no mechanical moving parts, it is resistant to vibration and electromagnetic interference, featuring ultra-low failure rate and long-term stable operation. It effectively reduces daily operation and maintenance workload and labor costs, delivering excellent long-term cost performance for food factories.
3.6 Full-Cycle After-Sales Service, Worry-Free Production Protection
In response to the 24-hour continuous operation demand of food production lines, ELEsenson provides a complete professional after-sales maintenance system, including equipment installation and commissioning guidance, regular operational inspections, rapid malfunction response, warranty repair services, and lifelong technical consultation. Targeted solutions are provided for common monitoring problems in jam production, effectively avoiding production line shutdown risks caused by equipment failures and insufficient maintenance, and fully safeguarding long-term stable automated production.
04.Core Application Scenarios in Jam Production Lines
4.1 Stirring Reaction Kettle
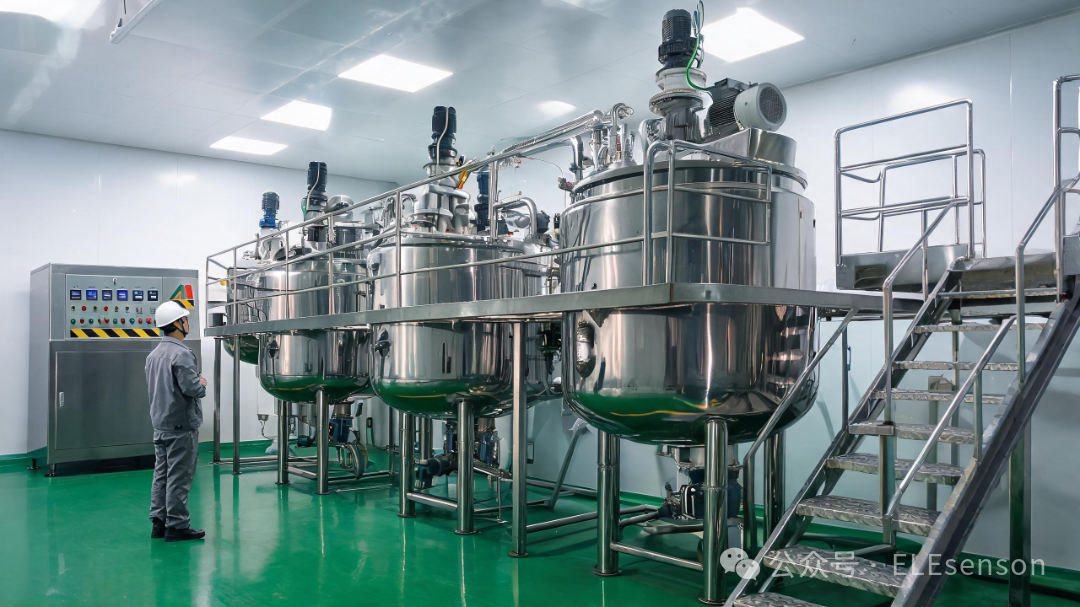
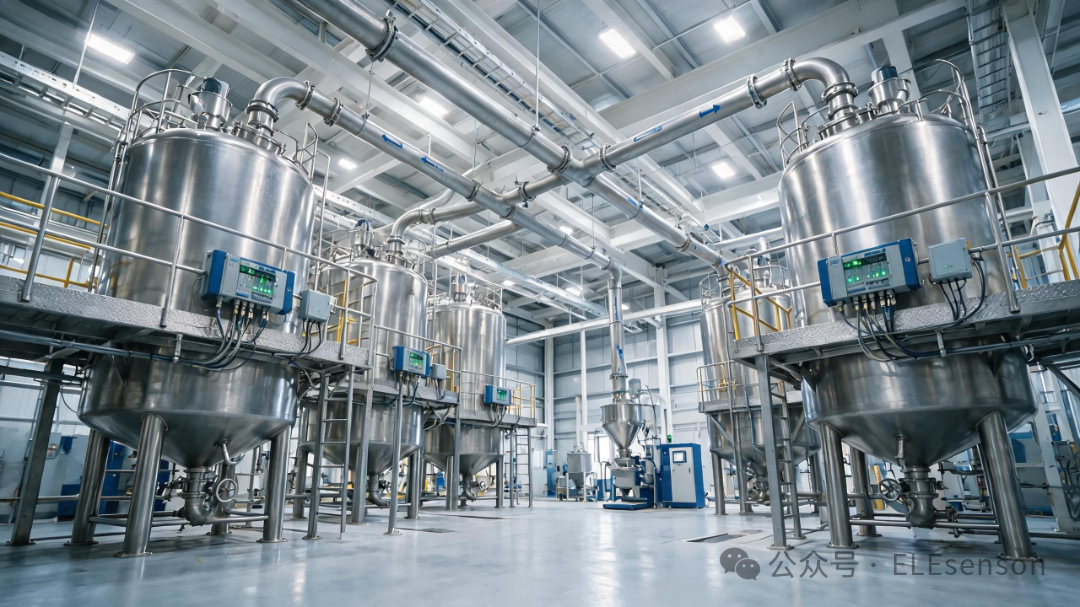
Realize high and low material level monitoring during jam stirring and boiling. The low-level protection function prevents equipment dry running and empty stirring; the high-level alarm avoids material overflow waste. Adapted to dynamic stirring and turbulent working conditions, it maintains stable level detection and ensures consistent cooking quality in each batch.
4.2 Finished Product Storage Tank
Monitor the real-time residual material level of finished jam storage tanks. Link with the conveying system to realize automatic material replenishment and automatic shutdown control. It effectively prevents production line shutdown caused by material shortage and material overflow accidents, realizing intelligent and unmanned management of finished product storage links.
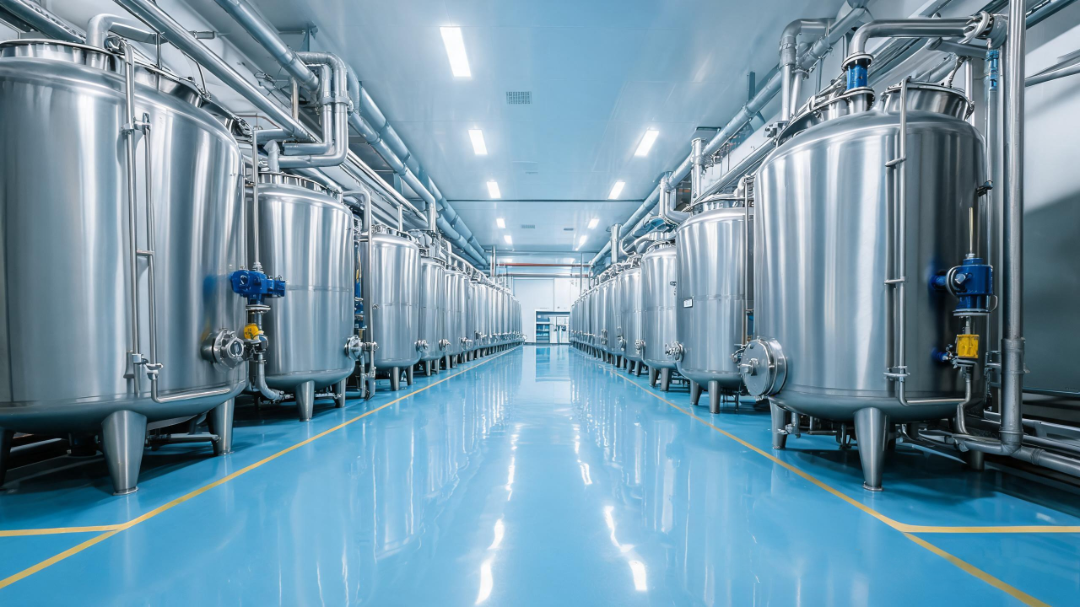
4.3 Filling Station Hopper
Accurately monitor the material level of jam in the filling hopper, synchronize with the automatic filling beat, and solve production abnormalities such as insufficient material supply, filling interruption, and liquid spillage. It stabilizes the filling production process, reduces material waste and defective products, and effectively improves overall production yield and automation efficiency.
05.Product Conclusion
Penetrating foam interference and shielding material adhesion noise, ELEsenson sweep frequency level sensor accurately captures the real material level changes inside the tank. It converts invisible and complex production working conditions into precise and controllable data, stabilizes every link of jam boiling, storage and filling with professional food-grade detection technology, strictly controls production quality, and ensures every batch of fresh jam is delivered with stable quality and reliable safety.
Ultrasonic Double Sheet Sensor | Eliminate Sheet Stacking & Production Downtime
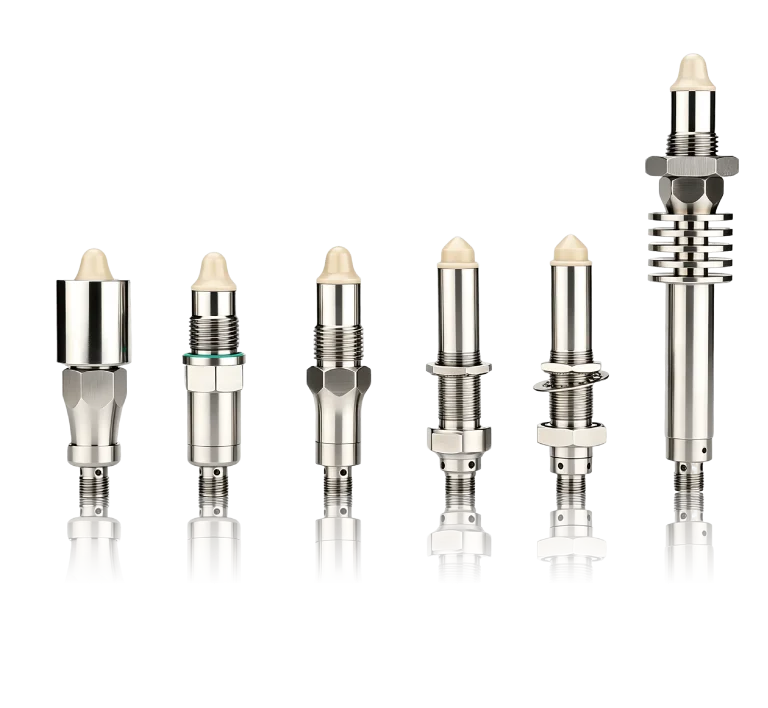
ELEsenson Ultrasonic Double Sheet Sensor is a professional non-contact detection device tailored for automated sheet feeding production lines. It fundamentally solves the common hidden failure of sheet overlapping, adhesion and double/multi-sheet feeding, effectively avoiding paper jams, product scrapping, tool and mold damage, and frequent equipment downtime caused by stacked materials. It delivers stable, high-precision layer detection for diverse thin materials across industrial scenarios, greatly reducing production loss and improving line operational efficiency.
01.Core Pain Points of Sheet Stacking in Automated Production
Sheet adhesion and overlapping feeding are long-standing invisible problems in automated processing. Due to static electricity, material friction and mechanical feeding deviation, two or more sheets often enter the workstation undetected. This abnormal condition directly triggers a series of production failures: equipment paper jams, finished product defects and scrapping, precision cutting tool wear, mold collision damage, and unplanned line shutdowns. These issues not only raise raw material and maintenance costs but also severely restrict continuous production capacity and product yield.
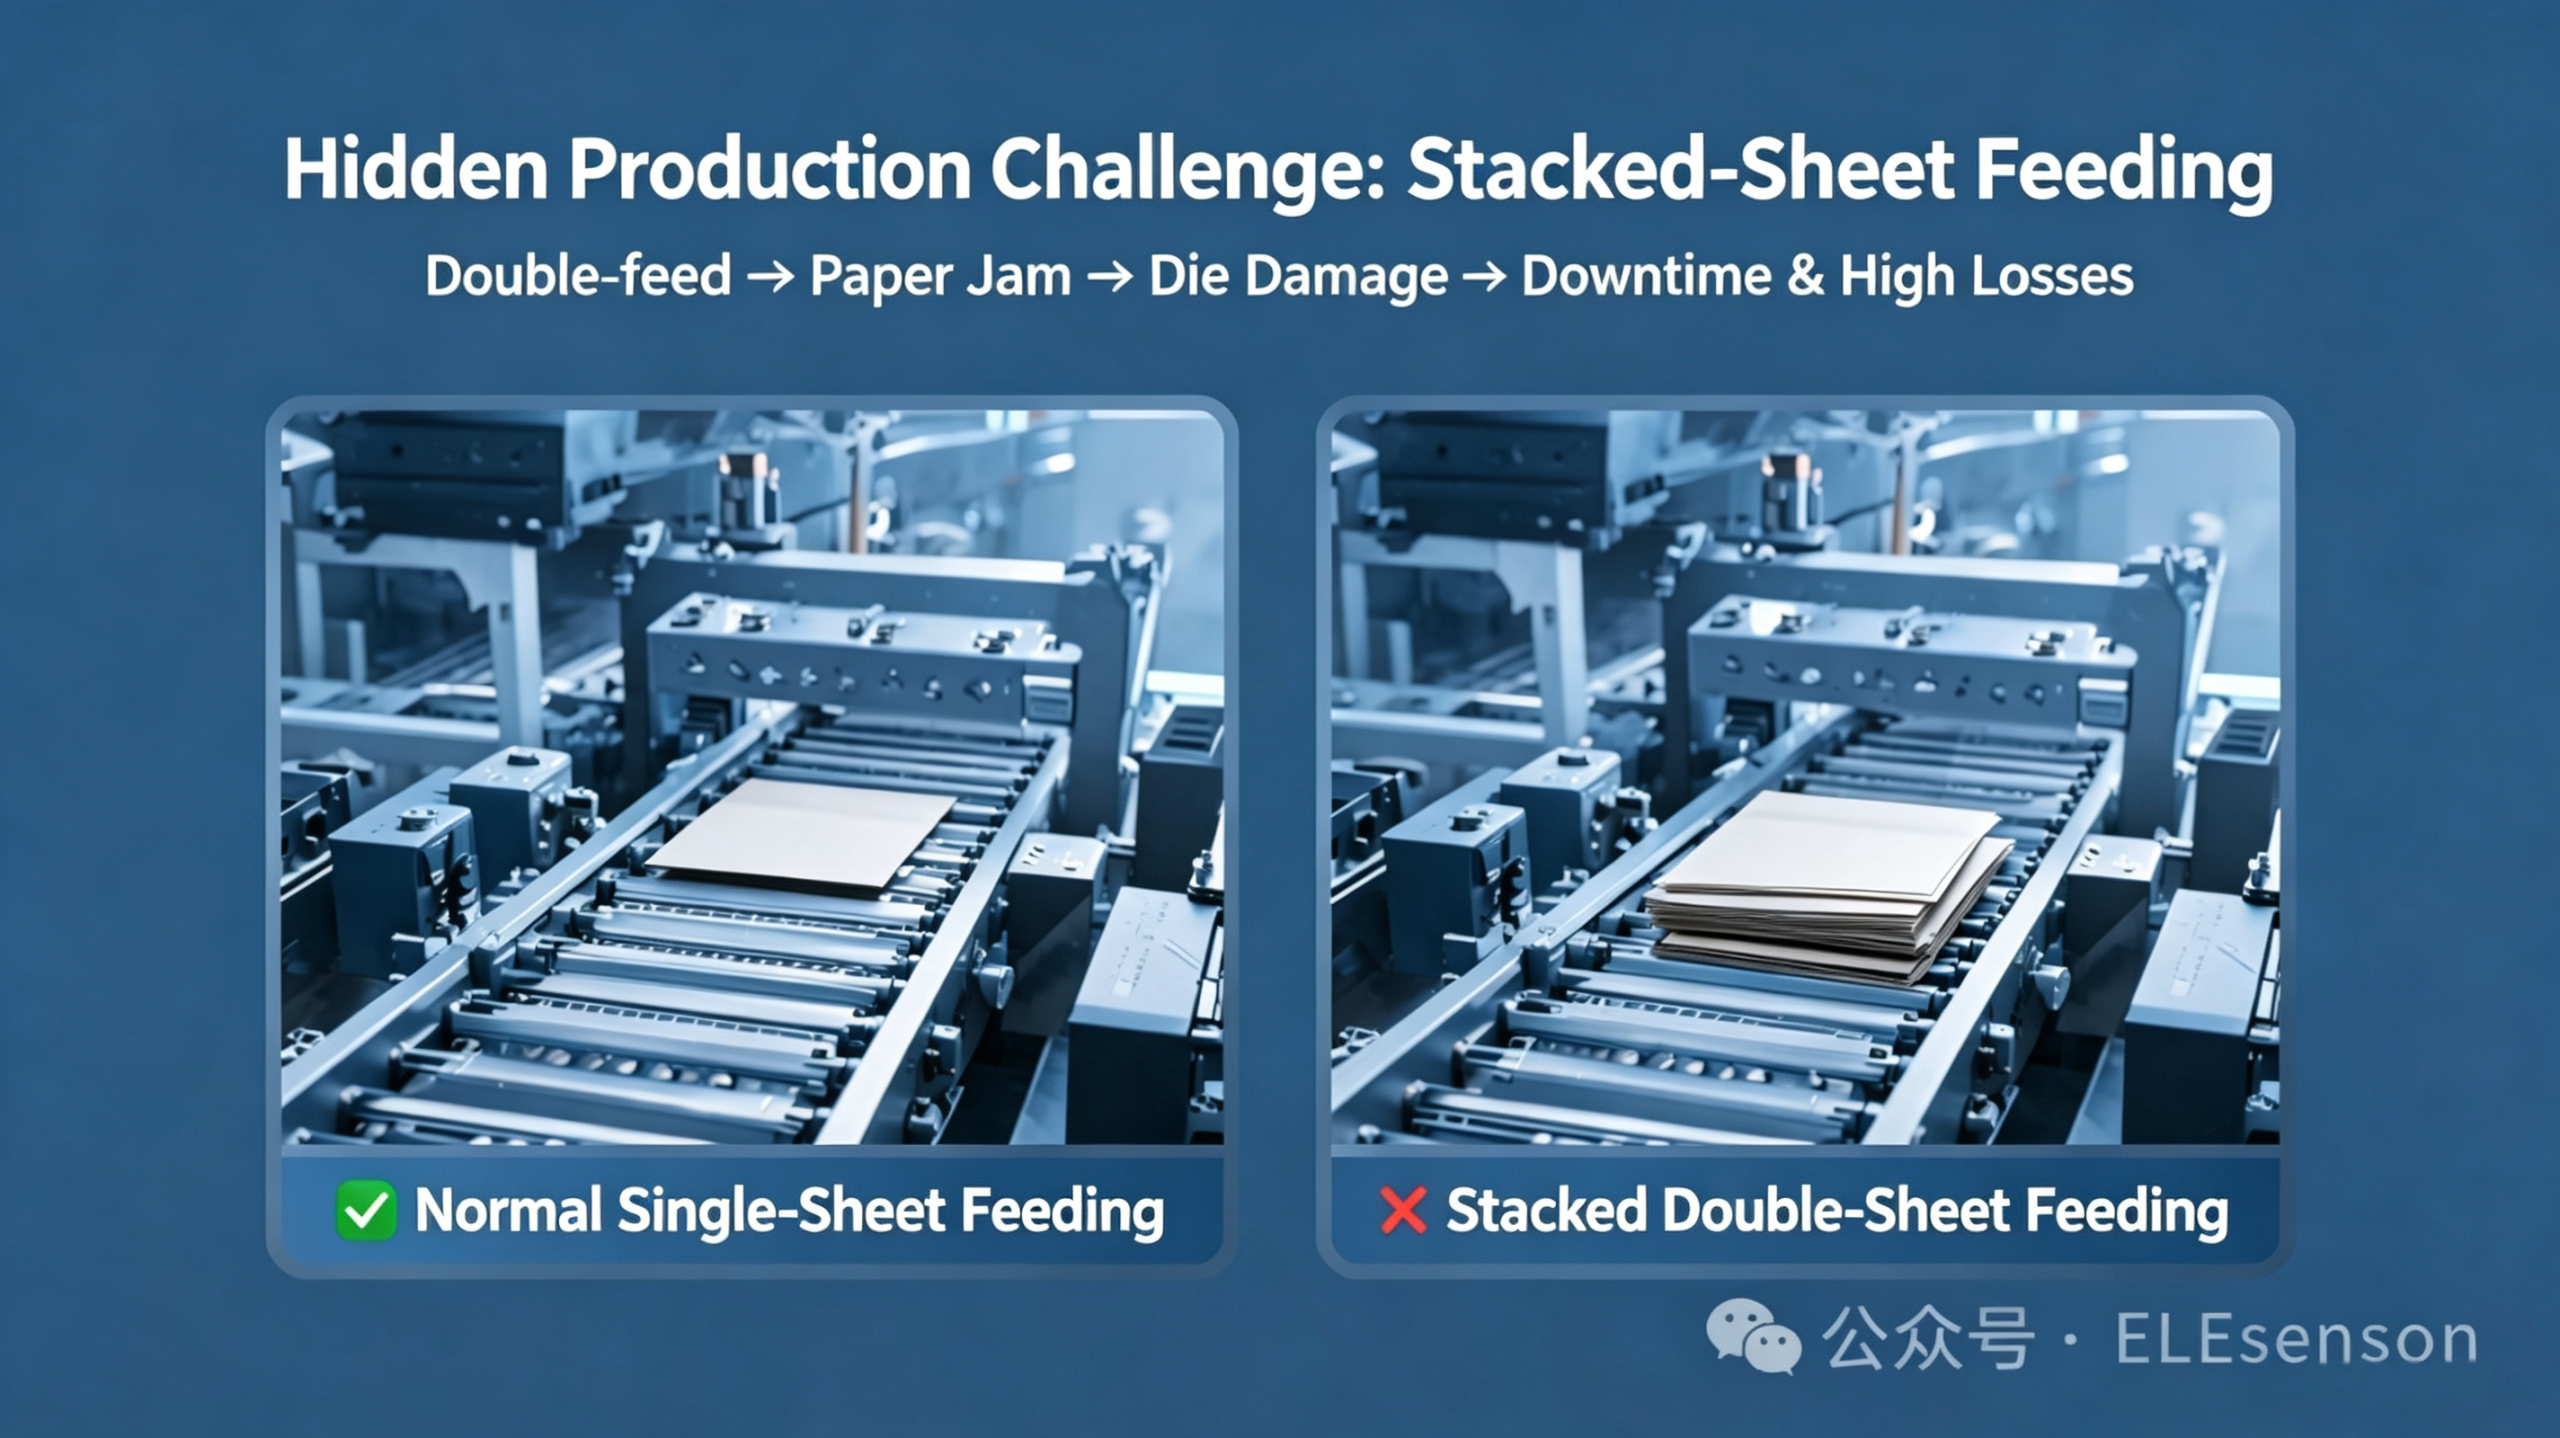
02.Working Principle: Non-Contact Ultrasonic Penetration Detection
Different from traditional photoelectric sensors limited by material appearance, the ELEsenson ultrasonic double sheet sensor adoptsultrasonic sound wave penetration principle for non-contact real-time detection. It accurately identifies four material states: no material, single sheet, double sheets, and multi-sheet stacking. The sensor intercepts stacking risks at the feeding source, realizing full-process error prevention for sheet feeding and ensuring stable, continuous and efficient operation of automated production lines.
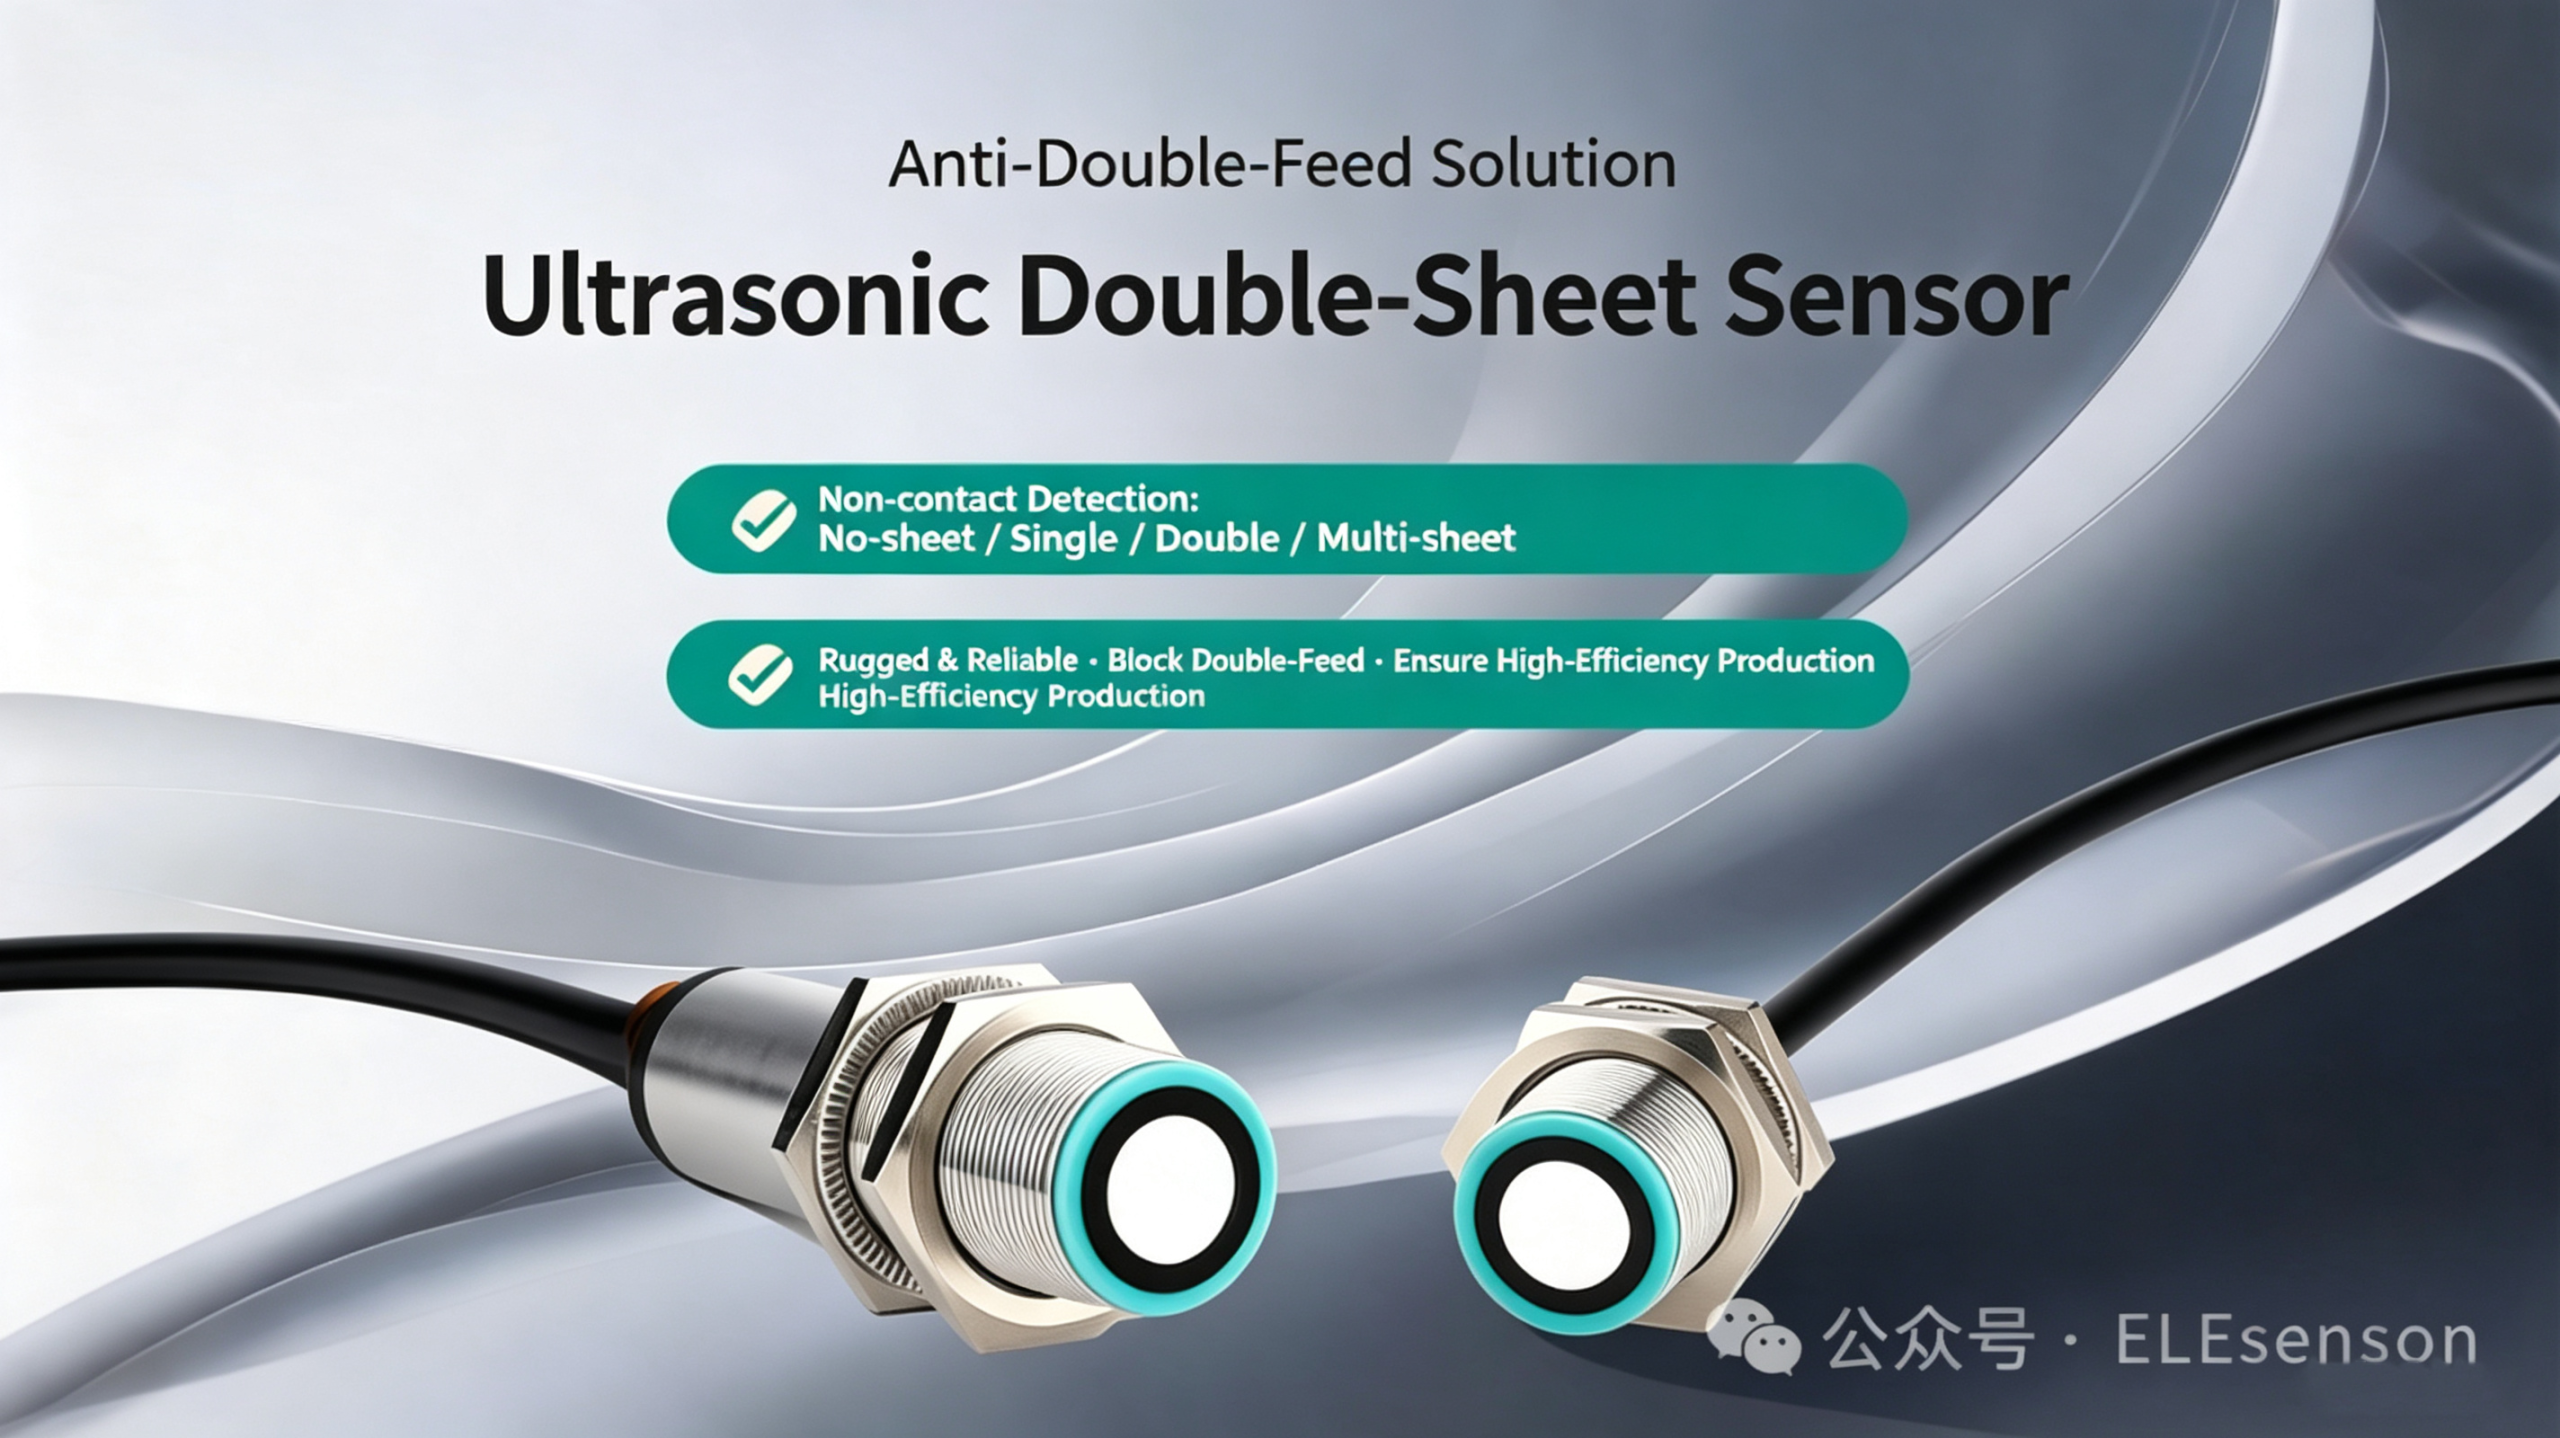
03.Core Advantages & Key Technical Features
3.1 Color & Transparency Independent Detection, Wide Material Compatibility
Relying on ultrasonic penetration rather than visible light reflection, the sensor is completely immune to material color, transparency, surface reflectivity and pattern differences. It perfectly makes up for the detection blind spot of photoelectric sensors on transparent and high-reflective materials. It supports reliable detection of paper, packaging film, aluminum foil, copper foil, lithium battery separators, and thin PCB boards, covering most thin industrial materials.
3.2 0.02–4mm Ultra-Wide Detection Range with One-Touch Teaching
It covers an ultra-wide material thickness range of0.02mm to 4mm, adapting from ultra-thin micro-films to thin metal sheets. Equipped with one-touch teaching function, it supports one-click parameter calibration during material switching. It greatly shortens production line changeover and debugging time, improves production flexibility, and meets the flexible production needs of multiple materials and multiple processes.
3.3 Millisecond High-Speed Response, Adapt to High-Speed Production Lines
With millisecond-level signal output speed, the sensor synchronizes with high-speed feeding equipment without delaying line operation. It maintains stable and accurate multi-layer identification and double-sheet judgment under high-frequency and high-speed operating conditions, ensuring detection accuracy and production efficiency do not conflict.
3.4 IP65 Industrial Protection, Stable for Harsh Workshop Environments
Built with IP65 dustproof and waterproof rating, the sensor integrates reverse connection protection and transient overvoltage protection functions. It resists workshop dust, light oil pollution, and temperature & humidity fluctuations. It effectively avoids false detection and missing detection during long-term continuous operation, maintaining consistent and reliable detection performance in complex and harsh industrial environments.
3.5 Plug-and-Play Integration, Compatible with PLC Systems
It supports optional NPN/PNP dual signal output, which can be directly connected to industrial PLC equipment. It features simple wiring, fast installation and zero-compatibility adaptation. It is applicable to both new automated machinery and old equipment renovation, realizing rapid deployment and online use with low application threshold.
04.Multi-Industry Industrial Application Scenarios
4.1 Printing & Packaging Industry
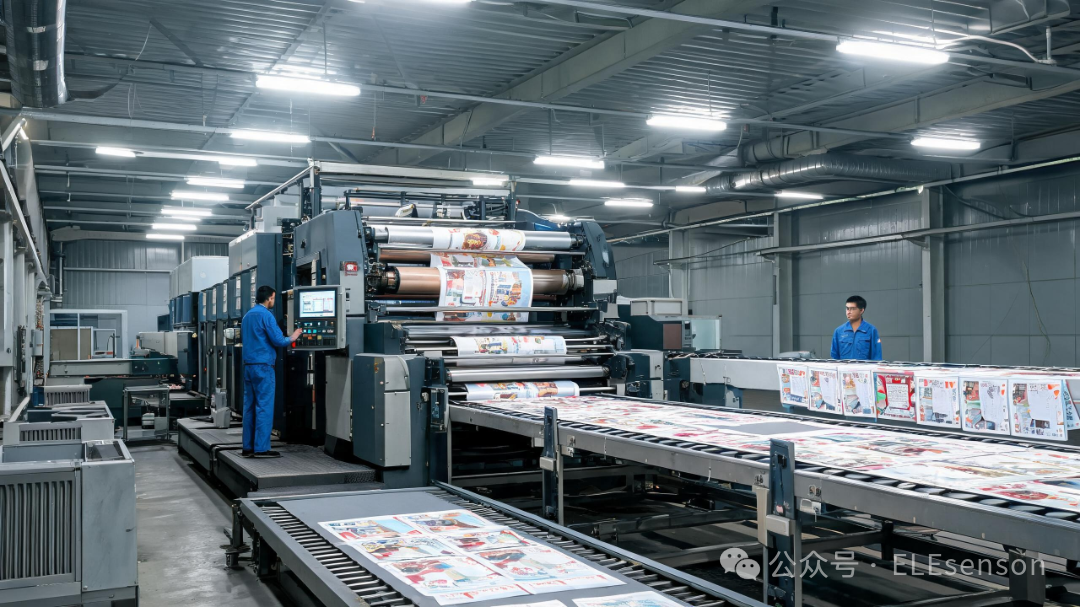
Applicable to printing machines, box gluing machines, laminating machines and collating machines. It detects paper, cardboard, label paper and packaging film, effectively preventing double-sheet feeding caused jams, printing registration errors and product scrapping. It reduces equipment maintenance frequency and stabilizes packaging line productivity.
4.2 Lithium Battery Manufacturing
Deployed on battery stacking workstations to detect battery separators, positive/negative electrode sheets, copper foil and aluminum foil. It accurately alarms for double-layer stacking, eliminates battery short-circuit risks caused by stacked electrode materials, improves battery product yield, and ensures safe and standardized battery production.
4.3 Precision Electronics Manufacturing
Suitable for conveying and detection of FPC flexible circuits, thin PCBs and silicon wafers. It identifies stacked sheet materials in real time to prevent multi-layer materials from entering precision processing stations, protecting cutting tools, stamping parts and precision electronic components from damage, and reducing precision equipment loss.
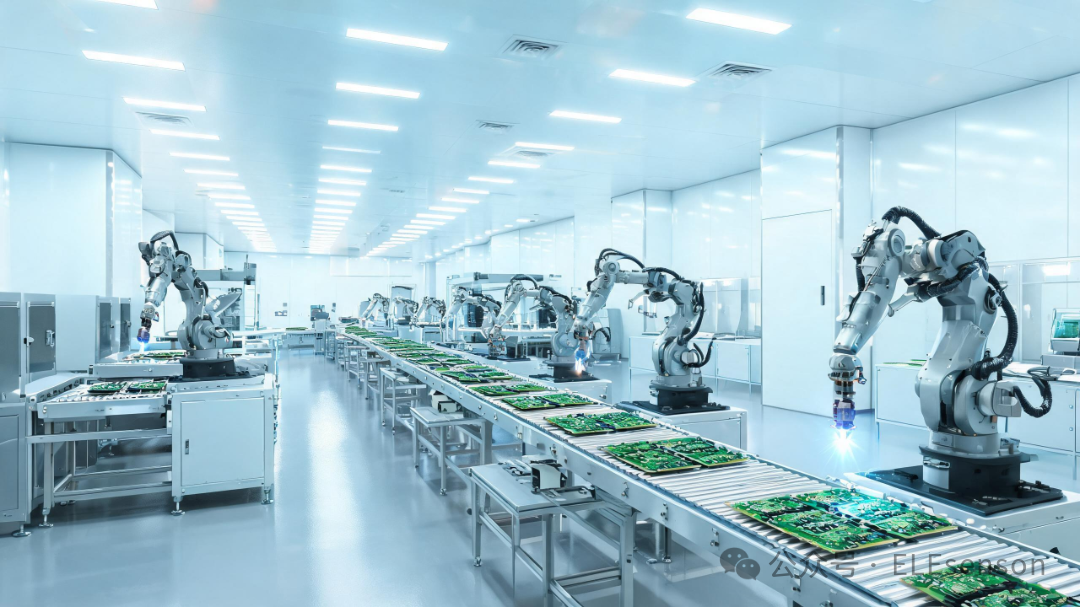
4.4 Flexible Packaging & Metal Stamping
Matching bag-making machines, film laminating production lines and hardware stamping sorting systems. It detects aluminum-plastic film, plastic film and thin metal sheets to avoid double-layer feeding faults, protect molds and core equipment, and reduce raw material waste and defective rate.
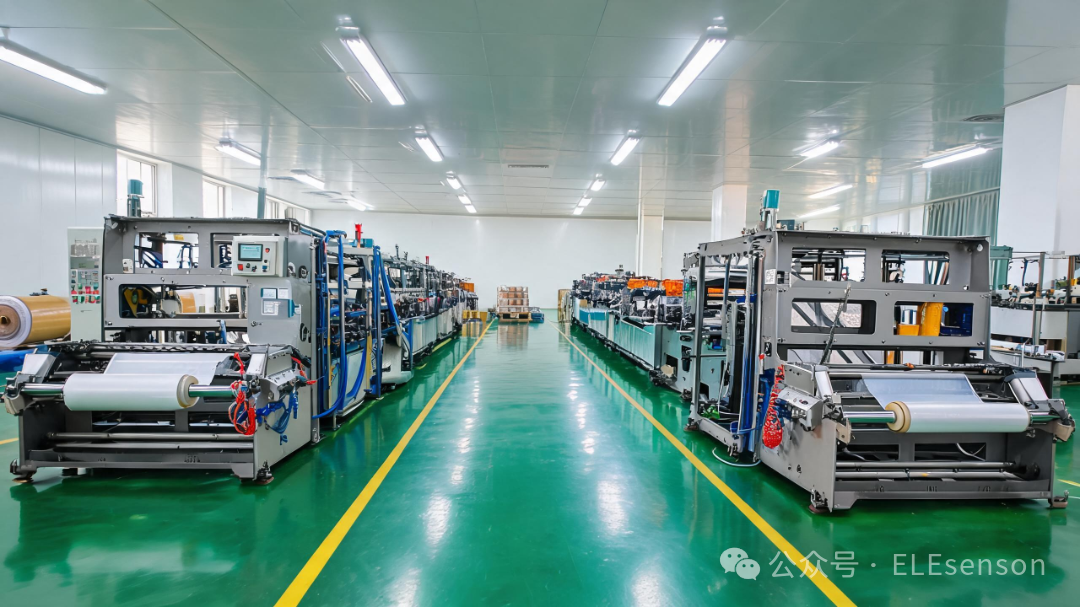
4.5 Food Packaging Production
Food packaging films, aluminum-plastic composite films and seasoning bag materials are prone to adhesion due to static electricity. Installed on bag-making machines, seasoning bag distributors and snack sealing stations, the sensor intercepts double-layer film feeding, avoids poor sealing, product leakage and package damage, and eliminates line downtime caused by packaging jams.
05.Conclusion
Sheet stacking and adhesion are key invisible faults that restrict the stability and yield of automated production lines. The ELEsenson Ultrasonic Double Sheet Sensor solves industrial detection pain points with non-contact anti-interference performance, wide material adaptability, high-speed response and industrial-grade stability. It provides efficient and reliable error-proof detection solutions for printing, new energy, electronics, packaging and stamping industries.
ELEsenson focuses on industrial precision detection, with a full range of sensor products to solve various hidden production failures. We welcome users to share on-site production problems and customize targeted detection solutions.
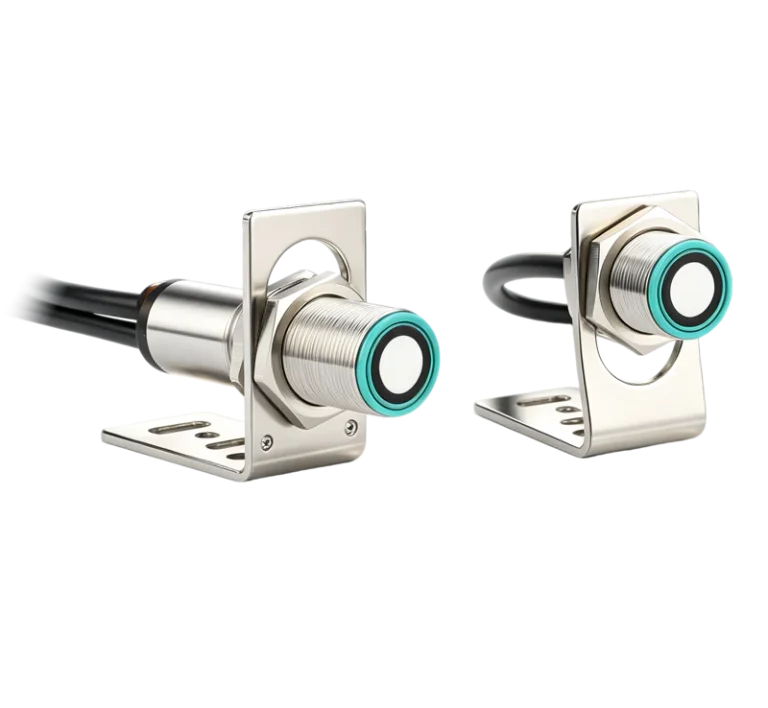
Industrial Proximity Switch | High-Precision Non-Contact Position Detection Sensor
01.Common Pain Points of Traditional Mechanical Positioning Detection
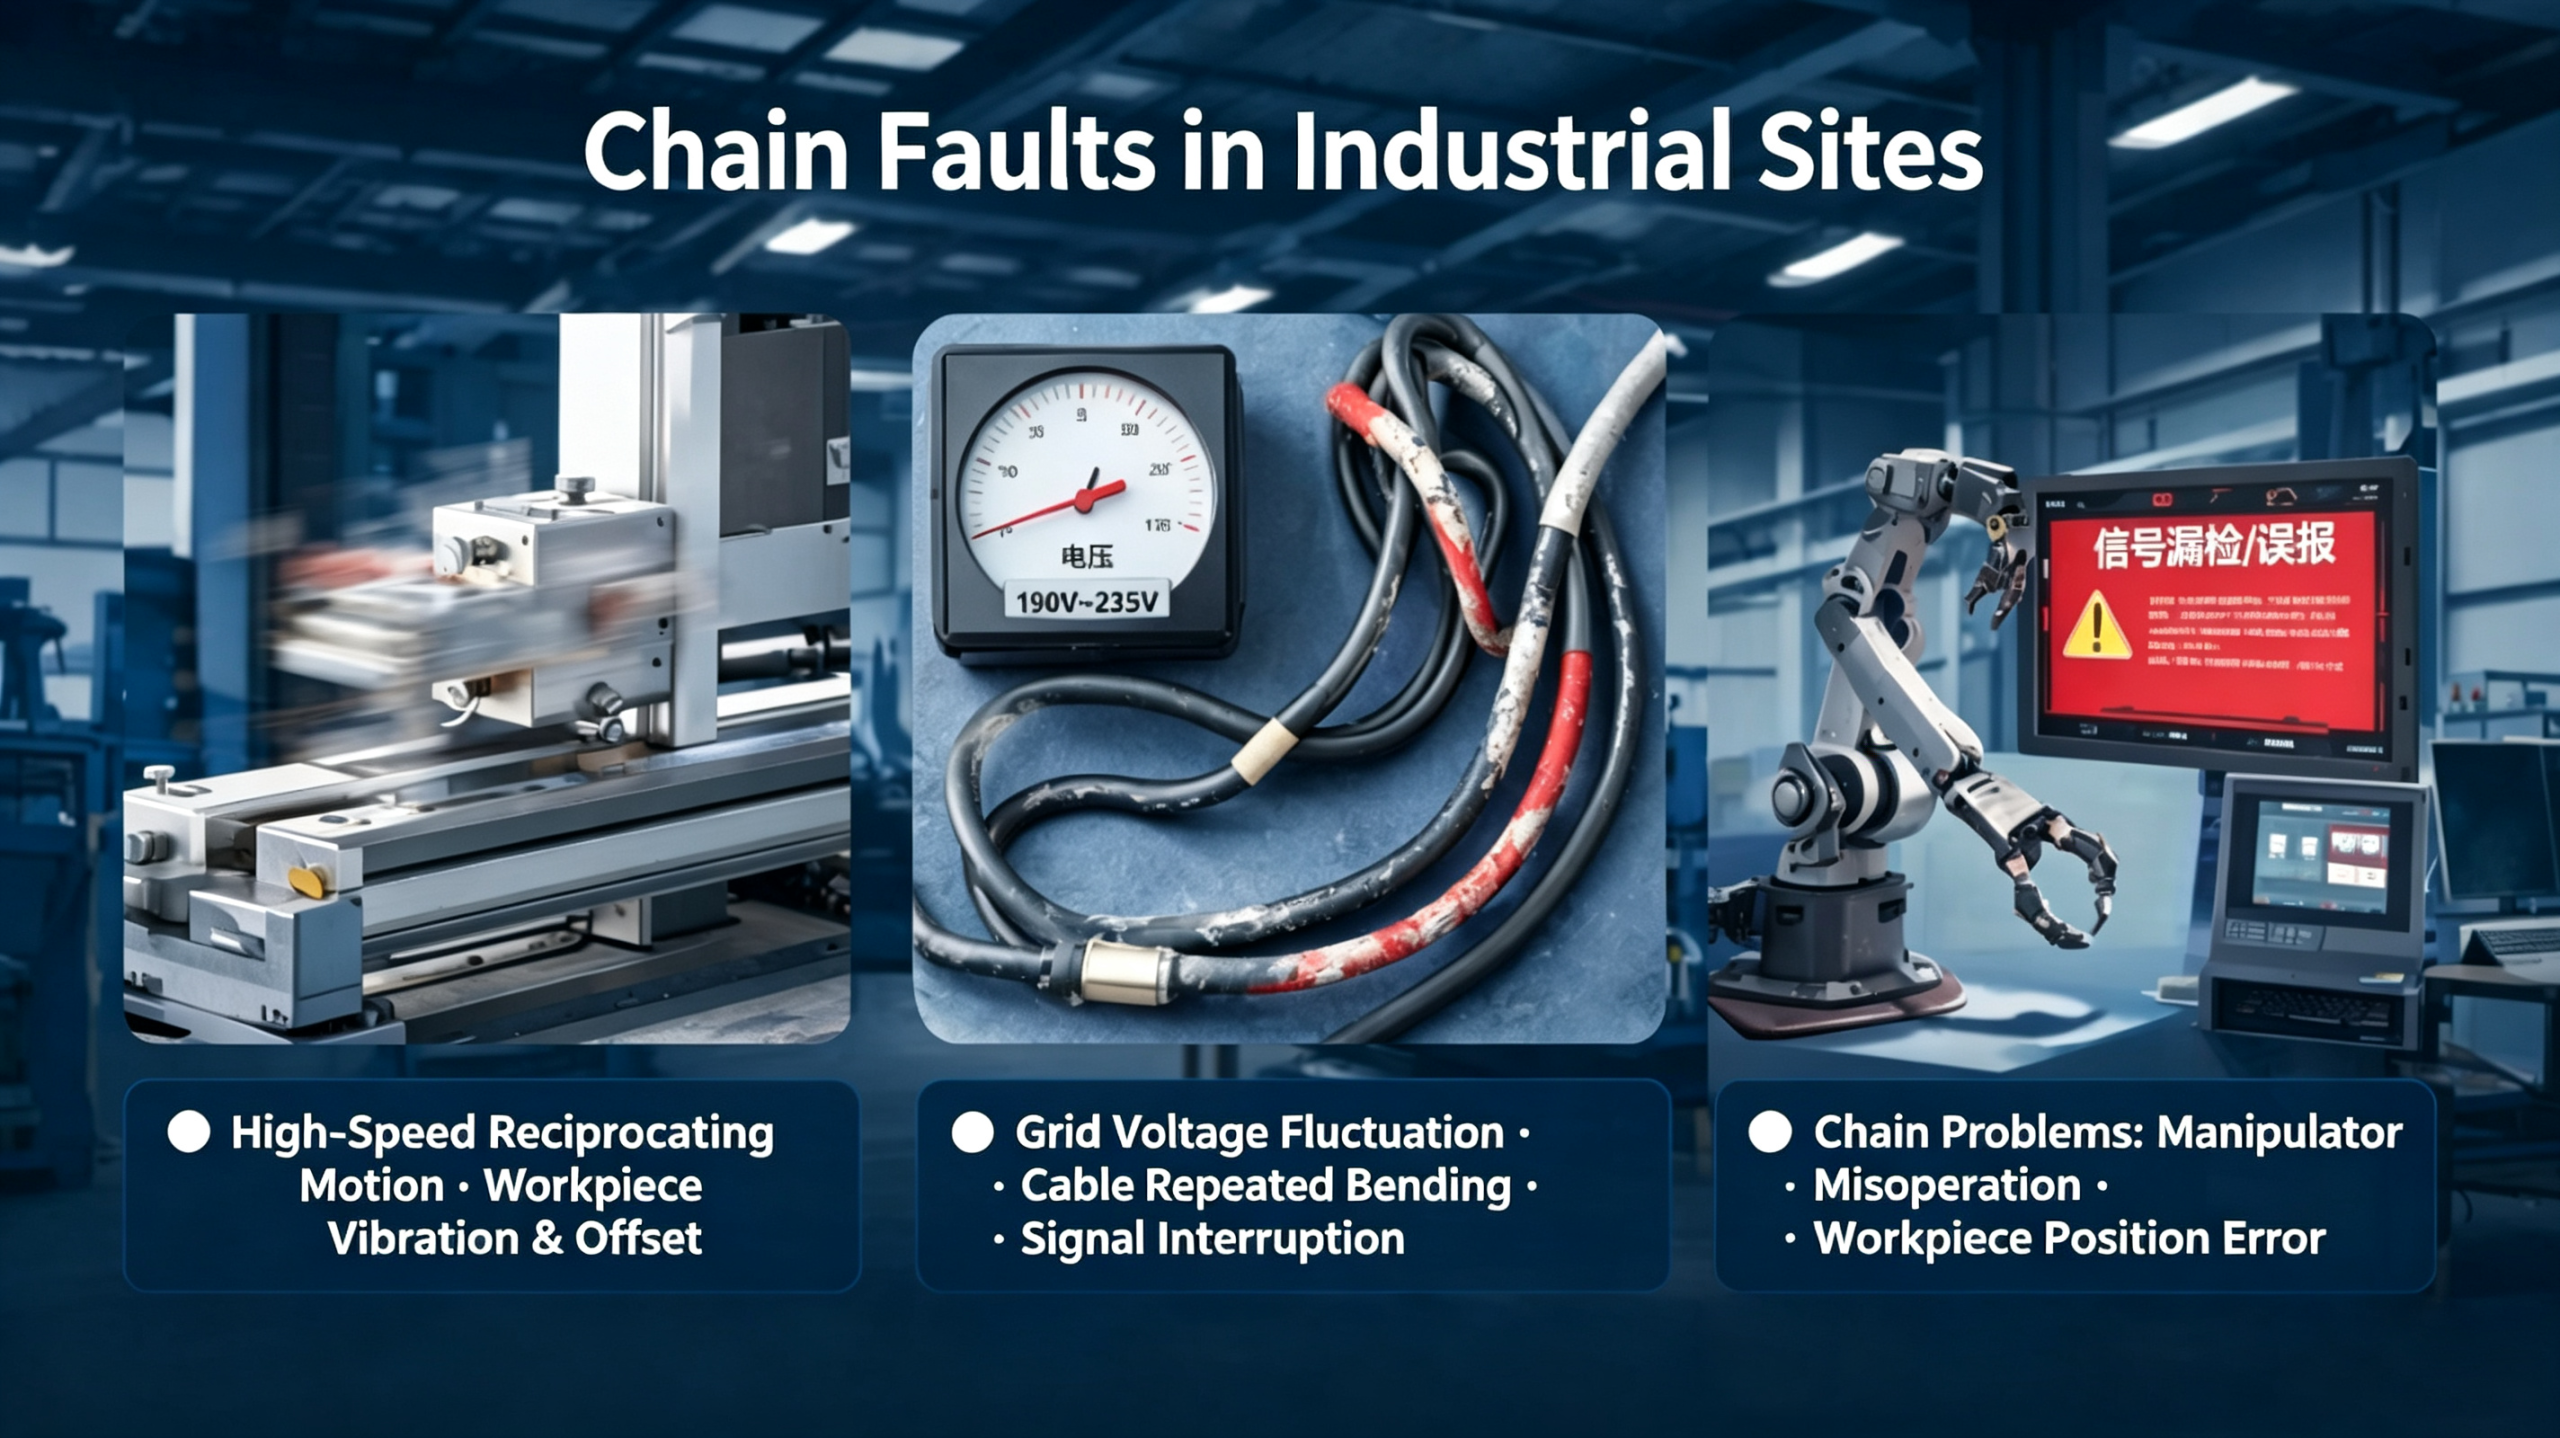
Many automated production lines still rely on traditional mechanical contact positioning methods, which cannot adapt to modern high-speed and high-frequency industrial production scenarios. On high-speed conveyor and assembly lines, frequent reciprocating equipment operation causes workpiece vibration, offset and positioning deviation. Meanwhile, workshop grid voltage fluctuation and long-term repeated cable bending easily lead to intermittent signal interruption, missed detection and false triggering.
These unstable detection problems directly cause industrial production anomalies such as empty grabbing by robotic arms, process misalignment and equipment jamming, seriously affecting production continuity, processing accuracy and operational stability, and bringing invisible losses to automated production.
02.Working Principle of Industrial Proximity Switch | Innovative Non-Contact Detection
ELEsenson industrial proximity switches adopt advanced non-contact inductive sensing technology to realize contactless real-time position monitoring of metal workpieces and mechanical mechanisms. The sensor accurately captures in-place signals without physical contact, fundamentally eliminating mechanical friction and wear caused by contact detection. It effectively solves the instability pain points of traditional mechanical switches, ensuring long-term stable and high-efficiency operation of automated equipment.
03. Core Product Advantages & Key Performance Features
3.1 Non-Contact Sensing Design, Zero Mechanical Wear & Longer Service Life
Different from traditional contact limit switches, the proximity switch completes position induction through electromagnetic sensing without touching workpieces and equipment components. It completely avoids structural wear, deformation and failure caused by frequent contact collision. It greatly extends the service cycle of the sensor, reduces equipment replacement frequency and later maintenance costs, and is perfectly suitable for high-frequency reciprocating motion and long-cycle continuous operation scenarios.
3.2 Industrial-Grade Anti-Interference & High Environmental Adaptability
Built with professional anti-electromagnetic interference circuits, the switch effectively resists complex workshop interferences such as industrial dust, oil pollution, equipment vibration and electromagnetic field fluctuation. It supports reverse polarity protection and short-circuit protection, with an IP67 high-level waterproof and dustproof rating. It can operate stably for a long time in harsh working conditions including cutting fluid splashing, heavy dust and high-vibration environments, maintaining consistent and reliable signal output.
3.3 Millisecond Fast Response, Matching High-Speed Production Cycles
Featuring ultra-high switching frequency and millisecond-level signal response speed, the sensor realizes real-time synchronous detection and feedback. It perfectly matches the high-speed operation rhythm of cylinders, sliding tables, conveyor lines and automated mechanical arms, effectively avoiding signal lag, delayed detection and false triggering problems, and ensuring precise coordination of each production process link.
3.4 Diversified Specifications & Simple Installation, Strong Compatibility
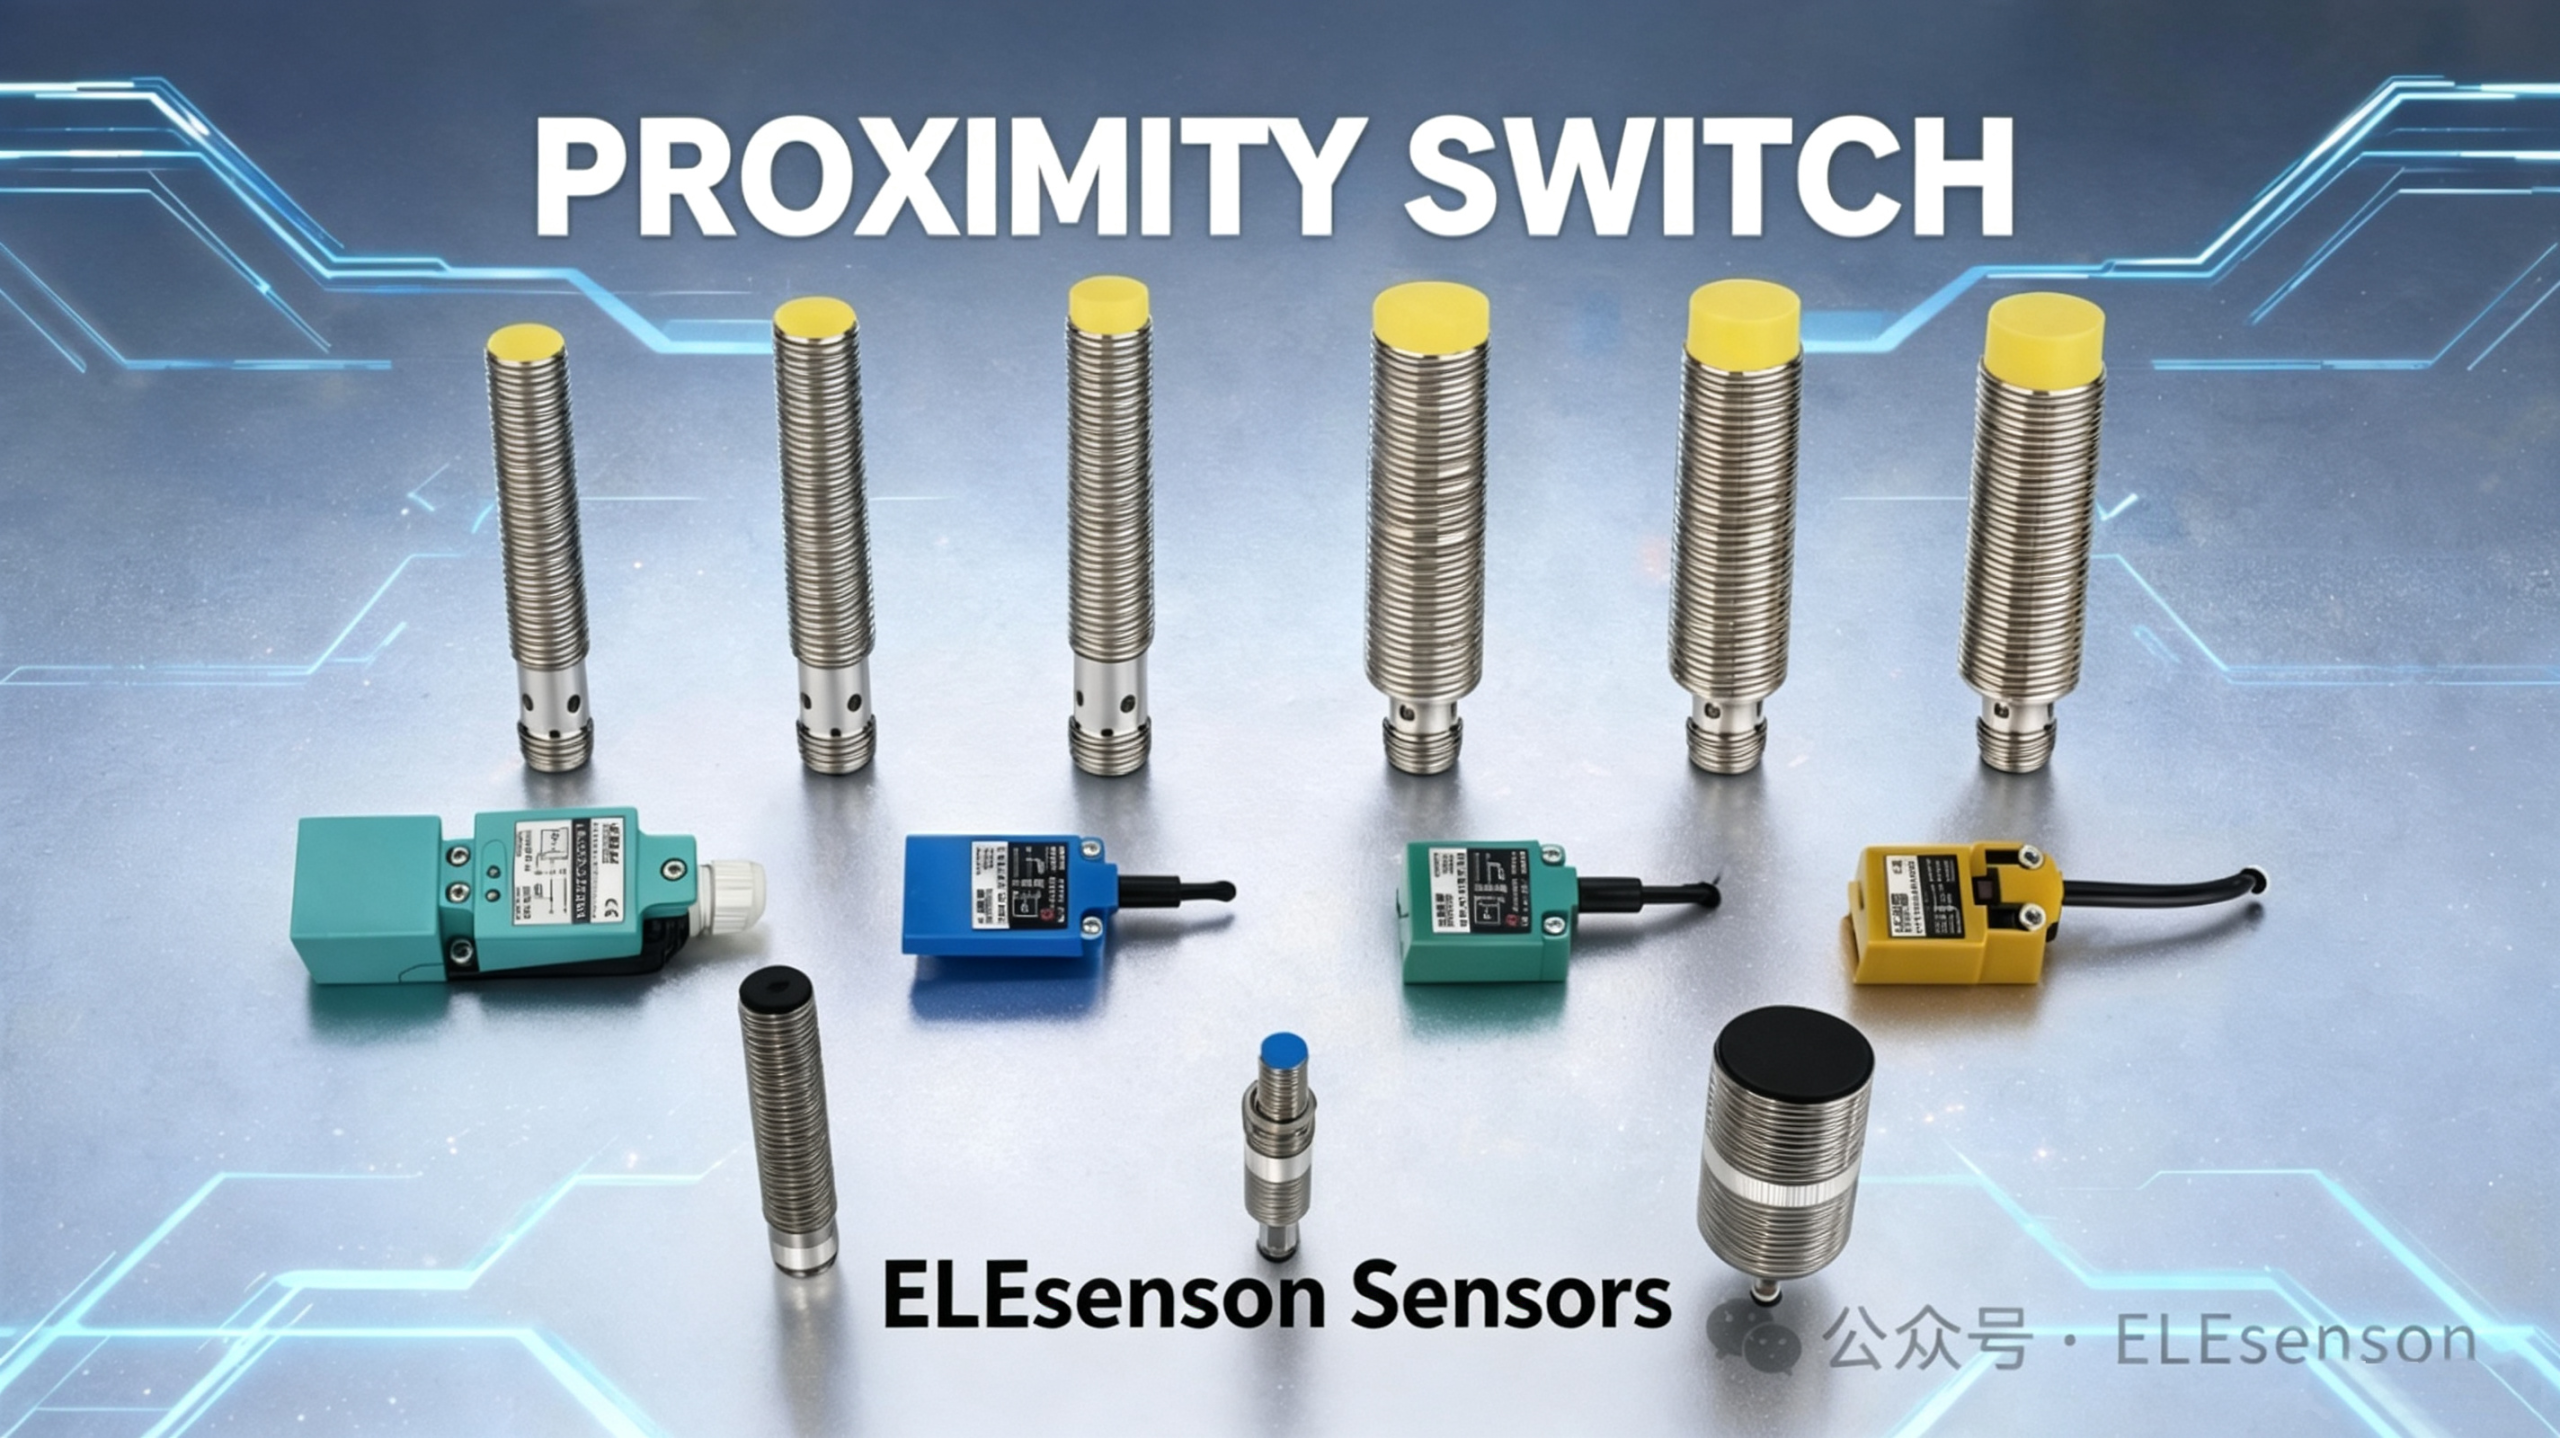
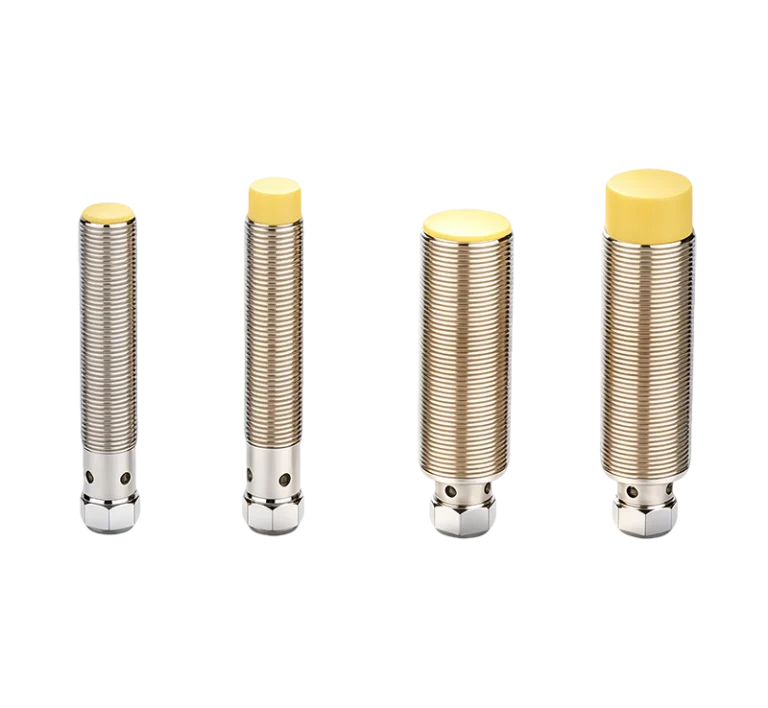
The product covers complete specifications including cylindrical M8, M12, M18, M30 and square models, supporting flush mounting and surface mounting in different installation spaces. It provides universal NPN/PNP signal output, which is highly compatible with mainstream industrial PLC control systems. It features simple wiring and convenient debugging, suitable for new equipment supporting installation and old production line renovation and upgrading.
3.5 Multiple Detection Ranges, Covering Full-Scenario Industrial Applications
Equipped with multiple optional sensing distances, it can flexibly meet diverse detection requirements from short-distance precise positioning to long-distance limit protection. It adapts to compact precision equipment and heavy-duty large-scale industrial machinery, realizing universal detection in various installation spaces and working scenarios.
04.Wide Application Scenarios, Safeguard Full-Line Automated Production
4.1 Machine Tool Processing Industry
Widely used in CNC machine tools and machining centers for sliding table travel limit detection, tool change mechanism positioning and fixture in-place verification. It replaces traditional mechanical limit switches, effectively preventing equipment over-travel failures, protecting machine tools and workpieces from damage, and ensuring high-precision machining standards.
4.2 Automated Assembly Lines
Applied to automated assembly and conveyor systems to realize metal workpiece presence detection, station positioning verification and product counting statistics. It transmits accurate position signals to the control system, standardizes the orderly operation of production processes, and guarantees continuous and efficient operation of assembly lines.
4.3 Packaging Machinery Equipment
Matching bag making machines, filling machines, sealing machines and other packaging equipment, it is used for mechanical baffle and cylinder position detection, and mechanism reset verification. It precisely coordinates the operation sequence and beat of each process, effectively reducing equipment jamming, misoperation and frequent failures.
4.4 Logistics Warehousing & Sorting Equipment
Suitable for lifting platforms, transplanting machines and intelligent sorting equipment, realizing lifting travel limit detection and pallet in-place monitoring. It avoids equipment overshoot risks, eliminates potential safety hazards, and ensures safe and stable operation of intelligent warehousing and logistics equipment.
4.5 Automotive Parts Manufacturing
Used for positioning monitoring of welding fixtures, assembly jigs and detection fixtures. It accurately identifies workpiece clamping and positioning status, effectively reducing assembly errors and defective products, and improving the overall safety and yield of automotive production lines.
4.6 Food Processing Equipment
Adapted to food processing and packaging clean production scenarios, it completes mechanical component position detection through non-contact induction. It avoids dirt accumulation and sanitary dead corners caused by contact detection, meets food-grade clean production standards, and ensures stable and hygienic equipment operation.
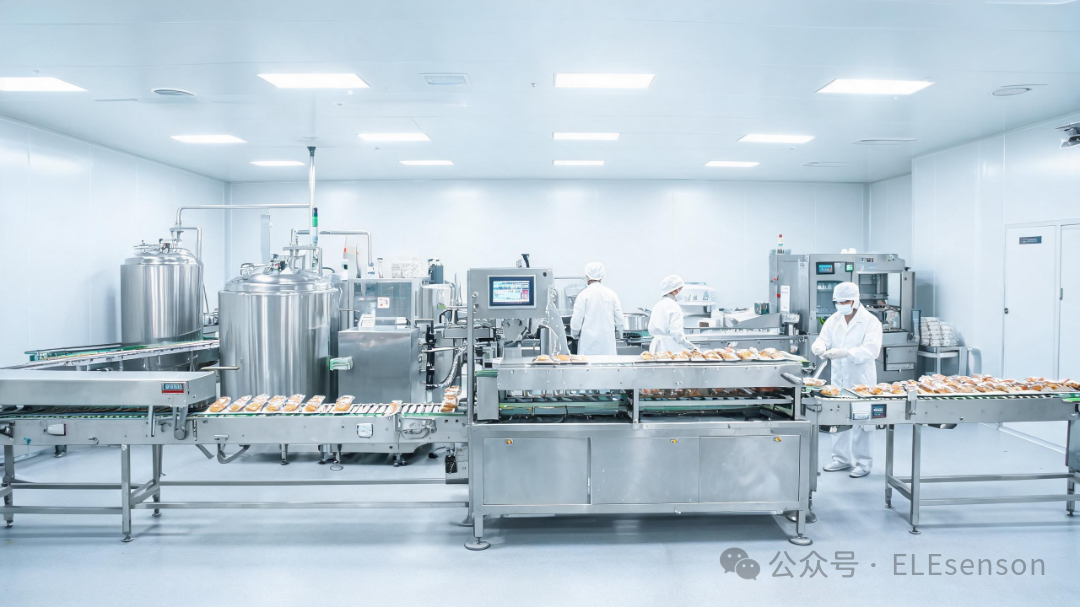
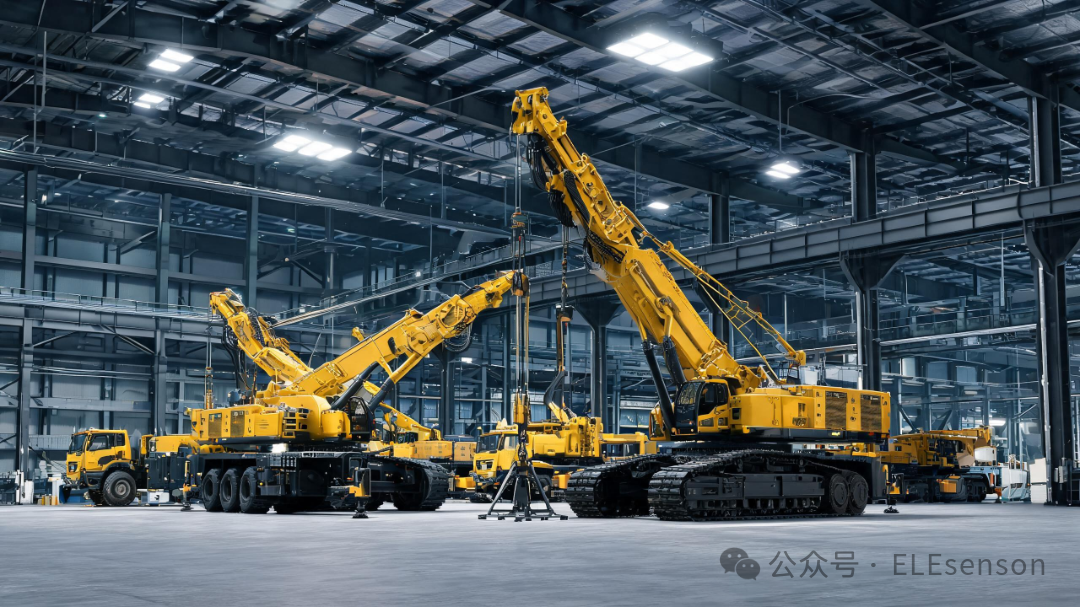
4.7 Heavy Industry & Construction Machinery
Applied to engineering lifting equipment and heavy-duty construction machinery for travel limit and stop position monitoring. It effectively prevents mechanical over-travel operation, eliminates equipment collision and structural damage risks, and reduces on-site construction safety hazards.
05.Product Value Summary
Different industrial scenarios pose completely different operational challenges: lifting equipment requires vibration resistance, machine tools need cutting fluid corrosion resistance, and food production demands clean and pollution-free detection. ELEsenson industrial proximity switches integrate anti-vibration, anti-corrosion, dustproof, waterproof and high-precision performance, targeting the differentiated needs of various industries. With reliable non-contact detection technology, it solves various positioning pain points in automated production, providing stable, efficient and cost-effective sensing support for modern industrial intelligent manufacturing.
Smart Feed Bins | Intelligent Sensing Solution for Modern Livestock Farming
01.Core Pain Points of Traditional Livestock Farming
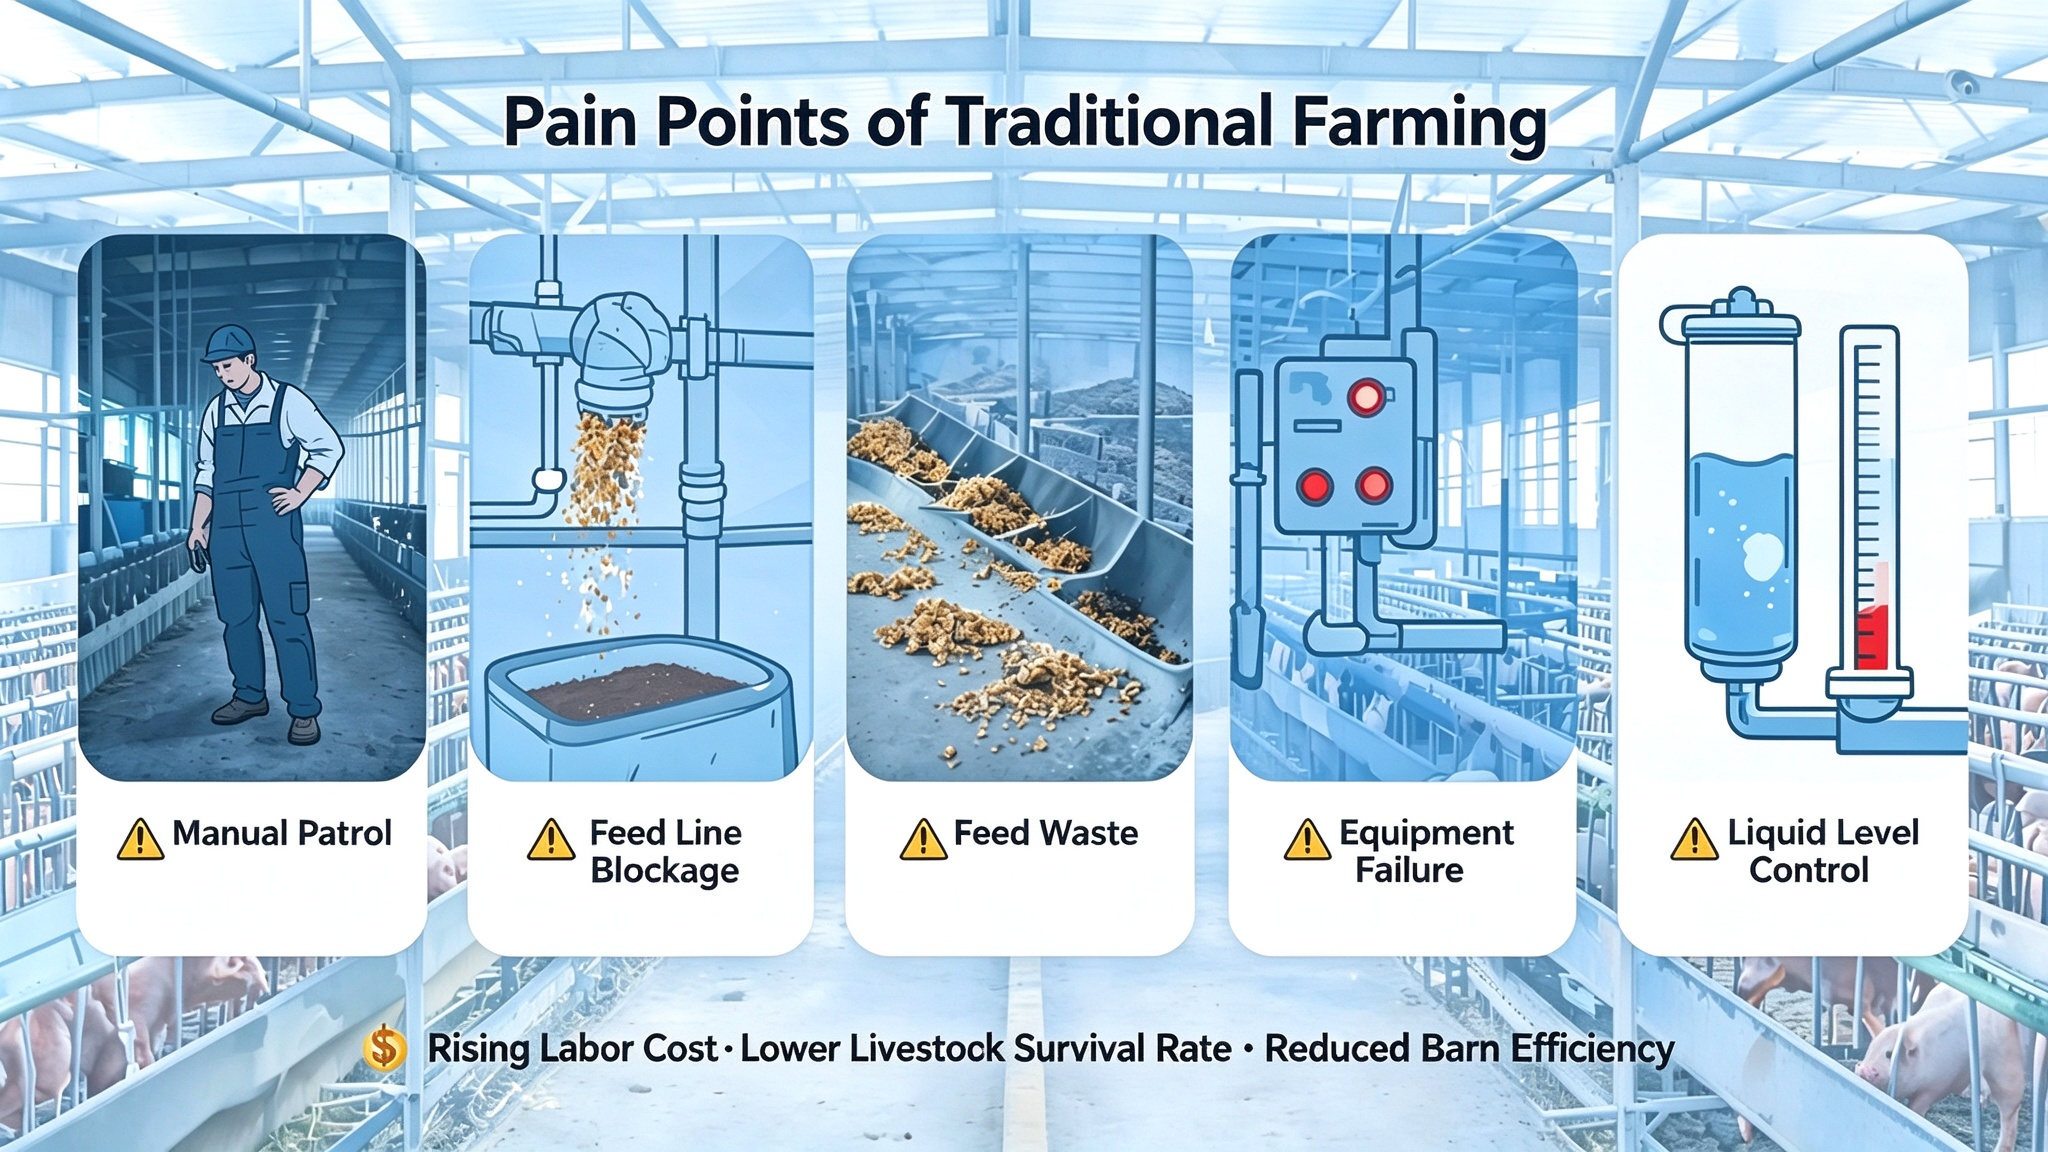
The global livestock industry is undergoing a comprehensive transformation from traditional manual breeding to large-scale, digital, and precise smart farming. With the continuous expansion of breeding scale, the inherent drawbacks of traditional farming modes have become increasingly prominent. Manual inspection efficiency is low, making it impossible to detect feed line blockages, material shortages, and equipment failures in a timely manner. Severe feed waste, inaccurate liquid level control, and frequent livestock housing equipment abnormalities not only raise labor costs and breeding expenses but also directly affect livestock health, survival rate, and overall farm profitability, becoming a major bottleneck restricting the income growth of modern breeding farms.
02.Smart Sensing Technology Empowers Upgraded Livestock Farming
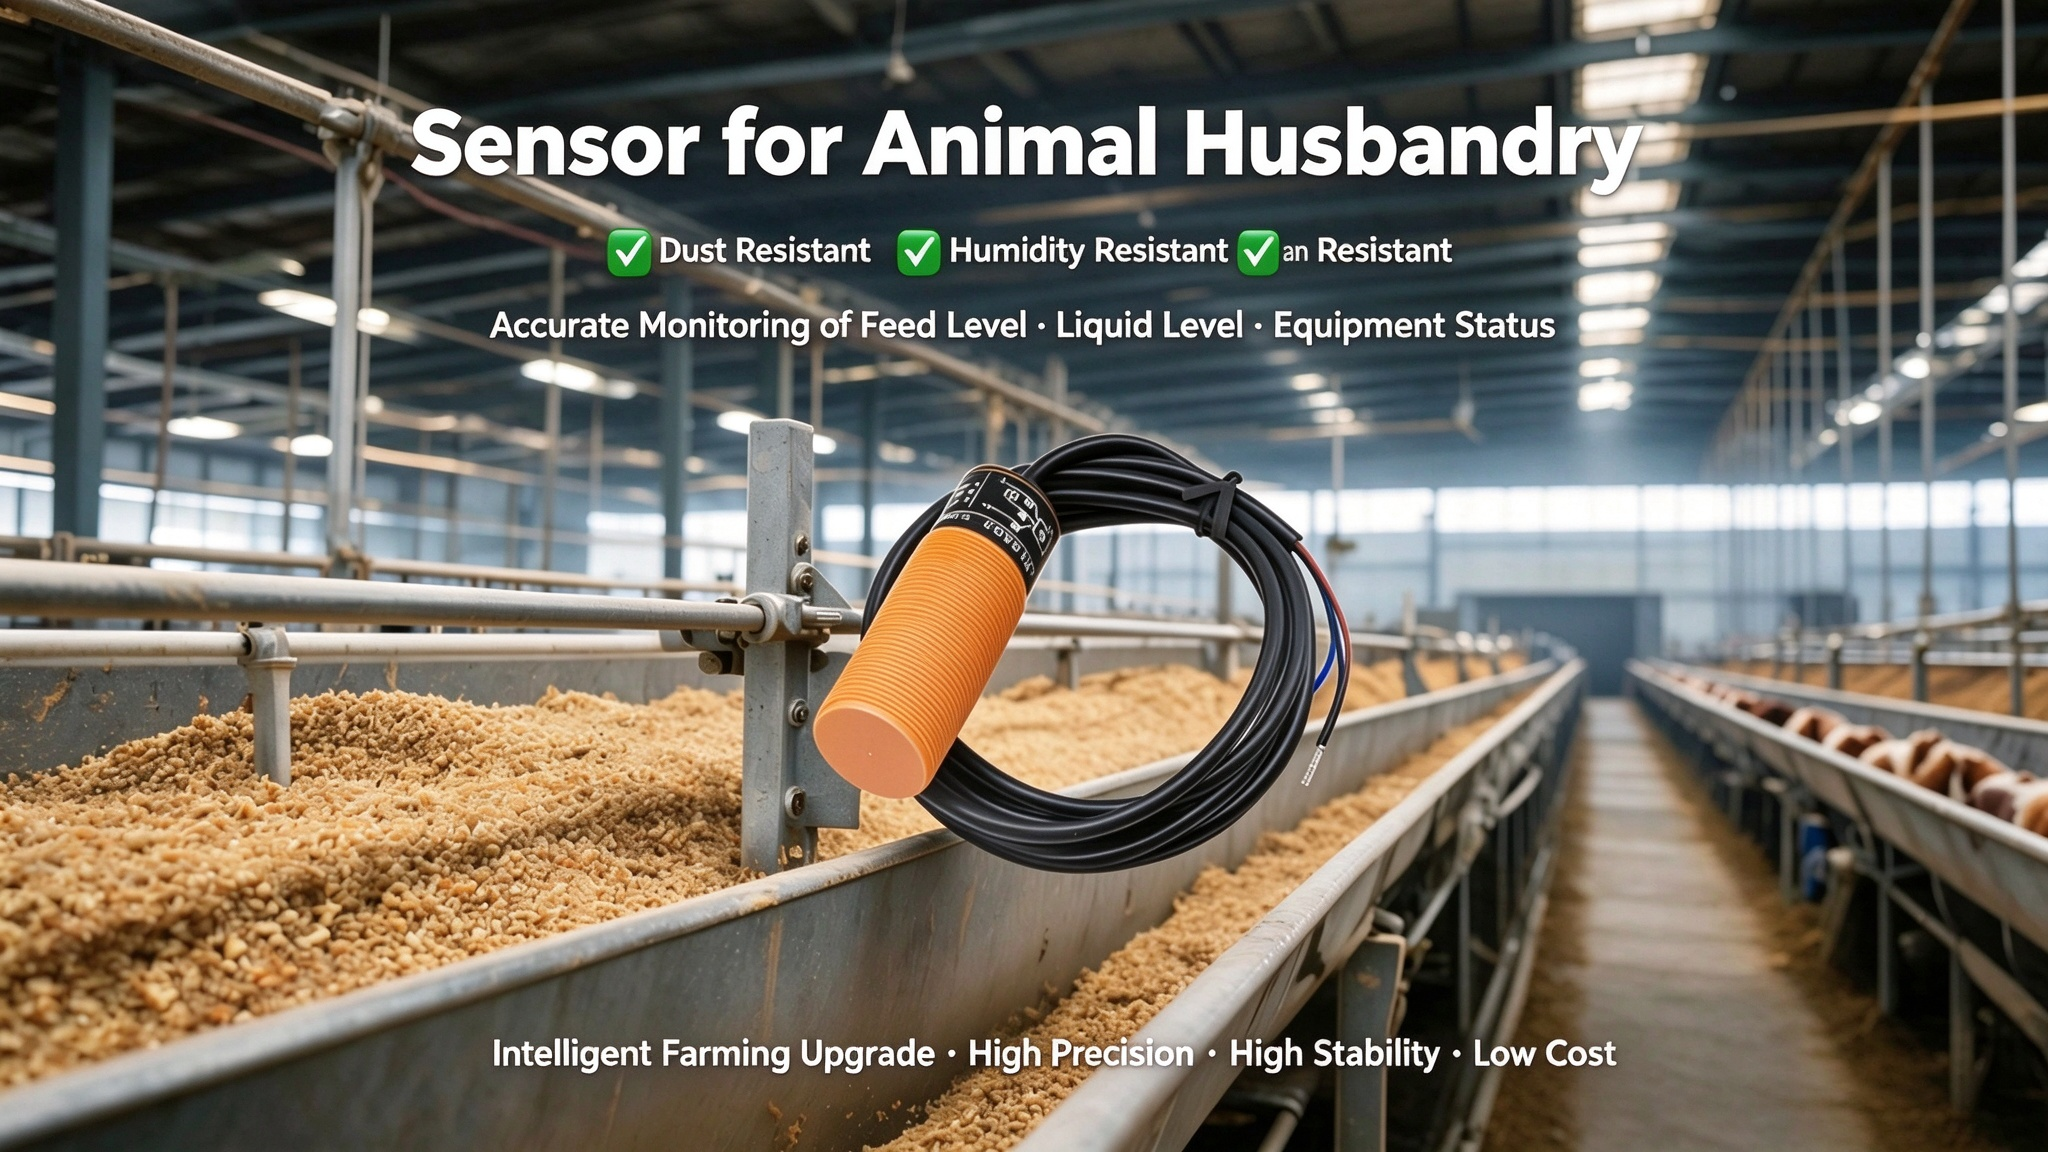
High-precision sensing equipment is the core cornerstone of intelligent and automated livestock farming. With in-depth industry experience and professional technical accumulation in the field of breeding sensing, ELEsenson has developed dedicated industrial sensors for livestock scenarios targeting the harsh operating characteristics of farm environments, including high dust, high humidity, and corrosive gas erosion.
The series of sensors precisely solves common monitoring pain points such as feed material level detection, water and medicine liquid level monitoring, and breeding equipment status perception. Relying on high-stability and high-precision sensing performance, it provides low-cost, high-efficiency digital transformation and intelligent upgrading solutions for large, medium, and small-scale livestock farms.
03.Four Core Advantages, Targeted Solving of Farming Difficulties
Advantage 1: Industrial-Grade Harsh Environment Adaptability, 24/7 Stable Operation
Livestock farms are plagued by long-term dust accumulation, humid and damp air, and frequent equipment vibration. ELEsenson livestock-specific sensors adopt industrial-grade dustproof, moisture-proof, and anti-corrosion structural design, which effectively resists feed adhesion, dust interference, and environmental corrosion. It thoroughly avoids detection failure and false alarm problems caused by harsh working conditions, supports uninterrupted stable operation throughout the year, and greatly reduces equipment failure rate, replacement and later maintenance costs.
Advantage 2: High-Precision Sensing & Real-Time Monitoring, Zero-Deviation Data
Aiming at the defects of traditional manual inspection such as delayed monitoring, missing inspection, and large data errors, the equipment is equipped with high-precision professional sensing chips. It realizes real-time and accurate monitoring of material levels in feed silos and conveying lines, as well as liquid level changes in water tanks and medicinal liquid storage tanks. The monitoring data is synchronized in real time with zero delay and zero deviation, providing reliable data support for precise farming management.
Advantage 3: Intelligent Interconnection & Automatic Control, Unmanned Breeding Management
The sensor supports a variety of universal signal output modes and can be seamlessly connected with farm PLC control systems, central control platforms, and intelligent feeding equipment. When abnormal conditions such as feed shortage, full bin overflow, pipeline blockage, and liquid level abnormality are monitored, the system can automatically trigger alarm reminders and linkage equipment start-stop control.
It builds a closed-loop intelligent management system of “real-time detection – abnormal alarm – automatic control”, completely getting rid of reliance on manual inspection and operation, realizing unattended intelligent operation of breeding links, and minimizing farming losses caused by human error and delayed processing.
Advantage 4: High Cost Performance & Customized Adaptation, Full-Scale Farm Coverage
Breaking the industry dilemma of high price for industrial high-precision equipment, this solution delivers industrial-grade stable performance with civilian affordable pricing. It is not only suitable for large-scale standardized intelligent breeding base deployment but also supports lightweight intelligent upgrading of small and medium-sized farms.
Meanwhile, it supports personalized customized services. According to different breeding types, feed properties (powder/granule), and monitoring media (clean water/medicinal liquid), equipment parameters and structural forms can be flexibly adjusted to meet the differentiated monitoring needs of various livestock and poultry breeding scenarios.
04.Diversified Application Scenarios, Full-Process Breeding Empowerment
4.1 Intelligent Feeding Monitoring
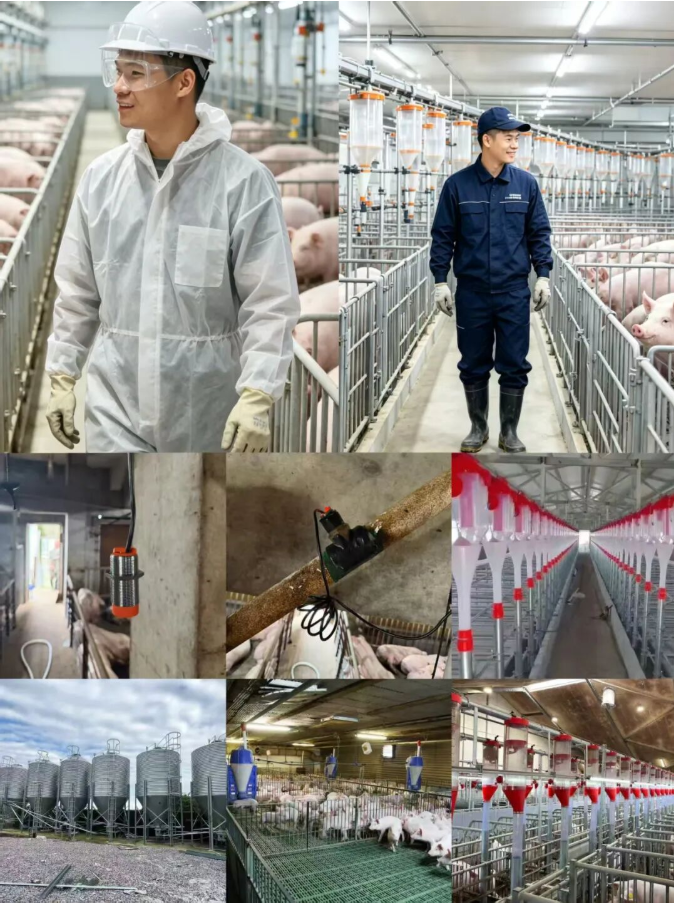
Widely compatible with feed silos, raw material storage bins, feeding hoppers and other equipment of various livestock and poultry farms. It realizes real-time high and low material level monitoring, automatically sends low-material shortage reminders and full-bin anti-overflow protection. It accurately identifies pipeline blockage and empty-bin operation faults, triggers automatic shutdown and alarm linkage, effectively prevents equipment empty-running damage and feed deterioration and waste, and ensures continuous, stable and standardized feeding operation.
4.2 Livestock Pen Intelligent Inspection, Pre-emptive Risk Prevention
Real-time monitoring of abnormal conditions such as feed spillage and trough accumulation in breeding pens. It can early warn of potential equipment operation hidden dangers, avoid feed dampness, water accumulation and mildew caused by long-term accumulation, reduce bacterial breeding and livestock and poultry disease incidence, optimize the micro-environment of breeding houses from the source, and reduce breeding safety risks and loss costs.
4.3 Feed Processing Monitoring, Assisting Factory Precision Production
It provides real-time data feedback for feed processing and production links such as material feeding, conveying and silo storage. Accurate and stable sensing data supports automated production scheduling and precise raw material proportioning, effectively improving feed processing efficiency, realizing refined management of production materials, and reducing production waste.
05.Product Summary
Accurately capture every change of feed and liquid level, and intelligently perceive every operation link of the farm. ELEsenson professional livestock breeding sensors act as an invisible digital partner for modern farms. Empowering traditional breeding with intelligent sensing technology, replacing cumbersome manual work with precise automatic monitoring, ELEsenson helps every farm realize low-cost transformation, efficient production and worry-free breeding management.